

Principles and Application Scenarios of Corn Starch Material Handling
Welcome to Shandong HeadPowder Engineering Co., Ltd., a leading provider of specialized material handling solutions for corn starch processing. This article explores the fundamental principles behind efficient corn starch material handling systems and highlights key application scenarios where these technologies are utilized in industrial settings. By understanding the core mechanisms and practical implementations, businesses can optimize their operations and enhance productivity in corn starch processing workflows.
Core Principles of Corn Starch Material Handling
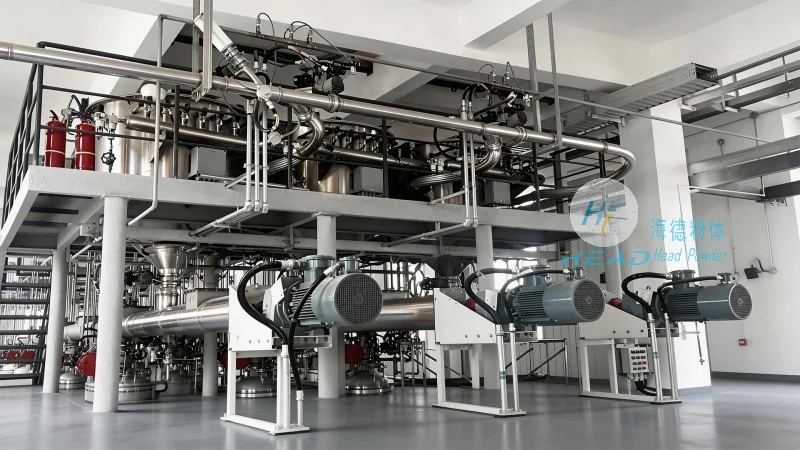
The efficient transportation of corn starch requires a combination of mechanical and gravitational forces tailored to the material's physical properties. Corn starch, being a fine, free-flowing powder, presents unique challenges in terms of dust control, flow uniformity, and equipment wear. To address these challenges, modern material handling systems for corn starch typically employ a range of technologies. One primary principle is the use of enclosed conveyor systems, which minimize dust dispersion and ensure consistent material flow. These systems often incorporate adjustable speed drives and variable incline angles to control the velocity and direction of the starch, preventing clogging and maintaining smooth operation. Additionally, the integration of pneumatic conveying systems may be employed for longer distances or when vertical lifting is required, leveraging air pressure to move the fine powder through pipelines. The selection of appropriate materials for conveyor components, such as food-grade stainless steel and specialized coatings, is critical to prevent contamination and ensure compliance with industry standards. By adhering to these fundamental principles, facilities can achieve reliable and efficient corn starch handling, reducing downtime and operational costs.
Key Application Scenarios in Industrial Settings
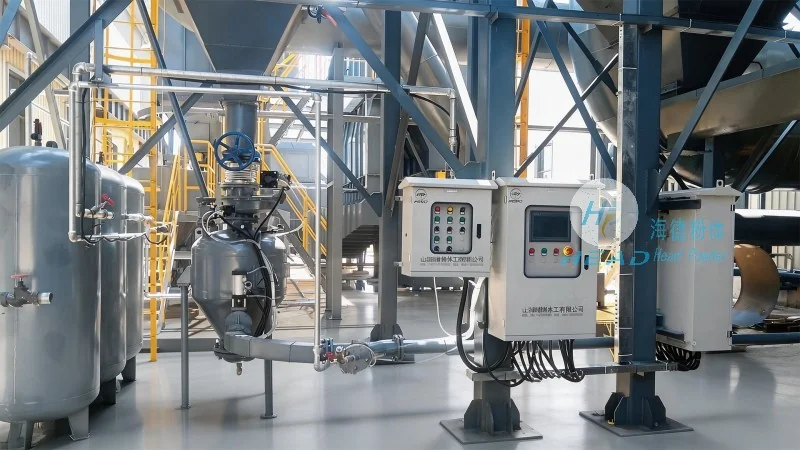
Corn starch material handling systems are widely applied across various industrial sectors, each with distinct requirements that influence the design and implementation of the handling solutions. In the food processing industry, corn starch is a key ingredient in many products, including baked goods, beverages, and dairy alternatives. The handling systems in these facilities must ensure that the starch is transferred hygienically and without contamination, often involving enclosed screw conveyors and sanitary design features. For example, in a bakery, corn starch may be used as a dusting agent or a thickening agent, and the handling system must deliver it to mixing equipment in a controlled manner to maintain product quality. In the pharmaceutical and nutraceutical sectors, corn starch is used as a filler or binder in tablets and capsules. Here, the material handling systems must meet stringent regulatory standards, including GMP (Good Manufacturing Practice) compliance, which requires cleanroom environments and validated processes. The systems may include dust collection and filtration systems to maintain air quality and prevent product contamination. In the chemical and industrial applications, corn starch is used as a raw material in the production of adhesives, coatings, and biodegradable plastics. In these settings, the handling systems may involve bulk storage silos and pneumatic conveying networks to transport the starch from storage to processing units. The ability to handle large volumes efficiently while maintaining material integrity is crucial for cost-effective production. Each application scenario demands a customized approach to material handling, ensuring that the corn starch is processed safely, efficiently, and in compliance with industry regulations.
Technical Considerations for Efficient Material Handling
Optimizing corn starch material handling involves careful consideration of several technical factors that impact system performance and longevity. The first consideration is the choice of conveyor type, which depends on the material's flow characteristics and the distance to be covered. Screw conveyors are commonly used for short to medium distances due to their simplicity and ability to handle vertical lifts. However, for longer distances or when the material needs to be elevated significantly, pneumatic conveying systems are more suitable, as they can transport the fine powder through pipelines without the need for mechanical contact. The design of the conveyor system must also account for the material's dustiness and potential for static accumulation. Proper grounding and bonding of equipment, along with the use of anti-static additives or materials, can mitigate these issues and prevent sparks or electrical hazards. Additionally, the system must be equipped with effective dust collection and filtration systems to maintain air quality and comply with environmental regulations. Regular maintenance is another critical factor, as corn starch can cause wear on conveyor components, particularly the screw flights and bearing housings. Implementing a preventive maintenance schedule, including lubrication, component inspection, and cleaning, helps to extend the life of the equipment and minimize downtime. The integration of sensors and monitoring systems can also enhance operational efficiency by providing real-time data on flow rates, pressure, and system performance, allowing for timely adjustments and troubleshooting. By addressing these technical considerations, businesses can ensure that their corn starch material handling systems operate at peak efficiency, reducing operational costs and improving overall productivity.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
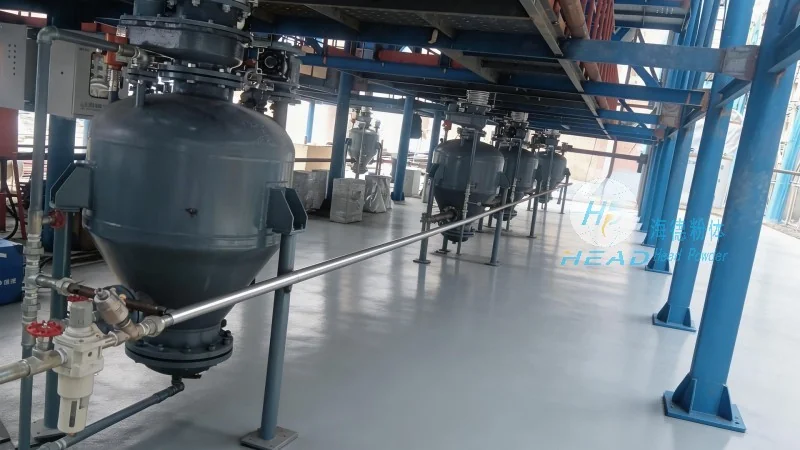
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a specialized engineering firm dedicated to providing innovative material handling solutions for the corn starch and related industries. With headquarters in Shandong, China, the company has built a strong reputation for delivering high-quality, customized systems that meet the unique needs of its clients. The company's expertise lies in the design, manufacturing, and installation of advanced material handling equipment, including enclosed conveyors, pneumatic systems, and bulk storage solutions. By leveraging years of experience in the industry, headpowder has developed a deep understanding of the challenges associated with corn starch processing and has developed tailored solutions to address them. The company's commitment to quality and customer satisfaction is reflected in its adherence to international standards and its focus on providing comprehensive support, from initial consultation to post-installation maintenance. Headpowder's team of engineers and technicians work closely with clients to assess their specific requirements and design systems that optimize material flow, minimize waste, and enhance overall operational efficiency. The company's facilities are equipped with state-of-the-art technology and testing equipment, ensuring that every product meets the highest standards of performance and reliability. With a strong focus on innovation and customer service, Shandong HeadPowder Engineering Co., Ltd. continues to be a trusted partner for businesses seeking to improve their corn starch material handling processes. Through its dedication to excellence and technical expertise, the company plays a vital role in supporting the growth and success of the corn starch industry.