

Working Principle and Features of Dicalcium Phosphate Material Conveying Line
HeadPowder, a professional manufacturer based in Shandong, China, specializes in the design and production of high-efficiency material conveying systems tailored for the dicalcium phosphate industry. This article provides an in-depth exploration of the working principle and key features of a dicalcium phosphate material conveying line, highlighting how these systems enhance operational efficiency and ensure product quality in industrial applications.
Understanding the Working Principle of Dicalcium Phosphate Material Conveying Lines
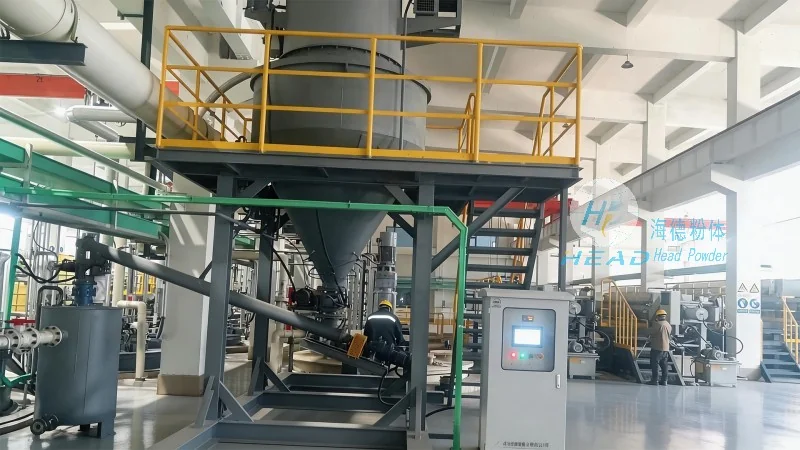
The dicalcium phosphate material conveying line operates through a series of integrated components that work in tandem to transport raw materials, intermediate products, and finished goods. At its core, the system typically includes feeders, conveyors, storage silos, and control systems. The process begins with the material being fed into the system, often from a hopper or storage silo, where it is then transferred to the conveyor belt or screw conveyor for movement. The conveying equipment, such as belt conveyors or bucket elevators, ensures that the material is transported vertically or horizontally with minimal loss and maximum efficiency. Control systems, equipped with sensors and automation technology, monitor the flow rate, pressure, and other critical parameters to maintain consistent operation. This integrated approach allows for seamless material handling from raw material intake to final product discharge, minimizing downtime and maximizing throughput.
Key Features of Dicalcium Phosphate Material Conveying Lines
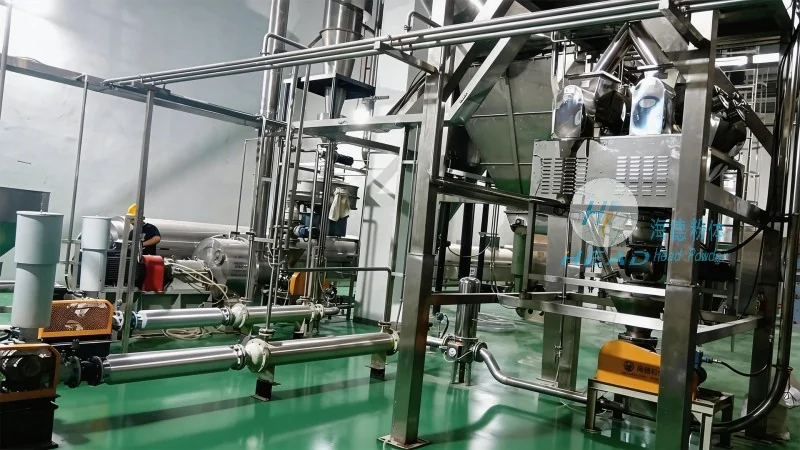
HeadPowder's dicalcium phosphate material conveying lines are engineered with several distinctive features that set them apart in the industry. Firstly, the systems are designed for high durability and resistance to corrosion, which is essential for handling materials that may be acidic or contain moisture. The use of high-quality materials, such as stainless steel or specialized coatings, ensures long-term reliability and reduces maintenance costs. Secondly, the conveying lines are equipped with advanced control technologies, including PLC (Programmable Logic Controller) systems and real-time monitoring software. These features enable precise control over the material flow, allowing operators to adjust parameters dynamically based on production demands. Thirdly, the systems incorporate safety features, such as emergency stop buttons and overload protection, to ensure safe operation and prevent accidents. Additionally, the design of the conveying lines allows for easy maintenance and cleaning, which is crucial for maintaining product purity and meeting regulatory standards. The integration of these features results in a robust, efficient, and user-friendly material handling solution that meets the specific needs of the dicalcium phosphate industry.
Enhancing Operational Efficiency and Product Quality
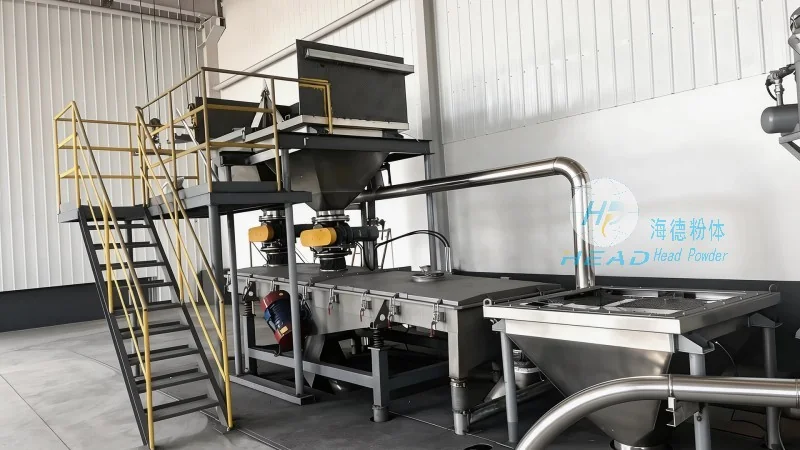
The implementation of a well-designed dicalcium phosphate material conveying line significantly improves operational efficiency in industrial settings. By automating the material handling process, the system reduces the need for manual labor, minimizes human error, and increases production throughput. The consistent flow of material ensures that production lines operate smoothly, with fewer interruptions and lower downtime. Furthermore, the advanced control systems allow for precise monitoring of material quality, ensuring that the final product meets stringent quality standards. This is particularly important in the dicalcium phosphate industry, where product purity and consistency are critical for downstream applications. The use of automated conveying systems also helps in maintaining a clean and hygienic environment, which is essential for compliance with food and pharmaceutical regulations. Overall, the features and working principle of the dicalcium phosphate material conveying line contribute to a more efficient, reliable, and cost-effective production process.
Conclusion
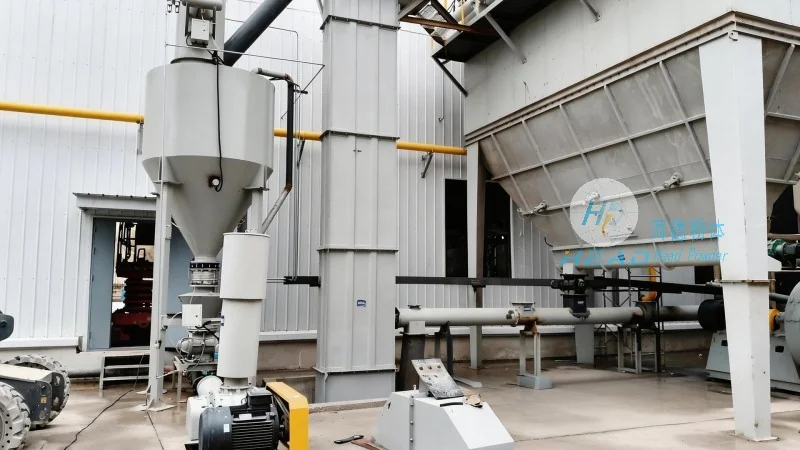
HeadPowder's dicalcium phosphate material conveying lines represent a sophisticated solution for material handling in the dicalcium phosphate industry. By combining advanced technology, robust design, and user-friendly features, these systems enhance operational efficiency, ensure product quality, and reduce maintenance costs. The working principle, which involves integrated components and automated control, enables seamless material transport from raw material intake to final product discharge. The key features, including durability, advanced control, and safety measures, make these conveying lines a reliable choice for industrial applications. As a leading manufacturer based in Shandong, China, HeadPowder continues to innovate and provide tailored solutions that meet the evolving needs of the dicalcium phosphate sector.