

Working Principle and Features of Cement Powder Conveying System Equipment
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design, production, and supply of advanced cement powder conveying systems. These systems are engineered to efficiently handle the transportation of cement and other fine powders, playing a crucial role in modern construction and industrial applications. The following sections will delve into the working principle and key features of such equipment, providing a comprehensive understanding of their functionality and benefits.
Working Principle of Cement Powder Conveying System Equipment
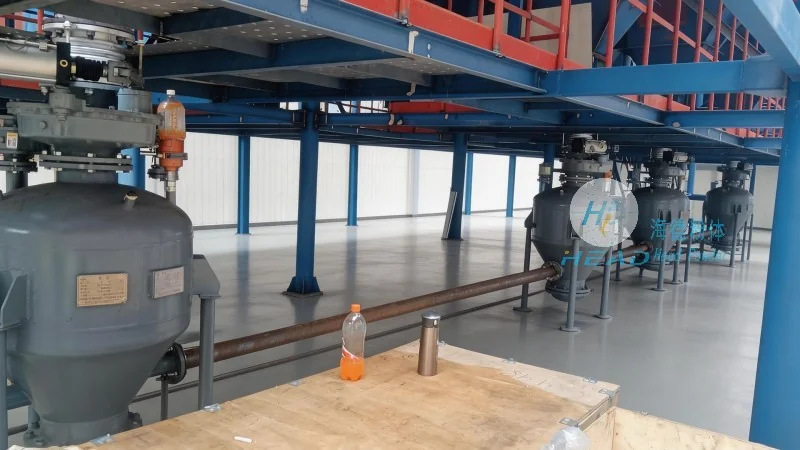
The cement powder conveying system primarily operates on the principle of pneumatic or mechanical transport, depending on the specific design and application requirements. A common method is the use of a positive pressure system, where compressed air or gas is used to create a flow of air carrying the powder particles. The system typically consists of a hopper for material storage, a feeder to control the flow rate, a conveying line (often equipped with ducts or pipes), and a receiver for the discharged material. The air flow is generated by a blower or fan, which draws air through the conveying line and transports the cement powder from the source to the destination. This process ensures that the material is moved without the need for mechanical contact, reducing wear and tear on the equipment. Additionally, some systems may incorporate vacuum technology for negative pressure transport, which is suitable for applications requiring the collection of dust or fine powders from a source location.
Key Features of Cement Powder Conveying System Equipment
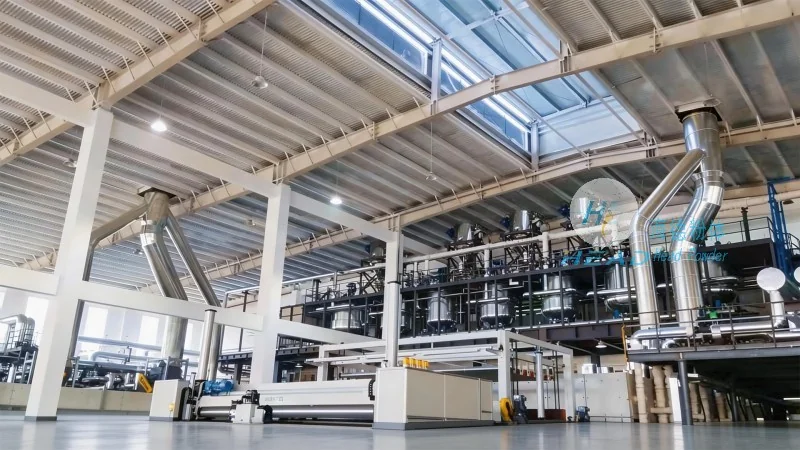
HeadPowder's cement powder conveying systems are characterized by several notable features that enhance their performance and reliability. Firstly, they are designed for high efficiency, capable of transporting large volumes of cement powder with minimal energy consumption. The systems are equipped with advanced control mechanisms that allow for precise regulation of the material flow rate, ensuring consistent and stable operation. This precision is crucial in applications where the quality of the transported material must be maintained, such as in the production of concrete or other cement-based products. Secondly, the equipment is built for durability and low maintenance. The use of high-quality materials and robust construction ensures that the system can withstand the abrasive nature of cement powder, reducing the frequency of repairs and extending its service life. Thirdly, the systems are designed with environmental considerations in mind. Many models incorporate dust collection and filtration systems to minimize air pollution and comply with environmental regulations. This not only protects the environment but also enhances workplace safety by reducing the exposure of operators to fine powders. Fourthly, the flexibility of the conveying systems allows for easy integration into existing production lines. The modular design enables customization to meet specific customer requirements, including different conveying distances, material capacities, and operational pressures. This adaptability makes the systems suitable for a wide range of industrial settings, from small-scale construction sites to large-scale cement production facilities.
Applications and Benefits in Industrial Context
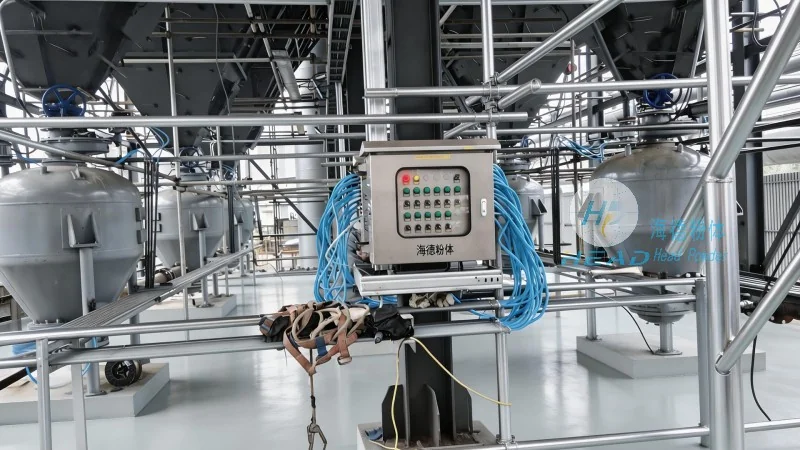
The cement powder conveying systems manufactured by Shandong HeadPowder Engineering Co., Ltd. find extensive applications across various industries. In the construction sector, these systems are essential for the efficient delivery of cement to mixing plants, ensuring that the production process remains uninterrupted and productive. The ability to transport large quantities of cement quickly and reliably reduces downtime and improves overall project efficiency. In the chemical and pharmaceutical industries, similar systems are used for the handling of other fine powders, such as chemicals and pharmaceuticals, where precision and cleanliness are paramount. The systems' ability to maintain the integrity of the material during transport is particularly valuable in these sectors. Additionally, the equipment is beneficial in the mining and mineral processing industries, where it is used to transport ore powders and other fine materials from processing plants to storage or further processing facilities. The consistent and reliable operation of the conveying systems helps to optimize the entire production process, leading to increased productivity and reduced operational costs. Overall, the cement powder conveying systems offer significant advantages in terms of efficiency, reliability, and environmental compliance, making them a vital component in modern industrial operations.
Conclusion and Company Overview
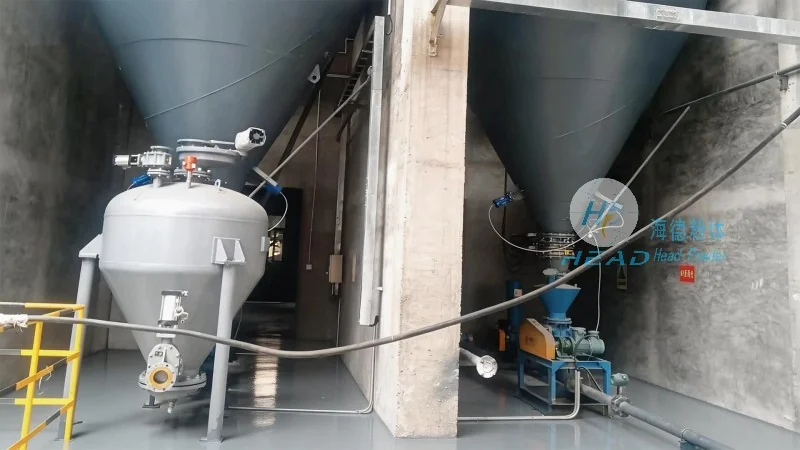
Shandong HeadPowder Engineering Co., Ltd. stands as a trusted provider of high-quality cement powder conveying system equipment, leveraging advanced technology and robust engineering to meet the diverse needs of its clients. The company's commitment to innovation and customer satisfaction is reflected in the design and functionality of its products, which are tailored to enhance operational efficiency and ensure long-term reliability. With a strong presence in Shandong, China, HeadPowder continues to serve the global market with cutting-edge solutions for powder handling, supporting the growth and success of industries that rely on the efficient transportation of fine materials. The systems' working principle, combined with their key features, positions them as a preferred choice for businesses seeking to optimize their material handling processes and improve overall productivity.