

Working Principle and Features of Automatic Weighing Powder Conveying Systems
Automatic weighing powder conveying systems represent a critical technology in modern industrial processes, particularly in sectors such as pharmaceuticals, chemicals, and food processing. These systems are designed to handle the precise measurement and transportation of bulk powders, ensuring consistent quality and efficiency in production lines. The integration of advanced weighing technology with automated conveying mechanisms has revolutionized how industries manage raw materials, reducing human error and enhancing operational reliability.
Working Principle of Automatic Powder Weighing and Conveying Systems
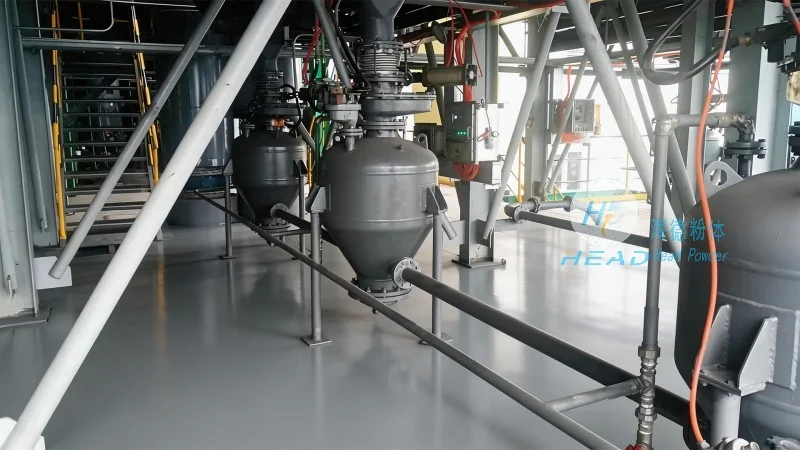
The core of an automatic weighing powder conveying system lies in its ability to accurately measure and control the flow of powders. Typically, the system comprises several key components: a weighing hopper or container, a conveyor mechanism (such as a screw conveyor or pneumatic conveyor), and a control unit equipped with sensors and a digital display. The weighing hopper is where the powder is placed, and as it is added or removed, the load cells within the hopper detect the weight changes. These signals are transmitted to the control unit, which processes the data and adjusts the conveyor speed or flow rate accordingly. The control unit may use algorithms to maintain a target weight, ensuring that the correct amount of powder is conveyed to the next stage of the process. For example, in a pharmaceutical manufacturing line, the system might be used to weigh and dispense active pharmaceutical ingredients (APIs) into packaging containers with high precision, meeting regulatory standards for dosage accuracy.
Key Features of Automatic Powder Weighing Conveying Systems
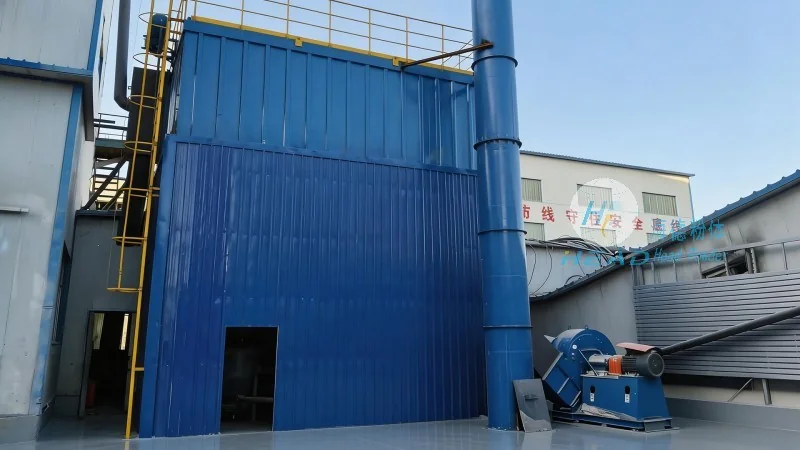
Several distinct features make automatic weighing powder conveying systems highly effective for industrial applications. First, high precision and accuracy are paramount. The systems utilize load cells with high sensitivity and resolution, enabling measurements with minimal error, often within ±0.1% of the target weight. This level of precision is crucial in industries where product consistency directly impacts quality and safety. Second, automation and integration are key advantages. Once set up, the system operates with minimal human intervention, allowing for continuous production without the need for constant monitoring. The control unit can be integrated with other equipment in the production line, such as mixers or packaging machines, creating a seamless workflow. Third, versatility in handling different powder types is another significant feature. These systems can accommodate a wide range of materials, from fine powders like talc or starch to bulkier materials like flour or cement, adapting to various particle sizes and flow characteristics. Additionally, stability and reliability are ensured through robust construction and advanced control algorithms, minimizing downtime and maintenance requirements. The systems are often designed with redundant components and self-diagnostic features to detect and address issues promptly, ensuring consistent performance over extended periods.
Application Scenarios and Benefits
Automatic weighing powder conveying systems find applications in diverse industries, each benefiting from the system's capabilities. In the pharmaceutical industry, they are used for the precise weighing of active ingredients and excipients, ensuring that each batch of medication meets strict dosage requirements. In the chemical industry, these systems are employed to handle raw materials for manufacturing, such as chemicals used in coatings or plastics, where uniformity is critical for product performance. The food and beverage industry also utilizes these systems for processing ingredients like sugar, flour, or spices, maintaining consistent quality in final products. The primary benefits of implementing such systems include improved product quality, reduced waste due to accurate measurement, increased production efficiency, and enhanced safety by minimizing manual handling of powders. Furthermore, the automation aspect reduces labor costs and the risk of human error, contributing to overall operational cost savings.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
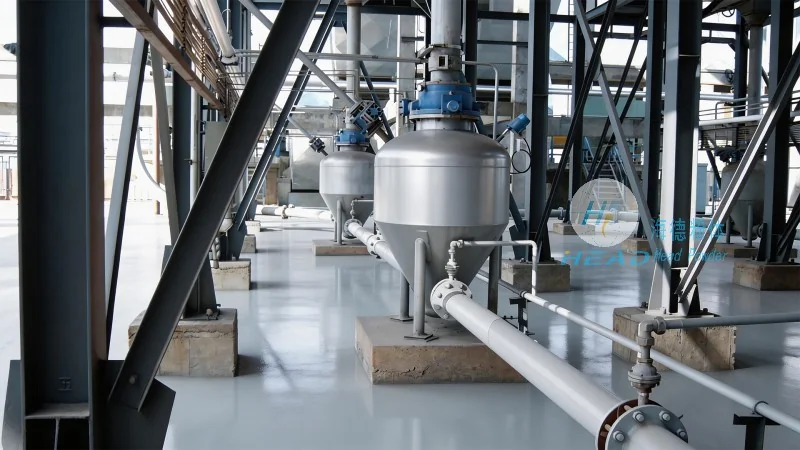
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name HeadPowder, specializes in the design, manufacturing, and supply of advanced powder handling equipment. With a focus on innovation and precision engineering, the company has established itself as a leading provider of automatic weighing powder conveying systems. HeadPowder's expertise lies in understanding the unique challenges of different industries and tailoring solutions to meet specific requirements. The company's products are built with high-quality materials and advanced technology, ensuring durability and reliability in demanding industrial environments. HeadPowder's commitment to customer satisfaction is reflected in its comprehensive after-sales support, including technical assistance, maintenance services, and customization options. Based in Shandong, China, HeadPowder leverages its local presence to provide efficient service and support to clients across the region and beyond.