

Working Principle and Characteristics of Positive Pressure Blown Powder Conveying
Positive pressure blown powder conveying systems are a critical component in modern industrial material handling, offering efficient and reliable methods for transporting bulk powders over long distances or through complex layouts. This technology is widely used across various industries, including pharmaceuticals, food processing, and chemical manufacturing, where precise and controlled powder movement is essential for operational efficiency and product quality. The following sections will delve into the working principle and key characteristics of this system, providing a comprehensive understanding of its functionality and advantages.
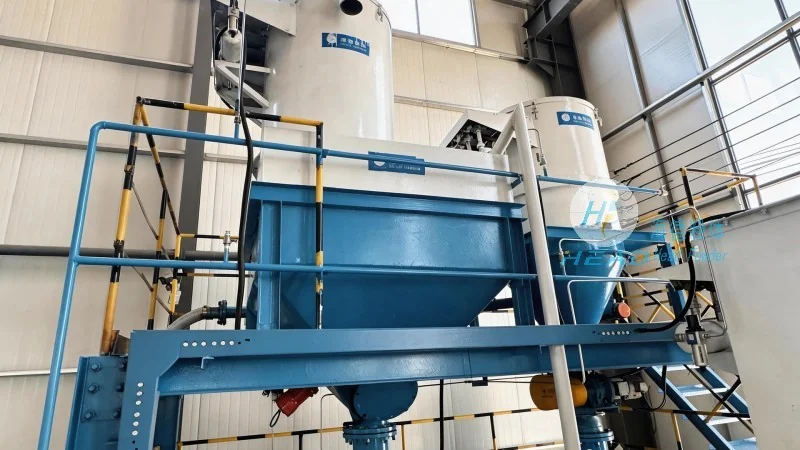
Working Principle of Positive Pressure Blown Powder Conveying
The core mechanism of positive pressure blown powder conveying involves creating a pressurized air stream within a sealed pipeline system. This pressurized air, typically generated by a high-pressure blower or fan, is used to transport the powder particles through the pipeline. The system operates by introducing the powder into the pipeline at a designated inlet point, where it is then entrained by the high-velocity air flow. As the air flows through the pipeline, it carries the powder particles along with it, ensuring that the material is transported from the source to the destination without the need for mechanical components like screws or belts that might cause wear or contamination. The pressurized air maintains a consistent flow rate, which is crucial for maintaining the integrity of the powder and preventing clogging or blockages in the system. The entire process is controlled by a series of valves, regulators, and sensors that monitor pressure, flow rate, and particle concentration, allowing for real-time adjustments to optimize performance and ensure safe operation.
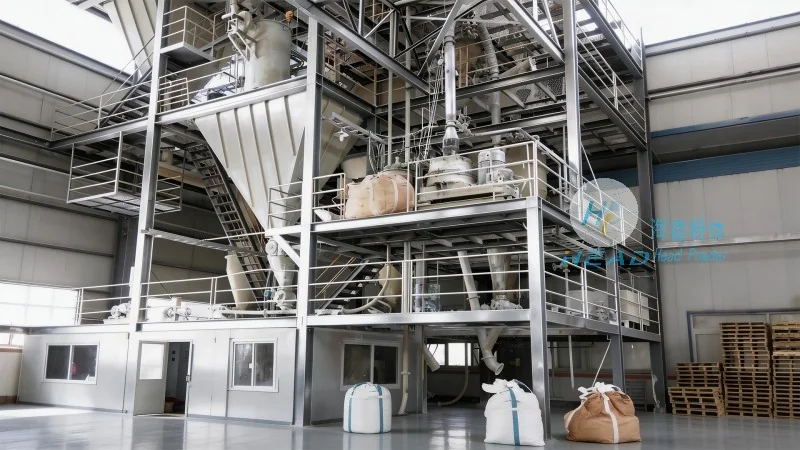
Key Characteristics of Positive Pressure Blown Powder Conveying Systems
Positive pressure blown powder conveying systems exhibit several distinct characteristics that make them suitable for a wide range of applications. One of the primary advantages is their ability to handle a variety of powder types, including fine powders, granules, and even cohesive materials, without requiring significant modifications to the system. The pressurized air flow provides sufficient momentum to overcome the gravitational forces acting on the powder particles, ensuring consistent and reliable transport. Another notable characteristic is the system's ability to operate over long distances, with minimal pressure drop, which is essential for industrial facilities that require material transport across multiple buildings or across large production areas. The sealed pipeline design also helps to prevent dust emissions and contamination, making it suitable for applications where product purity is paramount, such as in the pharmaceutical and food industries. Additionally, these systems are relatively low in maintenance compared to other conveying methods, as they lack moving parts that are prone to wear and tear. The use of high-quality materials, such as stainless steel or special alloys, further enhances the durability and longevity of the system, reducing the need for frequent repairs or replacements.
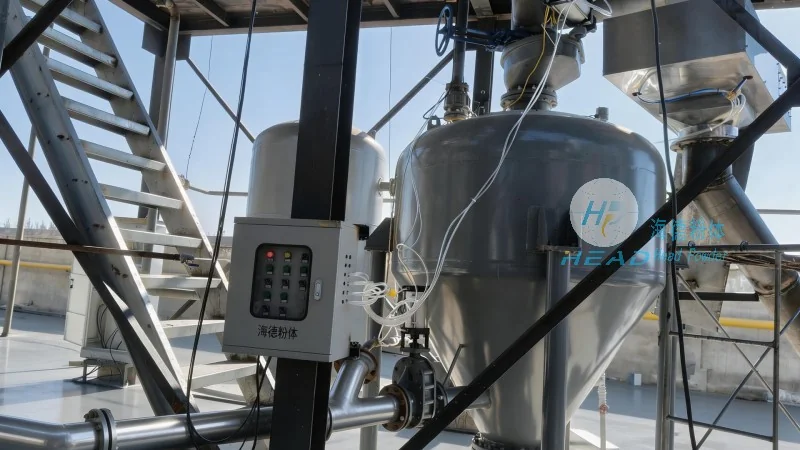
Applications and Industries Utilizing Positive Pressure Blown Powder Conveying
Due to its versatility and efficiency, positive pressure blown powder conveying is employed in numerous industries where bulk powder handling is a critical process. In the pharmaceutical industry, for example, this technology is used to transport active pharmaceutical ingredients (APIs) and excipients with high precision, ensuring that the final product meets stringent quality standards. The sealed system prevents cross-contamination and maintains the integrity of the powder, which is crucial for maintaining product efficacy and safety. In the food processing sector, the system is utilized to transport ingredients like flour, sugar, and spices, where hygiene and product purity are of utmost importance. The ability to handle fine powders without generating dust or causing product degradation makes it an ideal choice for food applications. Similarly, in the chemical manufacturing industry, positive pressure blown powder conveying is used to transport raw materials and intermediates, enabling efficient production processes and reducing downtime. The system's ability to handle abrasive and corrosive materials also makes it suitable for chemical applications where other conveying methods may not be feasible.
Advantages and Limitations of Positive Pressure Blown Powder Conveying
While positive pressure blown powder conveying offers numerous advantages, it also has certain limitations that must be considered when selecting a conveying system. One of the main advantages is its high efficiency in transporting powders over long distances with minimal energy consumption compared to other methods. The pressurized air flow ensures consistent particle movement, reducing the risk of clogging and improving overall system reliability. Another advantage is the system's ability to handle a wide range of powder characteristics, including varying particle sizes, densities, and flow properties. This flexibility makes it suitable for diverse industrial applications. However, the system does have limitations, such as the need for a sealed pipeline to prevent dust emissions and maintain product purity. The initial investment cost for the system can be higher compared to simpler conveying methods, as it requires specialized equipment like high-pressure blowers and sealed pipelines. Additionally, the system may not be suitable for transporting very large or heavy particles, as the air flow may not provide sufficient force to move them effectively. In such cases, alternative conveying methods like mechanical screw conveyors or pneumatic vacuum systems may be more appropriate.
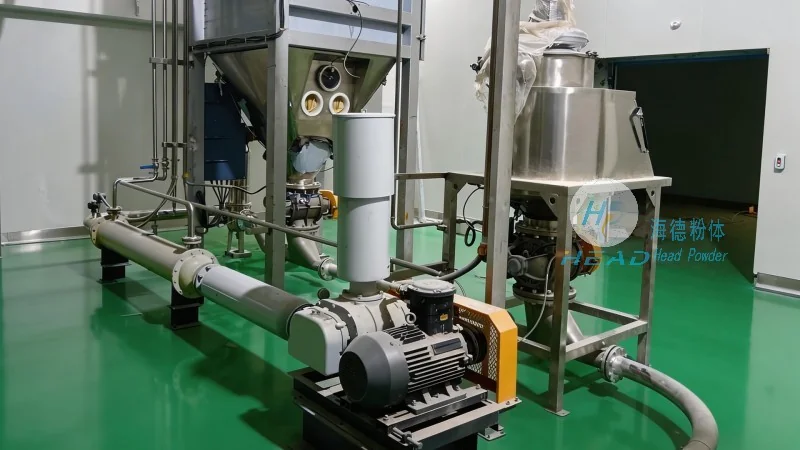
Conclusion and Company Information
Positive pressure blown powder conveying systems represent a sophisticated and efficient solution for bulk powder handling in various industrial sectors. By understanding the working principle and key characteristics of this technology, industries can make informed decisions about implementing it in their operations. The system's ability to ensure product purity, maintain consistent flow rates, and handle diverse powder types makes it a valuable asset for modern manufacturing processes. As a leading provider of powder handling solutions, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing high-quality positive pressure blown powder conveying systems tailored to the specific needs of different industries. With a focus on innovation and customer satisfaction, the company offers reliable and durable equipment that enhances operational efficiency and product quality. Based in Shandong, China, Shandong HeadPowder Engineering Co., Ltd. leverages its expertise and experience to deliver cutting-edge solutions that meet the evolving demands of the industrial market.