

What is a Powdered Food Additive Conveying Equipment? And What Are Its Design Principles?
For food processing industries, the efficient and safe handling of powdered food additives is a critical aspect of production. This involves specialized equipment designed to transport these materials from one point to another within a facility. The equipment in question is often referred to as a powdered food additive conveying system, and understanding its design principles is essential for optimizing operational efficiency and maintaining product integrity.
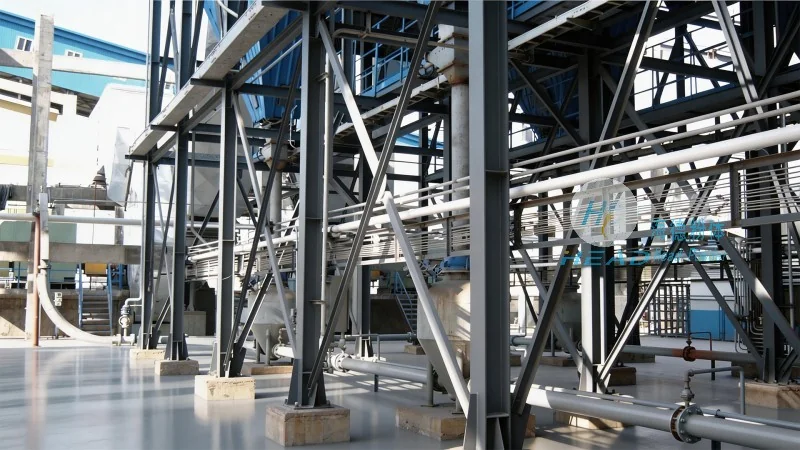
Introduction to Powdered Food Additive Conveying Equipment
Powdered food additives, such as vitamins, preservatives, and flavor enhancers, are commonly used in the food manufacturing process. These materials are typically fine, dry particles that require careful handling to prevent segregation, caking, or contamination. Conveying equipment specifically engineered for these applications ensures that the additives are transported reliably and hygienically, meeting stringent industry standards. The primary goal of such equipment is to provide a consistent flow of material while minimizing the risk of product degradation or cross-contamination.
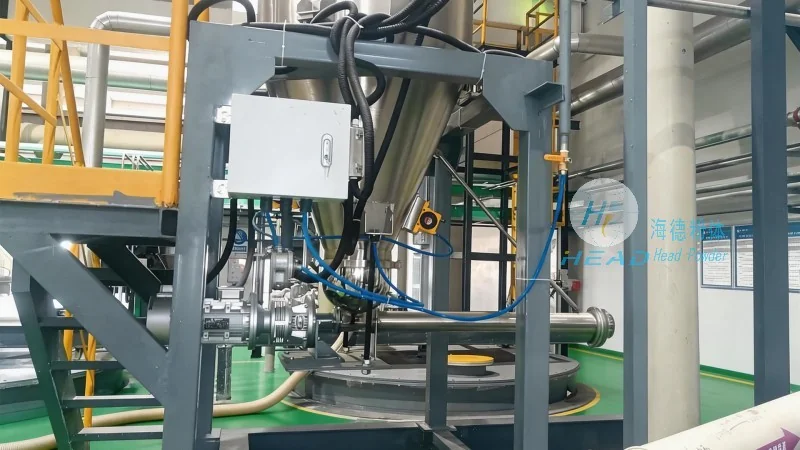
Key Components of Powdered Food Additive Conveying Systems
HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, specializes in the design and production of advanced conveying equipment for the food industry. Their systems are built with components that are specifically tailored to the unique characteristics of powdered food additives. Key components include:
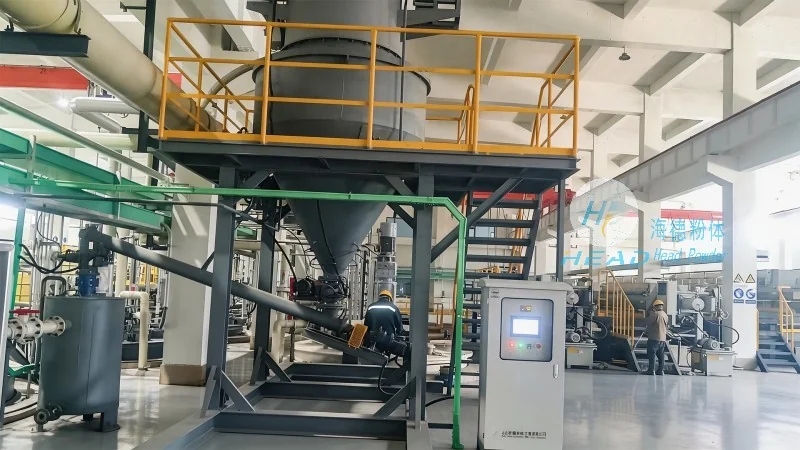
- Feeder Systems: These are designed to provide a controlled and uniform flow of material from storage silos or hoppers into the conveying line. Proper feeding is crucial to prevent overloading or underloading, which can lead to equipment wear or inconsistent product delivery.
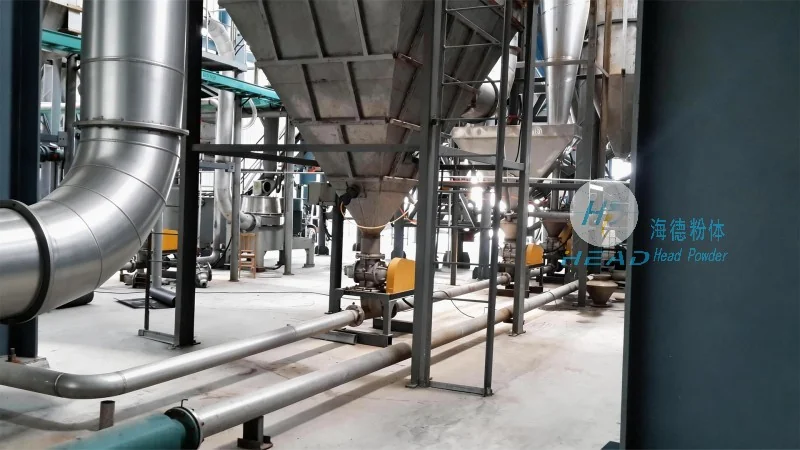
- Pneumatic Conveying Lines: Many systems utilize air or gas to transport the powder, using either positive or negative pressure to move the material. This method is ideal for handling fine powders that are prone to dusting or segregation.
- Rotary Valves and Check Valves: These components regulate the flow of material at various points in the system, ensuring that the powder is directed to the correct destination without backflow or spillage.
- Filter and Dust Collection Systems: To maintain a clean and safe environment, these systems capture any airborne particles, preventing contamination and ensuring compliance with hygiene regulations.
Design Principles for Efficient Powdered Food Additive Conveying
The design of a powdered food additive conveying system is guided by several key principles to ensure optimal performance and safety. These principles include:
- Hygienic Design: All components are constructed from materials that are easy to clean and sanitize, such as stainless steel. This is essential for maintaining food safety standards and preventing bacterial growth.
- Prevention of Segregation and Caking: The equipment is designed with smooth surfaces and gentle material handling to avoid the separation of different particle sizes or the formation of clumps. This ensures that the additive maintains its uniformity throughout the process.
- Controlled Airflow and Pressure: Precise control of air pressure and flow rate is critical to prevent material degradation or excessive wear on components. This also helps in maintaining consistent product quality.
- Energy Efficiency: Modern designs incorporate energy-saving features, such as variable speed drives and optimized air usage, to reduce operational costs while maintaining performance.
Application and Benefits in Food Processing
The powdered food additive conveying equipment from HeadPowder Engineering Co., Ltd. is widely used in various food processing applications. These systems are essential for transferring additives from storage to production lines, ensuring that the final product meets quality and regulatory requirements. The benefits of using such equipment include improved process efficiency, reduced labor costs, enhanced product consistency, and compliance with industry hygiene standards.
Conclusion
In summary, the powdered food additive conveying equipment is a vital component in modern food processing facilities. Its design, based on principles of hygienic operation, material handling, and energy efficiency, ensures the reliable and safe transport of powdered additives. Companies like HeadPowder Engineering Co., Ltd. play a crucial role in providing these specialized systems, contributing to the overall productivity and quality of the food industry.