

What is a Borax Powder Conveying System? What are its Design Principles?
For industrial applications involving borax powder, efficient and reliable material handling is crucial. A borax powder conveying system is a specialized setup designed to transport borax powder from storage to processing or packaging areas. The design principles behind such systems are tailored to address the unique challenges of handling fine, abrasive, and potentially hygroscopic powders like borax, ensuring minimal product loss, contamination, and operational safety.
HeadPowder Engineering: Your Partner in Powder Handling Solutions
HeadPowder Engineering, a leading provider of powder handling technologies, specializes in developing customized borax powder conveying systems. With headquarters in Shandong, China, the company leverages decades of expertise to deliver solutions that meet the specific demands of borax processing industries. Their systems are engineered to optimize flow, maintain product integrity, and enhance overall operational efficiency, making them a trusted choice for manufacturers relying on consistent and safe borax handling.
Key Components of a Borax Powder Conveying System
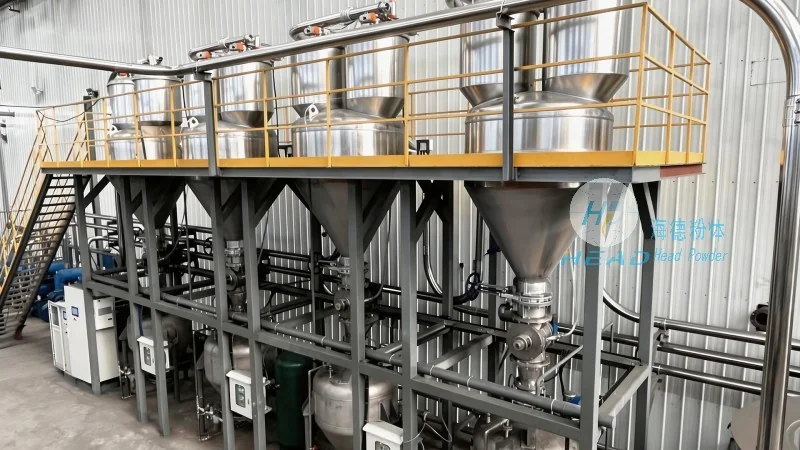
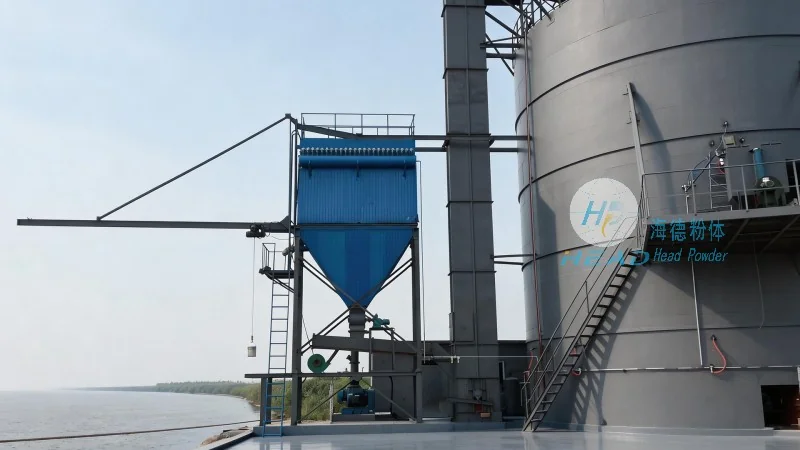
A typical borax powder conveying system comprises several critical components that work in harmony to ensure smooth material transport. These include feeders, conveyors, dust collection systems, and control units. The feeders, often rotary or vibratory types, are designed to regulate the flow of borax powder from storage bins or hoppers, preventing overfilling and ensuring a steady supply to the conveyor. Conveyors, such as pneumatic or mechanical systems, then transport the powder through pipelines or enclosed ducts, minimizing exposure to the environment and reducing the risk of dust dispersion. Dust collection systems are integrated to capture any airborne particles, maintaining air quality and compliance with environmental regulations. Control units, equipped with sensors and automation, monitor system performance, adjust flow rates, and provide real-time feedback to optimize operation.
Design Principles for Efficient Borax Powder Handling
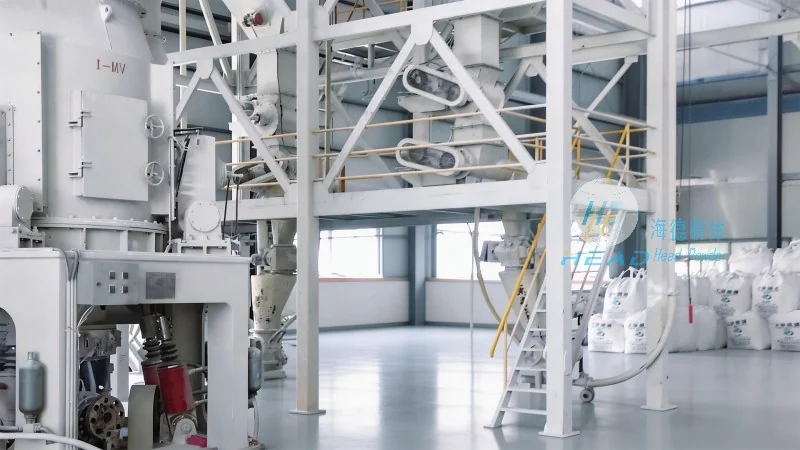
The design of a borax powder conveying system is guided by several key principles aimed at maximizing efficiency and safety. First, the system must prioritize material integrity. Borax is a fine powder that can degrade or clump if not handled properly, affecting its quality and usability. Therefore, components like feeders and conveyors are constructed from materials resistant to corrosion and abrasion, such as stainless steel or specialized polymers, to prevent product contamination and equipment wear. Second, the system must ensure complete containment. Borax is often handled in environments where dust control is critical, and the design incorporates sealed enclosures and positive pressure systems to prevent dust leakage and protect both the product and personnel. Third, the system must offer flexibility and scalability. HeadPowder Engineering designs systems that can be adjusted to accommodate varying production volumes and process requirements, allowing for seamless integration into existing manufacturing lines or expansion as production needs grow. Finally, the system must prioritize energy efficiency and operational cost-effectiveness. By optimizing flow rates and reducing material loss, the design minimizes energy consumption and operational expenses, making it a cost-effective solution for long-term use.
Advantages of a Well-Designed Borax Powder Conveying System
Implementing a well-designed borax powder conveying system offers numerous advantages for industrial operations. Firstly, it enhances product quality by maintaining the purity and consistency of borax powder. By preventing contamination and ensuring uniform flow, the system ensures that the final product meets stringent quality standards, which is particularly important in applications like detergents, glass manufacturing, and pharmaceuticals. Secondly, it improves operational safety by reducing dust exposure and minimizing the risk of accidents. The sealed design and dust collection systems create a safer working environment, protecting employees from respiratory hazards and other health risks associated with fine powders. Thirdly, it boosts productivity by streamlining material handling processes. The automated control units and efficient conveyors reduce manual labor, allowing for faster and more consistent production, which can lead to increased output and reduced downtime. Finally, it provides cost savings through reduced material loss and energy efficiency. By minimizing product waste and optimizing energy use, the system lowers operational costs over time, making it a financially sound investment for businesses in the borax processing industry.
Conclusion: Choosing the Right Borax Powder Conveying System
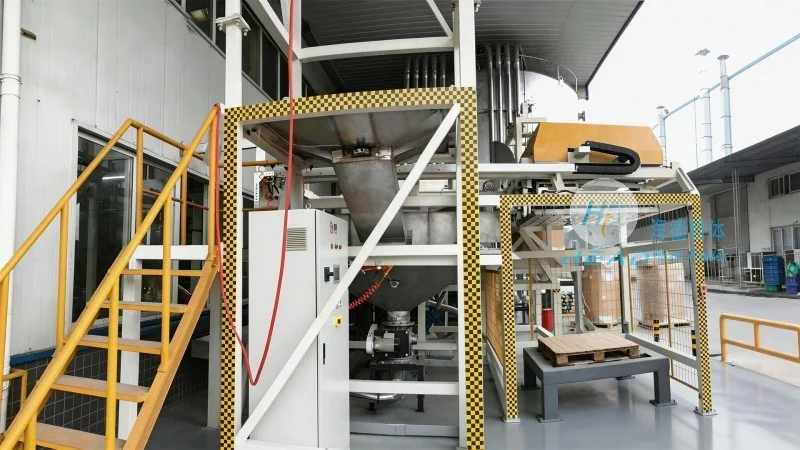
When selecting a borax powder conveying system, it is essential to consider the specific requirements of your operation, including production volume, product characteristics, and environmental regulations. HeadPowder Engineering, with its expertise in powder handling and commitment to quality, offers tailored solutions that address these needs effectively. By focusing on design principles that prioritize material integrity, containment, flexibility, and efficiency, their systems provide reliable and cost-effective solutions for borax powder transport. Whether you are a new manufacturer entering the borax market or an existing one looking to upgrade your handling capabilities, HeadPowder Engineering can help you achieve optimal performance and operational success. With a strong presence in Shandong, China, and a reputation for excellence, they are the ideal partner for your powder handling needs.