

What is a Coke Powder Pneumatic Conveying System? What are its Design Principles?
Coke powder, a crucial material in industrial processes, requires efficient and reliable handling methods to ensure smooth operations. The coke powder pneumatic conveying system equipment has emerged as a sophisticated solution to meet these demands, offering a range of benefits from improved material flow to enhanced safety and operational efficiency. This article delves into the components, operational mechanisms, and design principles of such systems, providing a comprehensive overview for professionals in the field.
Introduction to Coke Powder Pneumatic Conveying Systems
Coke powder, derived from the carbonization of coal, is widely used in metallurgical, chemical, and other industrial applications. Traditional handling methods, such as manual conveying or mechanical systems, often face challenges like dust generation, material degradation, and inefficiencies. The coke powder pneumatic conveying system equipment addresses these issues by utilizing air as the medium to transport the powder, creating a closed-loop system that minimizes contamination and optimizes material movement. This technology has become indispensable in modern industrial settings, where precise and controlled material handling is critical.
Key Components of the Coke Powder Pneumatic Conveying System
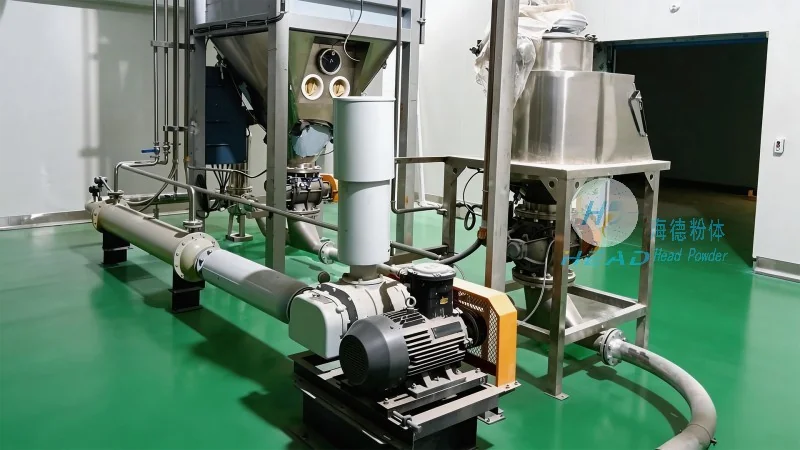
The coke powder pneumatic conveying system consists of several essential components that work in tandem to ensure effective operation. These include the material feed hopper, which holds the coke powder and controls the flow rate; the air compressor or blower, which generates the necessary air pressure to move the powder; the conveying line, typically made of stainless steel or other corrosion-resistant materials to prevent material buildup and contamination; and the receiver or discharge hopper, where the powder is collected after transportation. Additionally, the system may incorporate accessories like filters, cyclones, and pressure regulators to maintain air quality and system stability. Each component plays a vital role in the overall performance and reliability of the system.
Design Principles and Operational Mechanisms
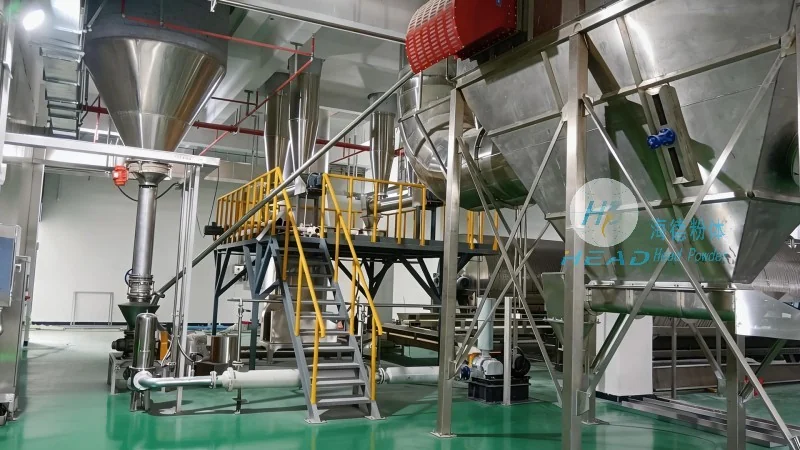
The design of a coke powder pneumatic conveying system is based on fundamental principles of fluid dynamics and material handling. The primary design principle is to maintain a consistent air flow rate and pressure to ensure the powder is transported efficiently without clogging or degradation. The system operates by creating a pressure differential between the feed and discharge points, using the air to lift and move the powder particles through the conveying line. The velocity of the air and the size of the powder particles are critical factors, as they determine the system's capacity and efficiency. Engineers must carefully calculate the air volume, pressure, and line dimensions to match the specific characteristics of the coke powder, such as particle size distribution, density, and moisture content. Proper design also considers factors like system scalability, maintenance requirements, and safety measures to ensure long-term operational success.
Advantages of Using a Coke Powder Pneumatic Conveying System
Implementing a coke powder pneumatic conveying system offers numerous advantages over traditional handling methods. One of the most significant benefits is the reduction of dust and contamination, as the system operates in a closed environment, preventing exposure to airborne particles. This not only enhances workplace safety but also maintains the quality of the coke powder by preventing moisture absorption or oxidation. Additionally, the system provides a high degree of control over material flow, allowing for precise dosing and batch processing. The compact design of the equipment saves space in industrial facilities, making it suitable for both new installations and retrofitting existing systems. Furthermore, the system's ability to handle abrasive materials like coke powder reduces wear and tear on components, leading to lower maintenance costs and longer equipment life. These advantages make the coke powder pneumatic conveying system an attractive solution for industries seeking to improve operational efficiency and product quality.
Applications and Industries
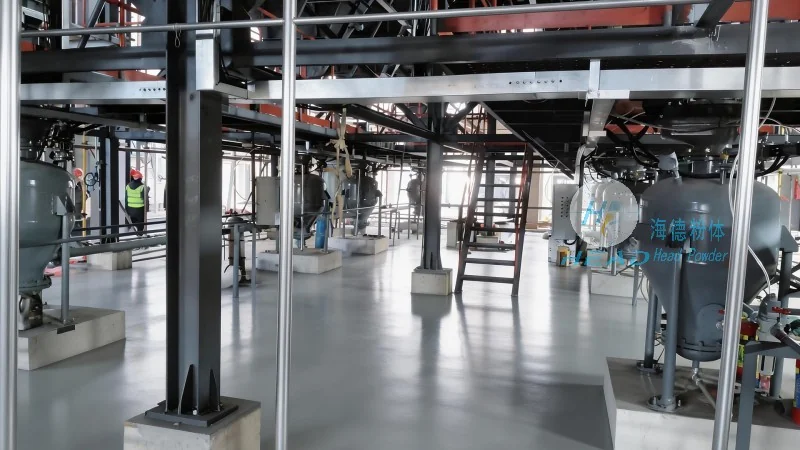
The coke powder pneumatic conveying system is widely used across various industries that rely on coke powder as a raw material. In the metallurgical industry, it is essential for transporting coke powder to blast furnaces and other processing units, ensuring a consistent supply of material for steel production. The chemical industry utilizes the system for handling coke powder in the production of chemicals, where precise material control is crucial for product quality. Additionally, the system is applied in the power generation sector, where coke powder is used as a fuel additive in boilers. Other industries, such as ceramics and refractory materials, also benefit from the system's ability to handle fine powders efficiently. The versatility of the coke powder pneumatic conveying system makes it a valuable asset in any industrial setting where reliable material handling is required.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer and supplier of advanced material handling systems, including coke powder pneumatic conveying equipment. With a strong commitment to innovation and quality, the company has established itself as a trusted partner in the industry, providing customized solutions tailored to the specific needs of clients. Headpowder's team of experienced engineers and technicians leverages cutting-edge technology and rigorous testing to develop systems that meet the highest standards of performance and reliability. The company's facilities, located in Shandong, China, are equipped with state-of-the-art manufacturing equipment and quality control measures to ensure each product meets or exceeds industry specifications. Headpowder's dedication to customer satisfaction and technological advancement has earned it a reputation for excellence in the market, making it a preferred choice for businesses seeking efficient and reliable coke powder handling solutions.