

Components of Quartz Stone Pneumatic Conveying
Quartz stone pneumatic conveying systems are sophisticated industrial solutions designed to transport quartz particles efficiently and safely. Understanding the components that make up these systems is crucial for optimizing performance, ensuring reliability, and maintaining operational efficiency. This article explores the key elements that constitute a typical quartz stone pneumatic conveying setup, highlighting the expertise of Shandong HeadPowder Engineering Co., Ltd. in designing and implementing such systems.
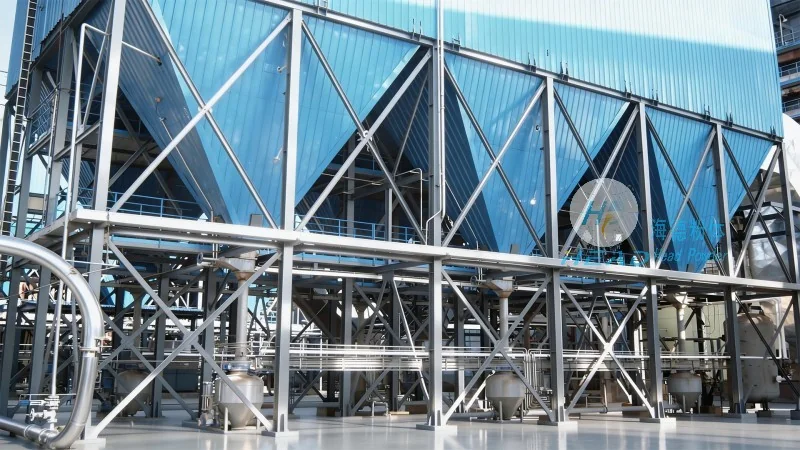
Key Components of the Pneumatic Conveying System
The core components of a quartz stone pneumatic conveying system work in concert to facilitate the movement of material from the source to the destination. These components include, but are not limited to, the following:
1. Feeding Equipment: This is the initial stage where quartz stone is introduced into the system. Feeding equipment such as hoppers, feeders, or vibratory feeders ensures a consistent and controlled flow of material into the conveying line. Proper feeding is essential to prevent blockages and maintain system stability.
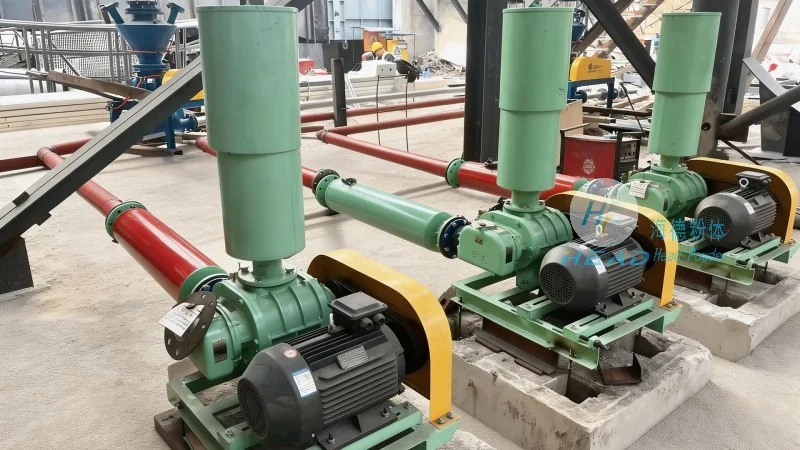
2. Pneumatic Conveying Line: The main body of the system, this is where the quartz particles are transported. The line consists of pipes or ducts that are either positive pressure or negative pressure systems. Positive pressure systems use air to push the material forward, while negative pressure systems use suction to draw the material. The choice of system depends on the material characteristics, distance, and environmental considerations.
3. Air Supply System: This component provides the necessary air or gas to power the conveying process. It includes compressors, air dryers, and filters to ensure the air is clean and dry, preventing contamination of the quartz stone and maintaining system efficiency.
4. Separation and Collection Equipment: At the receiving end, the system needs to separate the quartz particles from the air stream. This is typically achieved through cyclones, filters, or baghouses. These devices capture the material and return it to the process, while the air is either recirculated or discharged.
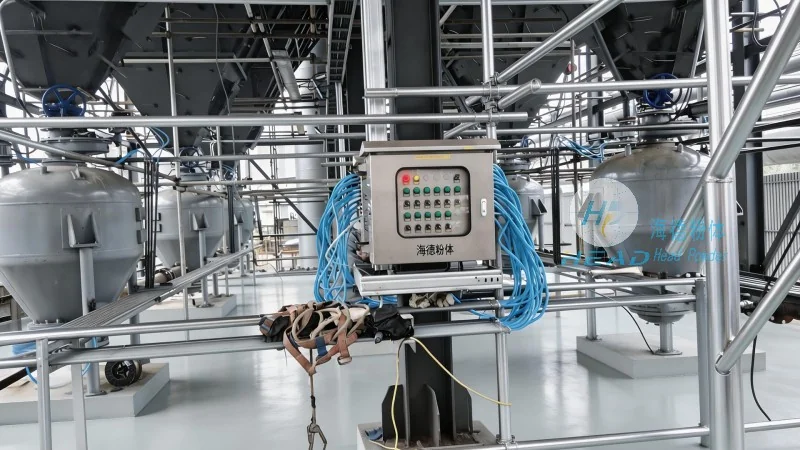
5. Control and Monitoring Systems: Modern pneumatic conveying systems are equipped with control panels and sensors to monitor pressure, flow rates, and other critical parameters. This allows for real-time adjustments and ensures the system operates within optimal conditions, enhancing safety and efficiency.
The Role of HeadPowder in Designing and Implementing These Systems
Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field, specializes in the design, manufacturing, and installation of quartz stone pneumatic conveying systems. With years of experience, HeadPowder understands the unique challenges associated with handling quartz stone, such as its abrasive nature and varying particle sizes. The company's engineers work closely with clients to assess their specific needs, including material properties, production capacity, and operational environment, to develop customized solutions.
HeadPowder employs advanced engineering techniques and high-quality materials to construct durable and reliable pneumatic conveying systems. The company's commitment to quality is evident in its adherence to industry standards and rigorous testing protocols. By leveraging its expertise, HeadPowder ensures that the components of the system are not only functional but also long-lasting, reducing maintenance costs and downtime for clients.
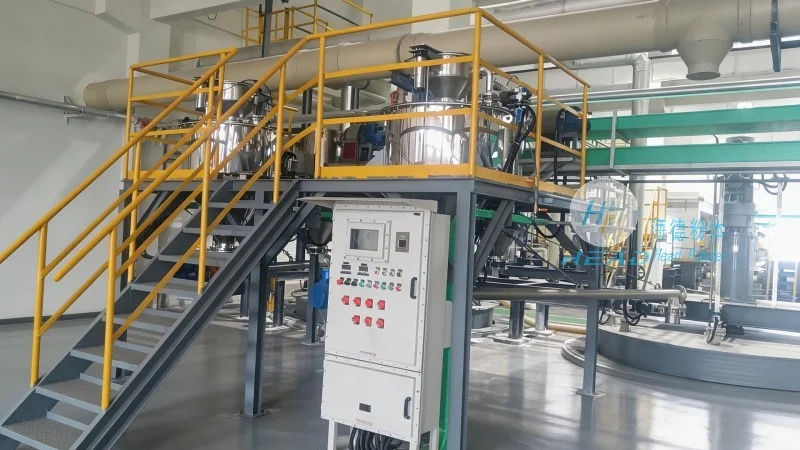
Furthermore, HeadPowder offers comprehensive support services, including system maintenance, troubleshooting, and upgrades. This holistic approach ensures that clients can rely on their quartz stone pneumatic conveying systems to operate at peak performance, meeting their production demands consistently.
Conclusion
In summary, quartz stone pneumatic conveying systems are composed of several critical components that work together to achieve efficient material transport. From the feeding equipment to the separation and collection systems, each part plays a vital role in the overall functionality of the system. Shandong HeadPowder Engineering Co., Ltd. stands out as a trusted partner in the industry, providing expert solutions tailored to the specific requirements of quartz stone handling. By understanding and implementing these components effectively, industries can enhance their operational efficiency and ensure the safe and reliable transport of quartz stone.