

Classification and Composition of Stone Pneumatic Conveying Systems
Stone pneumatic conveying systems are essential in various industrial applications, particularly in the construction and material handling sectors. These systems utilize air pressure to transport bulk materials like stones, gravel, and similar particulate materials over long distances or vertical heights. The design and functionality of such systems are tailored to meet specific operational requirements, ensuring efficient material transfer while maintaining system reliability and durability.
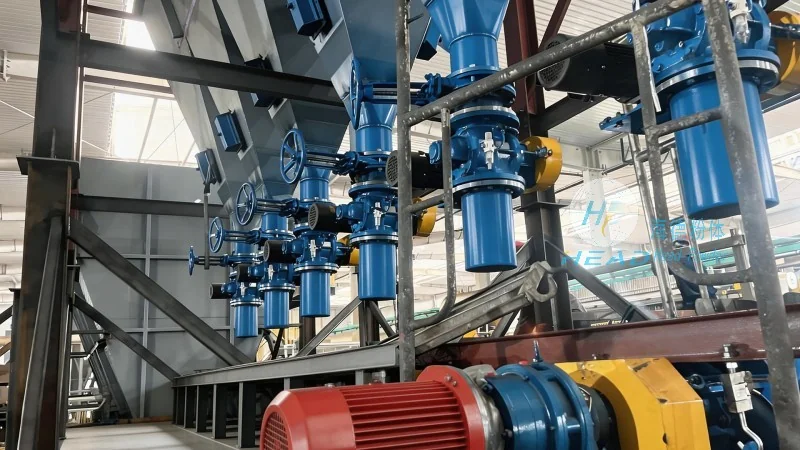
Classification of Stone Pneumatic Conveying Systems
Stone pneumatic conveying systems can be broadly classified based on the conveying principle and the pressure used. The primary classifications include:
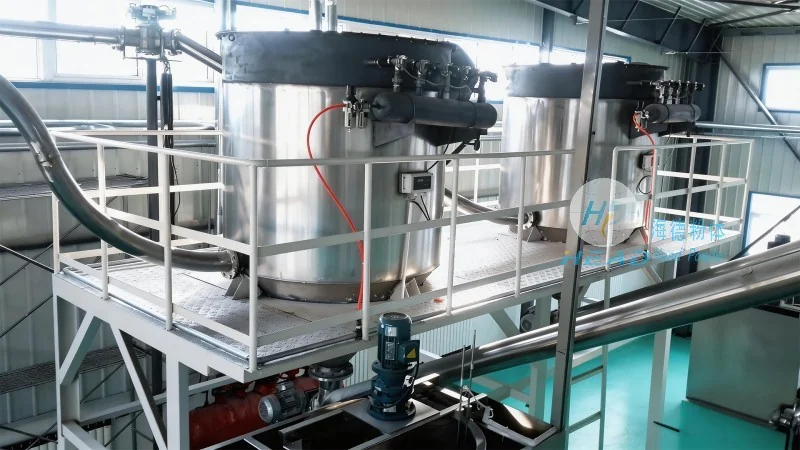
- Positive Pressure Systems: These systems use compressed air to push the material through the pipeline. The air is introduced at the inlet, creating a positive pressure that propels the material forward. This type is suitable for short to medium distances and can handle a wide range of particle sizes.
- Negative Pressure (Vacuum) Systems: In contrast, negative pressure systems use a vacuum to draw the material into the pipeline. The vacuum is created at the receiving end, pulling the material from the source. This method is ideal for applications requiring material to be transported from a higher elevation to a lower one or over longer distances.
- Two-Stage Systems: Combining elements of both positive and negative pressure, two-stage systems use a positive pressure section to move material from the source to an intermediate point and then a negative pressure section to transport it to the destination. This approach is beneficial for complex layouts and varying elevation changes.
Key Components of Stone Pneumatic Conveying Systems
Regardless of the classification, stone pneumatic conveying systems consist of several critical components that work in tandem to ensure effective operation. The main components include:
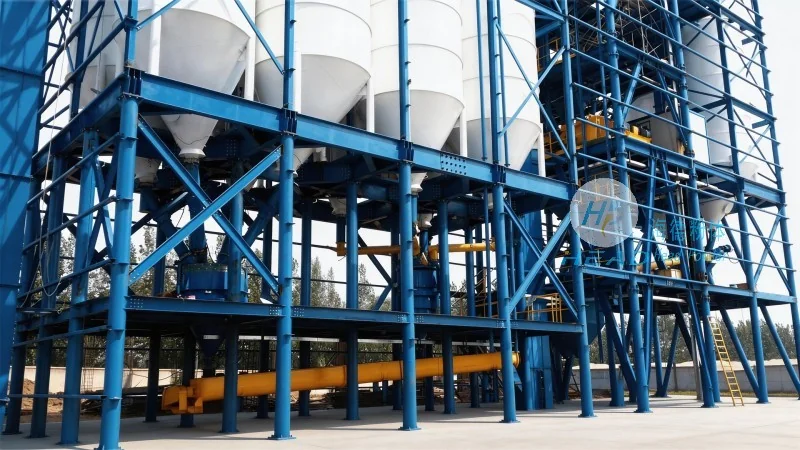
- Material Hopper or Source: This is where the stone material is stored before being fed into the system. The hopper is designed to hold the bulk material and provide a consistent feed rate to the conveyor. It may include a feeder, such as a rotary valve or a screw feeder, to control the flow of material.
- Conveying Pipeline: The pipeline is the main channel through which the material and air travel. It is typically made of stainless steel or other corrosion-resistant materials to withstand the abrasive nature of stone particles. The pipeline diameter and length are crucial factors in determining the system's capacity and efficiency.
- Air Supply or Vacuum Unit: This component provides the necessary air pressure or vacuum for the conveying process. In positive pressure systems, a blower or compressor generates compressed air, while in negative pressure systems, a vacuum pump creates the vacuum. The power and capacity of this unit must match the system's requirements to avoid underperformance or excessive energy consumption.
- Control Valves and Regulators: These components regulate the flow of air and material within the system. They include check valves, flow control valves, and pressure regulators to maintain stable operation and prevent backflow or pressure surges. Proper control ensures the system runs smoothly and efficiently.
- Receiver or Discharge Bin: The receiver is where the material is deposited after being conveyed. It is designed to collect the material and may include a discharge valve or a hopper to control the release of the material. The receiver's design should prevent material buildup and ensure easy access for maintenance.
- Filter and Dust Collection System: Due to the abrasive nature of stone particles, a filter system is essential to capture dust and fine particles that are carried along with the material. This system protects the air supply unit and the environment from contamination. It typically includes a filter housing, a fan, and a collection container.
Applications and Benefits of Stone Pneumatic Conveying Systems
Stone pneumatic conveying systems are widely used in various industries, including construction, mining, and material processing. Their applications range from transporting gravel and crushed stone for road construction to delivering sand and aggregates in concrete production. The key benefits of these systems include:
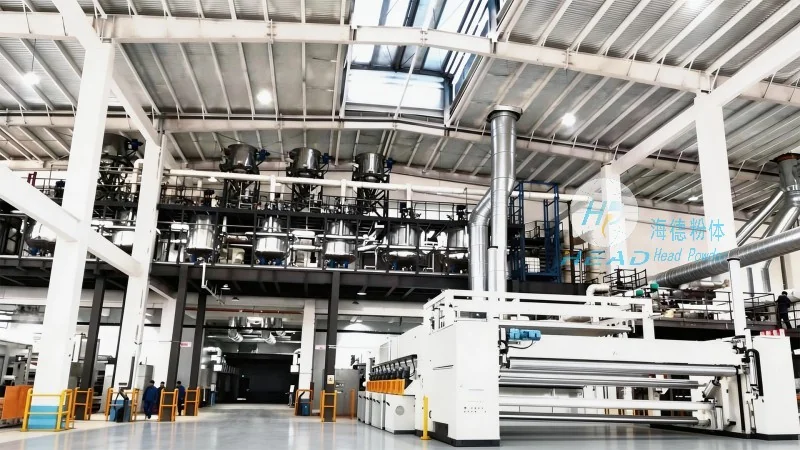
- Efficient Material Transfer: By using air as the conveying medium, these systems can transport materials over long distances and vertical heights with minimal energy consumption compared to traditional methods like belt conveyors or trucks.
- Reduced Labor and Maintenance: Automated systems require less manual labor for operation and maintenance, reducing operational costs and improving safety. The enclosed pipeline design also minimizes material spillage and dust exposure.
- Flexibility in Layout: Pneumatic conveying systems can be easily integrated into existing facilities or reconfigured to accommodate changes in production processes or layout requirements.
- Environmental Friendliness: By containing dust and preventing material spillage, these systems contribute to a cleaner working environment and comply with environmental regulations.
Conclusion
Stone pneumatic conveying systems are a vital component in modern material handling, offering efficient, flexible, and environmentally friendly solutions for transporting bulk stone materials. The classification and composition of these systems are tailored to meet specific operational needs, ensuring optimal performance and reliability. As a leading provider in the industry, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing high-quality stone pneumatic conveying systems that meet the diverse requirements of its clients.