

Operation Process and Working Principle of Air-Lifted Quartz Sand Particle Material Handling
Quartz sand, a widely used industrial material, often requires efficient and reliable transportation methods for various applications. Air-lifted material handling systems, also known as pneumatic conveying systems, offer a solution that effectively transports quartz sand particles through a pipeline using air or gas as the conveying medium. This article explores the operation process and working principles of such systems, focusing on their application in quartz sand handling.
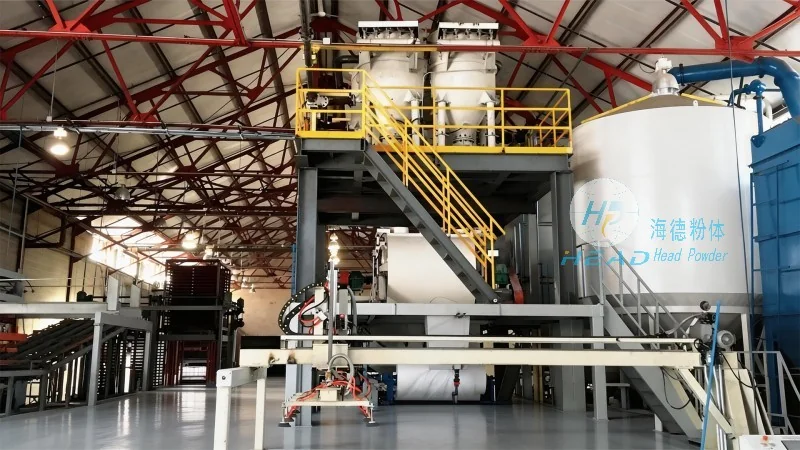
Introduction to Air-Lifted Material Handling Systems
HeadPowder, a leading provider of material handling solutions, specializes in designing and manufacturing air-lifted systems tailored for quartz sand and other granular materials. These systems are engineered to handle the unique characteristics of quartz sand, such as its particle size, density, and flowability, ensuring optimal performance and efficiency in industrial settings.
Key Components of the Air-Lifted System
The air-lifted material handling system consists of several critical components that work in tandem to transport quartz sand particles. The primary components include a hopper for material storage, a conveyor pipeline, a blower or compressor to generate airflow, a separator to separate air from the conveyed material, and a discharge point for the material. Each component plays a vital role in the overall operation of the system.
Operation Process of the Air-Lifted System
The operation process of an air-lifted system for quartz sand begins with the loading of the material into the hopper. As the material is fed into the system, the blower or compressor starts operating, generating a high-pressure airflow that is introduced into the conveyor pipeline. The airflow creates a negative pressure or positive pressure environment within the pipeline, depending on the system design, which draws the quartz sand particles into the pipeline.
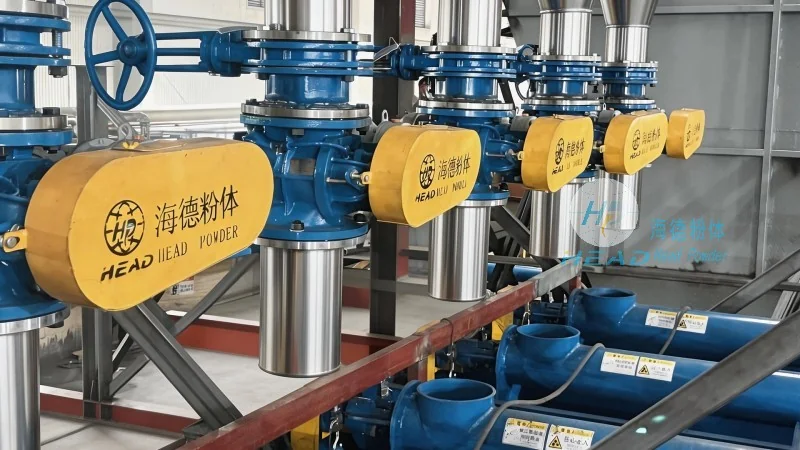
Once the particles are inside the pipeline, they are carried along by the airflow. The system may use different conveying modes, such as dilute phase or dense phase, to optimize the transport of quartz sand. Dilute phase conveying involves a low concentration of particles in the air stream, while dense phase conveying uses a higher concentration, providing better control over the material flow. The choice of conveying mode depends on the specific requirements of the quartz sand handling application.
Working Principle of the Air-Lifted System
The working principle of the air-lifted system is based on the principles of fluid dynamics and particle motion. The airflow generated by the blower creates a pressure differential between the inlet and outlet of the pipeline. This pressure differential propels the quartz sand particles through the pipeline. The particles are suspended in the air stream due to the drag force exerted by the airflow, allowing them to be transported over long distances without the need for mechanical components like belts or buckets.
The separator at the end of the pipeline plays a crucial role in separating the air from the quartz sand particles. It typically uses a cyclone or a filter to separate the particles from the air, allowing the quartz sand to be discharged into the receiving container. The separated air is then either recirculated back into the system or released into the atmosphere, depending on the system design and environmental regulations.
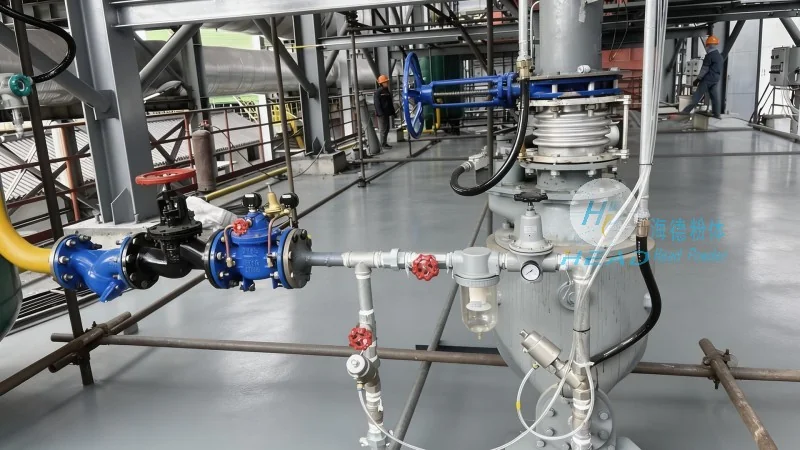
Advantages of Air-Lifted Material Handling for Quartz Sand
Using air-lifted systems for quartz sand handling offers several advantages over traditional mechanical conveying methods. These include reduced maintenance costs, as there are fewer moving parts, improved safety due to enclosed pipelines, and the ability to handle abrasive materials like quartz sand without causing wear and tear on the system components. Additionally, air-lifted systems can transport quartz sand over long distances with minimal energy consumption, making them an economical choice for industrial applications.
Application Examples in Quartz Sand Processing
HeadPowder's air-lifted systems are widely used in various applications within the quartz sand processing industry. For instance, in mining operations, these systems are used to transport mined quartz sand from the extraction site to processing facilities. In manufacturing plants, they are employed to move quartz sand from storage silos to production lines for further processing. The flexibility and adaptability of air-lifted systems make them suitable for a wide range of quartz sand handling scenarios, ensuring efficient material flow and reduced downtime.
Conclusion
HeadPowder Engineering Co., Ltd., based in Shandong, China, is a trusted provider of air-lifted material handling solutions for quartz sand and other granular materials. By understanding the operation process and working principles of these systems, industrial users can optimize their material handling operations, improve efficiency, and reduce costs. The air-lifted system's ability to handle quartz sand effectively and reliably makes it an essential component in modern industrial processes.