

Principle and Working Scene Characteristics of Borax Granular Material Pneumatic Conveying Machine
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and manufacturing of advanced pneumatic conveying systems tailored for various industrial applications. This article delves into the fundamental principles and operational characteristics of a borax granular material pneumatic conveying machine, highlighting its efficiency and adaptability in handling this specific chemical product.
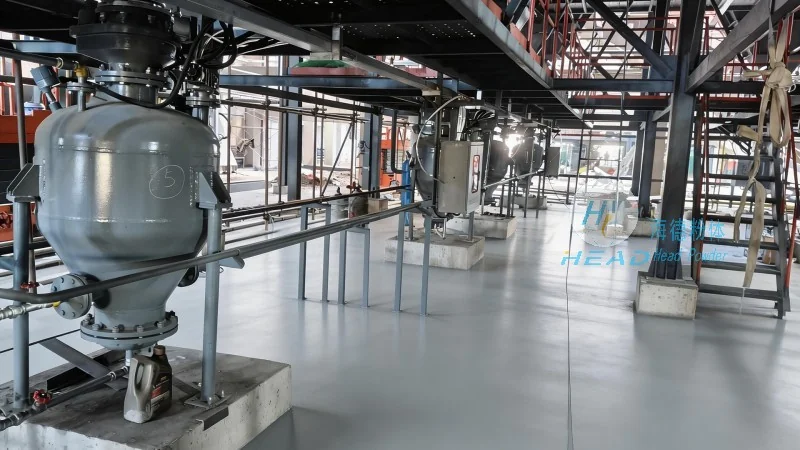
Introduction to Borax Granular Material Pneumatic Conveying
Borax, a widely used chemical compound in industries such as glass manufacturing, detergents, and agriculture, is often supplied in granular form. Traditional methods of transporting borax granules, like belt conveyors or bucket elevators, may face challenges like material degradation, dust generation, and high maintenance costs. Pneumatic conveying offers a more efficient and hygienic solution, especially for handling fine or dusty materials like borax. The borax granular material pneumatic conveying machine leverages the principles of air flow to transport the material from a source to a destination, minimizing contact with external elements and reducing operational risks.
Core Principles of Pneumatic Conveying for Borax Granules
The operation of a borax granular material pneumatic conveying machine is based on the fundamental principle of using air as a medium to transport solid particles. The system typically consists of a hopper, a rotary valve, a conveying pipe, a fan or blower, and a receiver. The process begins when the borax granules are fed into the hopper. A rotary valve then controls the flow of material into the conveying pipe, where the fan generates a high-velocity air stream. The air stream carries the granules through the pipe to the receiver, where the material is deposited. The air, now containing the conveyed particles, is then filtered and recycled back into the system, ensuring energy efficiency and minimal waste.
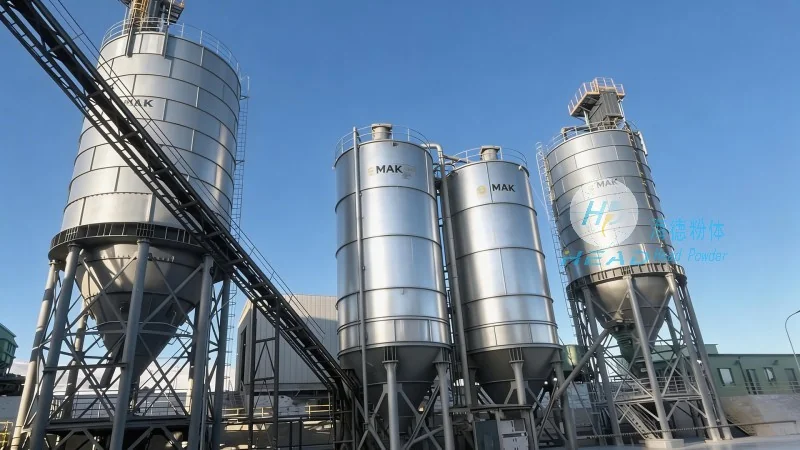
Key Components and Their Functions
Each component of the borax granular material pneumatic conveying machine plays a critical role in the overall operation. The hopper serves as the storage and feeding unit, ensuring a consistent supply of granules. The rotary valve acts as a controlled gate, regulating the flow rate of the material into the conveying pipe to prevent blockages and maintain system stability. The conveying pipe is designed with smooth internal surfaces to minimize friction and particle attrition. The fan or blower provides the necessary air pressure and velocity to move the granules through the system. Finally, the receiver collects the delivered borax granules and may include a dust collection system to ensure environmental compliance and product purity.
Working Scene Characteristics and Applications
The borax granular material pneumatic conveying machine is particularly suited for industrial environments where precision, cleanliness, and efficiency are paramount. In glass manufacturing plants, for example, borax granules are used as a flux to lower the melting point of silica. The pneumatic conveying system allows for seamless integration with the glass production line, ensuring a steady supply of borax without interrupting the manufacturing process. Similarly, in detergent production facilities, the system can handle borax granules in a controlled manner, reducing dust exposure for workers and maintaining product quality. The machine's ability to operate in a closed system also minimizes environmental impact, making it an ideal choice for industries with strict regulatory requirements.
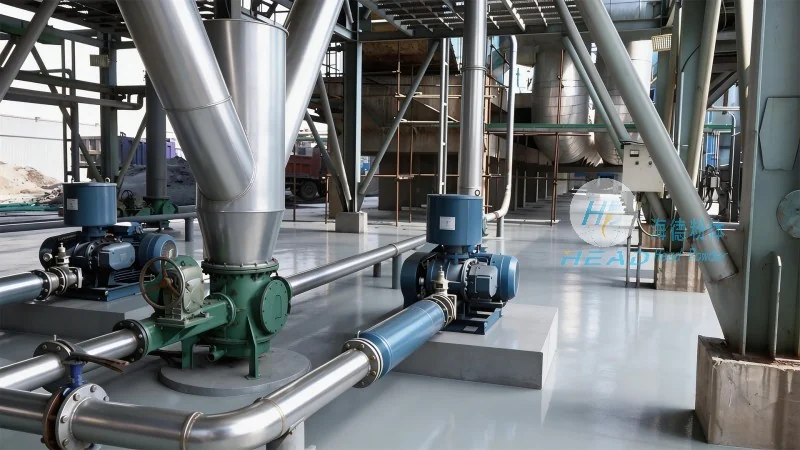
Advantages of Using a Borax Granular Material Pneumatic Conveying Machine
Compared to traditional bulk handling methods, the borax granular material pneumatic conveying machine offers several advantages. Firstly, it provides a dust-free and hygienic environment, which is crucial for food and pharmaceutical industries where product contamination must be avoided. Secondly, the system is highly efficient, with minimal energy consumption due to the recycling of air. Thirdly, it reduces labor costs by automating the material handling process, as the machine can operate continuously without the need for manual intervention. Additionally, the closed system design prevents material loss and contamination, ensuring consistent product quality. These advantages make the borax granular material pneumatic conveying machine a cost-effective and reliable solution for borax handling in various industrial applications.
Conclusion and Company Overview
HeadPowder Engineering Co., Ltd., with its headquarters in Shandong, China, is committed to providing innovative and reliable pneumatic conveying solutions for the chemical industry. The borax granular material pneumatic conveying machine exemplifies the company's expertise in designing systems that meet the specific needs of industrial clients. By leveraging advanced engineering principles and high-quality materials, HeadPowder ensures that its products deliver optimal performance, durability, and efficiency. For industries dealing with borax granules, the pneumatic conveying machine is an essential tool for maintaining production continuity, enhancing product quality, and reducing operational costs. HeadPowder continues to be a trusted partner in the development and implementation of efficient material handling solutions for the global chemical industry.