

Principle and Working Scene Characteristics of Ammonium Nitrate Powder Pneumatic Conveying System
Ammonium nitrate is a widely used industrial chemical, often handled in bulk powder form. The pneumatic conveying system is an efficient method for transporting such powders over long distances or within industrial facilities. This article explores the fundamental principles behind these systems and highlights the specific characteristics of their application in scenarios involving ammonium nitrate powder. Developed by Shandong HeadPowder Engineering Co., Ltd., a leading provider of specialized engineering solutions for bulk material handling, these systems are designed to meet the stringent requirements of industries dealing with hazardous materials like ammonium nitrate.
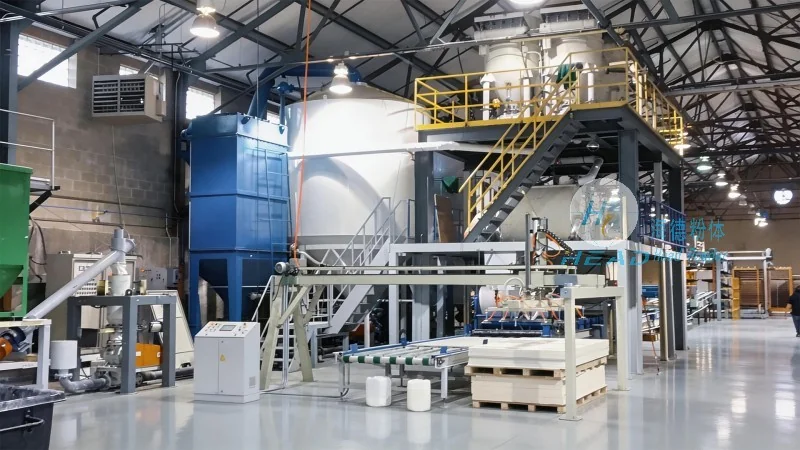
Core Principles of Pneumatic Conveying for Ammonium Nitrate
The pneumatic conveying system operates by using compressed air or other gases to transport particulate materials through a pipeline. In the case of ammonium nitrate, the system must be designed to handle the material's properties, such as its density, flowability, and potential reactivity. The system typically consists of a feeding device, a conveying line, a separation unit, and a discharge mechanism. The feeding device ensures a consistent flow of powder into the system, while the conveying line transports the material using air pressure. The separation unit, often a cyclone or a filter, separates the powder from the air stream, and the discharge mechanism delivers the powder to its final destination. The choice of conveying method—such as dilute phase or dense phase—depends on factors like the distance to be covered, the required flow rate, and the material's characteristics. For ammonium nitrate, a dilute phase system is commonly used due to its ability to handle long distances and maintain material integrity.
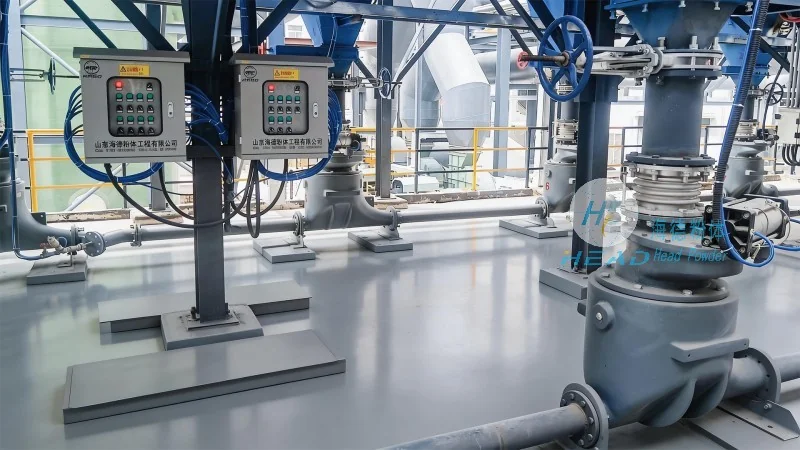
Working Scene Characteristics of Ammonium Nitrate Pneumatic Conveying
The application of ammonium nitrate powder pneumatic conveying systems varies across different industrial settings. In fertilizer production facilities, these systems are used to transport raw ammonium nitrate from storage silos to processing units or to distribute it to packaging lines. The systems must be designed to minimize dust generation and ensure safe handling, as ammonium nitrate is a hazardous material under certain conditions. In mining operations, the systems may be used to transport ammonium nitrate from processing plants to storage or to other processing sites. The working scene characteristics also include considerations for environmental regulations, as the handling of ammonium nitrate requires compliance with safety and environmental standards. The systems are typically installed in enclosed or controlled environments to prevent dust dispersion and to ensure worker safety. Additionally, the design must account for the material's potential to cause dust explosions, requiring proper explosion-proof measures in the system components.
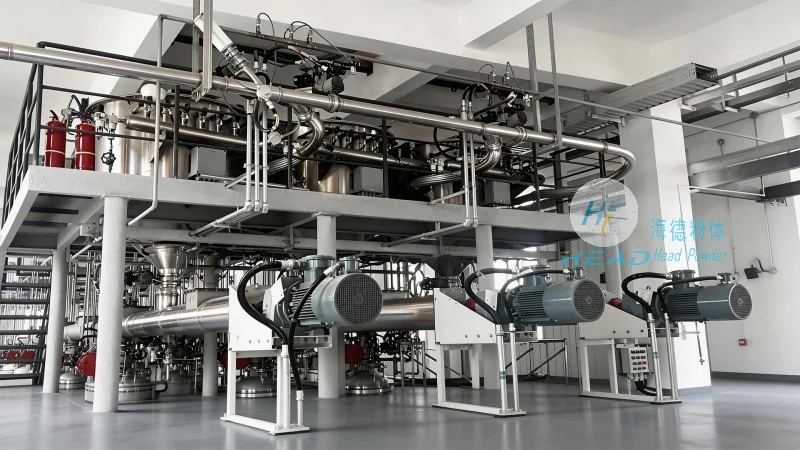
Key Features and Advantages of Ammonium Nitrate Pneumatic Conveying Systems
Ammonium nitrate powder pneumatic conveying systems offer several advantages over traditional mechanical conveying methods. One of the primary benefits is the ability to transport materials over long distances without the need for intermediate transfer points or elevators. This reduces the risk of material degradation and contamination. The systems also provide a closed-loop operation, which minimizes dust exposure and improves workplace safety. Additionally, the flexibility of pneumatic conveying allows for easy integration with other industrial processes, such as mixing or packaging. The systems are designed to handle varying flow rates and material loads, making them suitable for both continuous and batch operations. For ammonium nitrate, the systems are engineered to maintain the material's quality and prevent caking or agglomeration during transport. This is crucial for maintaining the material's performance in downstream applications, such as fertilizer production or chemical processing.