

Principle and Working Scene Characteristics of Hydrogen Chloride Powder Pneumatic Conveying System
Hydrogen chloride (HCl) is a highly corrosive and reactive gas, commonly used in various industrial processes such as chemical synthesis, metal processing, and water treatment. When handled as a powder, it presents unique challenges for material handling and transportation. Pneumatic conveying systems have emerged as an effective solution for safely and efficiently transporting HCl powder from production sites to processing or storage facilities. This article explores the fundamental principles behind HCl powder pneumatic conveying systems and highlights the key working scene characteristics that define their application in industrial settings.
The Core Principles of Pneumatic Conveying for HCl Powder
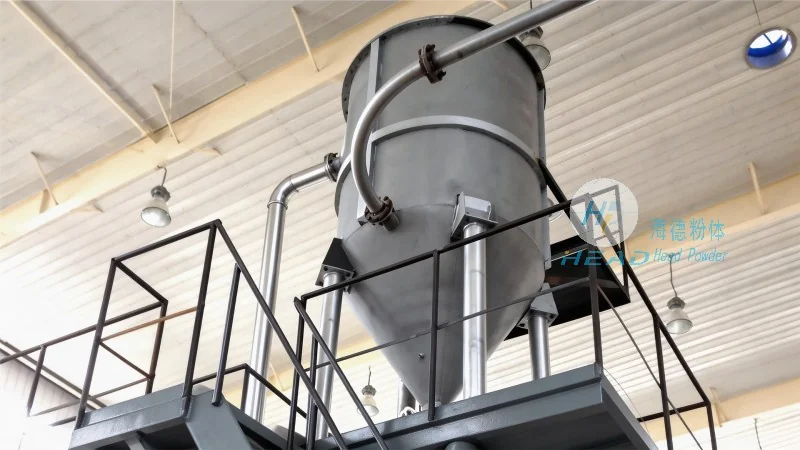
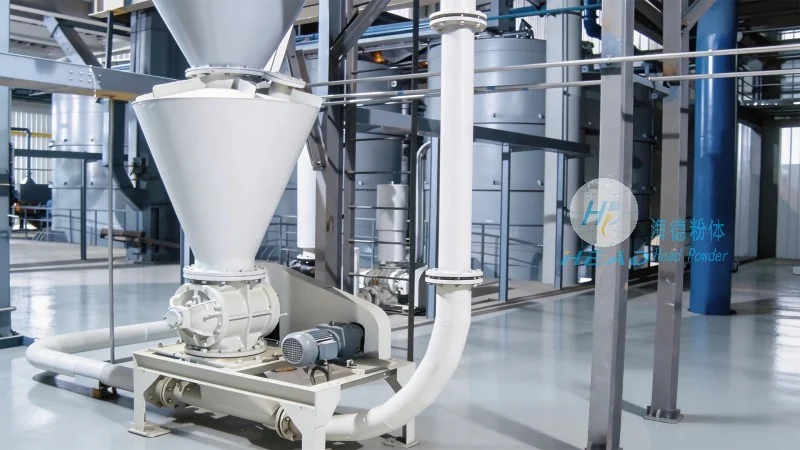
The operation of a hydrogen chloride powder pneumatic conveying system is based on the principle of transporting solid particles through a pipeline using a gas stream, typically air or a specialized inert gas. The system consists of several critical components, including a material feed hopper, a conveying line, a control valve, and a discharge point. The process begins with the powder being fed into the hopper, where it is then drawn into the conveying line by the moving gas. The gas velocity is carefully controlled to ensure that the powder particles are fully entrained and transported without clogging or degradation. The key to successful HCl powder conveying lies in maintaining the appropriate gas flow rate and pressure, which directly impacts the system's efficiency and safety. For HCl, which is highly corrosive, the materials used in the system components—such as stainless steel, PTFE, or specialized coatings—are crucial to prevent material degradation and ensure long-term operational reliability.
Key Working Scene Characteristics of HCl Powder Pneumatic Conveying Systems
The application of HCl powder pneumatic conveying systems varies across different industrial environments, each with distinct characteristics that influence system design and performance. One common working scene is in chemical manufacturing plants where HCl is produced as a byproduct or a raw material. In such settings, the system must handle large volumes of powder and integrate seamlessly with existing production lines. The working environment is often characterized by high temperatures and the presence of other corrosive chemicals, requiring robust system design and regular maintenance to ensure consistent performance. Another typical working scene is in metal processing facilities, where HCl is used for pickling and cleaning operations. Here, the system must be capable of handling abrasive particles and maintaining a clean, dust-free environment to prevent contamination of the processed metal surfaces. Additionally, in water treatment plants, HCl is used for pH adjustment and disinfection. The pneumatic conveying system in this context must meet stringent safety and environmental regulations, as HCl is a hazardous substance that requires careful containment and disposal. The working scene characteristics also include the need for flexibility in conveying distances and the ability to handle varying powder flow rates, which may fluctuate based on production schedules or demand.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
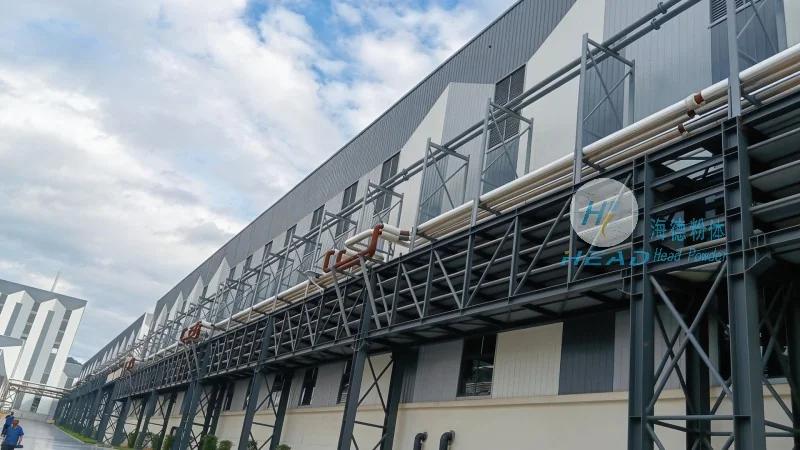
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name HeadPowder, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems for various industrial applications. With a focus on safety, efficiency, and durability, HeadPowder has established itself as a leading provider of HCl powder handling solutions. The company's headquarters is located in Shandong, China, where it leverages local expertise and resources to develop cutting-edge technologies tailored to the unique challenges of HCl powder transportation. HeadPowder's team of engineers and technicians work closely with clients to understand their specific operational requirements, ensuring that the delivered systems are optimized for performance and compliance with industry standards. The company's commitment to quality and innovation has earned it a reputation for delivering reliable and long-lasting pneumatic conveying solutions that meet the demanding needs of modern industrial processes.