

Principle and Working Scene Characteristics of Calcium Carbonate Limestone Powder Material Handling
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced material handling systems tailored for calcium carbonate and limestone powder applications. This article delves into the core principles and operational characteristics of their material handling equipment, providing insights into how these systems efficiently manage the unique challenges of handling fine powders in industrial settings.
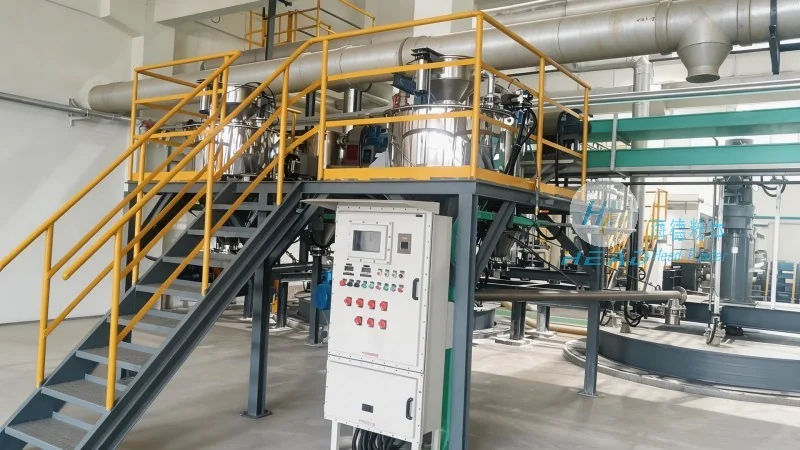
Overview of the Material Handling System
The calcium carbonate limestone powder material handling system is engineered to address the specific demands of processing and transporting fine powders. At its core, the system integrates multiple components, including feeders, conveyors, and control units, to ensure seamless material flow from storage to processing or packaging stages. The design prioritizes efficiency, reliability, and safety, making it suitable for various industrial applications where consistent and high-volume powder handling is required.
Working Principle of the System
The system operates on a closed-loop mechanism that ensures precise control over the material flow. Initially, the limestone powder is fed into the system through a hopper or bulk storage container. A feeder, typically a screw or vibratory type, regulates the material discharge rate, preventing overloading and maintaining consistent feed to the conveyor. The conveyor, often a belt or pneumatic type, transports the powder to the next processing stage or storage area. Advanced control systems monitor parameters such as flow rate, pressure, and temperature, adjusting operations in real-time to optimize performance and prevent equipment damage.
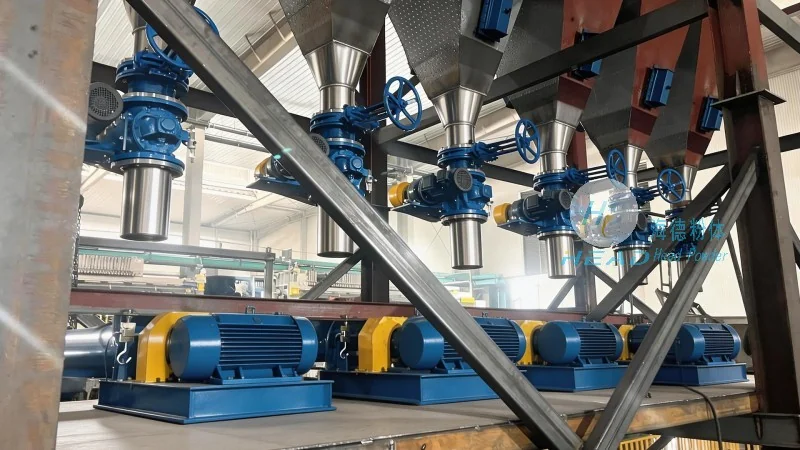
Key Working Scene Characteristics
The material handling system is designed to operate in diverse industrial environments, each with distinct requirements. In mining and quarrying operations, the system efficiently handles raw limestone ore, processing it into fine powder for further use. In manufacturing plants, it supports the production of calcium carbonate-based products, such as coatings, plastics, and paper, by ensuring a steady supply of high-quality powder. The system's adaptability allows it to be integrated into existing production lines, enhancing overall operational efficiency and reducing downtime.
Benefits and Advantages
Implementing this material handling system offers several advantages for industrial operations. The precise control over material flow minimizes waste and reduces the risk of product contamination, which is critical in applications where powder quality is paramount. The system's durability and low maintenance requirements contribute to long-term cost savings, as it requires minimal downtime for repairs or adjustments. Additionally, the system's scalability allows it to be customized to meet the specific needs of different production capacities, making it a versatile solution for various industries.
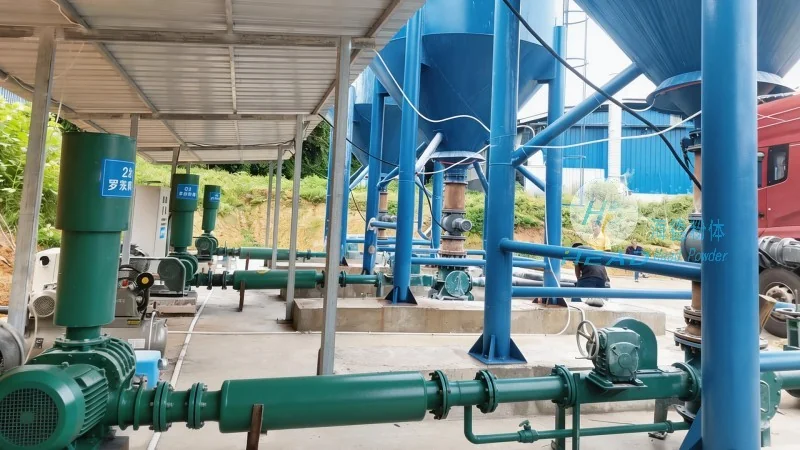
Application Examples
HeadPowder's material handling systems have been successfully deployed in several industries, demonstrating their effectiveness in real-world scenarios. For instance, in a calcium carbonate production facility, the system efficiently processes limestone ore into fine powder, which is then used to manufacture high-quality fillers for the paper industry. In another application, the system supports the production of plastic additives, ensuring a consistent supply of powder that meets stringent quality standards. These examples highlight the system's versatility and reliability in handling different types of calcium carbonate and limestone powders.
Conclusion
HeadPowder's calcium carbonate limestone powder material handling system represents a sophisticated solution for industrial material processing. By combining advanced technology with robust design, the system addresses the unique challenges of handling fine powders, ensuring efficient, reliable, and safe operations. As a leading company in Shandong, China, HeadPowder continues to innovate and provide tailored solutions that meet the evolving needs of industrial clients, enhancing productivity and operational excellence in material handling applications.