

Principle and Working Scene Characteristics of Rare Earth Powder Conveying System Equipment
HeadPowder, a leading enterprise in the field of powder handling technology, specializes in the design, manufacturing, and supply of advanced rare earth powder conveying systems. The company, with its headquarters in Shandong, China, has established itself as a key player in providing efficient and reliable solutions for the transportation of rare earth powders, which are critical components in modern industrial applications.
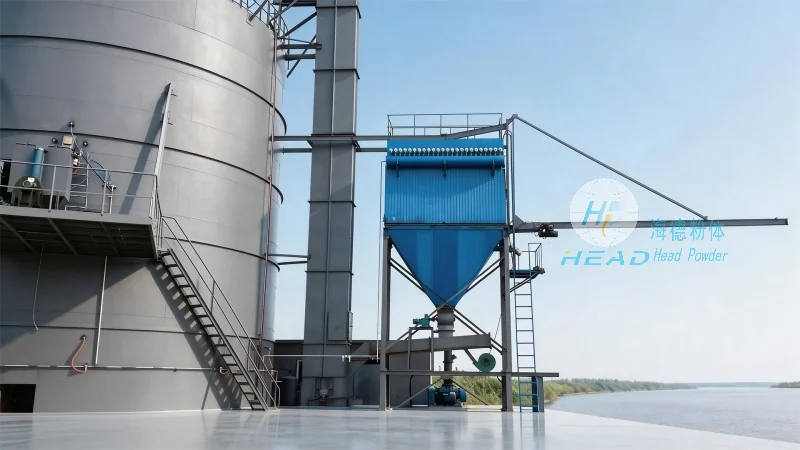
Overview of Rare Earth Powder Conveying Systems
At the core of HeadPowder's product line is the rare earth powder conveying system, engineered to handle the unique challenges associated with transporting these valuable materials. These systems are designed to ensure minimal product loss, maintain consistent particle size distribution, and provide a clean, dust-free operation environment. The equipment is built with materials that are resistant to corrosion and wear, ensuring long-term durability and low maintenance costs.
The Working Principle of the Conveying Equipment
The operation of the rare earth powder conveying system is based on a combination of mechanical and pneumatic principles. The system typically incorporates a hopper for material storage, a feeding mechanism to control the flow rate, and a conveying component such as a screw conveyor, pneumatic duct, or air slide. The feeding mechanism, often a rotary valve or a vibratory feeder, regulates the amount of powder entering the conveying line, preventing overloading and ensuring smooth operation. The conveying component then transports the powder from the source to the destination, with the pneumatic system utilizing compressed air to create a flow that moves the particles through the ducts. This method is particularly effective for fine powders, as it minimizes particle degradation and maintains the integrity of the material.
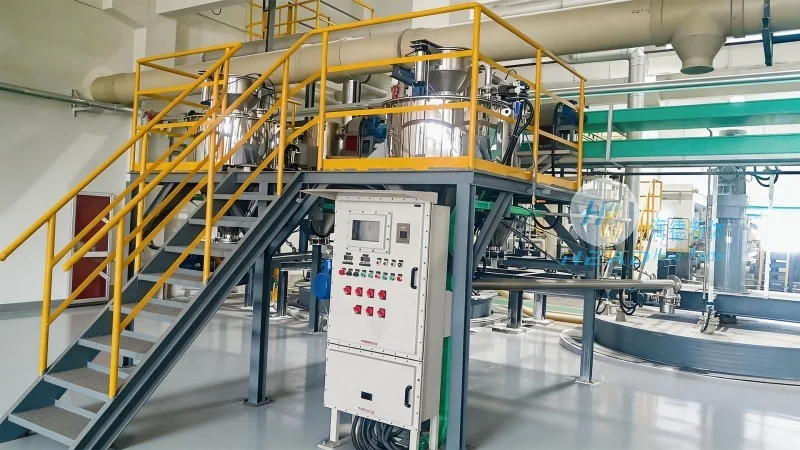
Key Working Scene Characteristics
The working scene characteristics of the rare earth powder conveying system are tailored to meet the specific demands of industrial environments. These systems are designed for high throughput, allowing for the efficient handling of large volumes of rare earth powders in manufacturing and processing facilities. The equipment is also equipped with safety features, such as dust extraction systems and explosion-proof components, to comply with industrial safety standards and protect both personnel and the environment. Additionally, the modular design of the system enables easy integration into existing production lines, reducing downtime and facilitating maintenance.
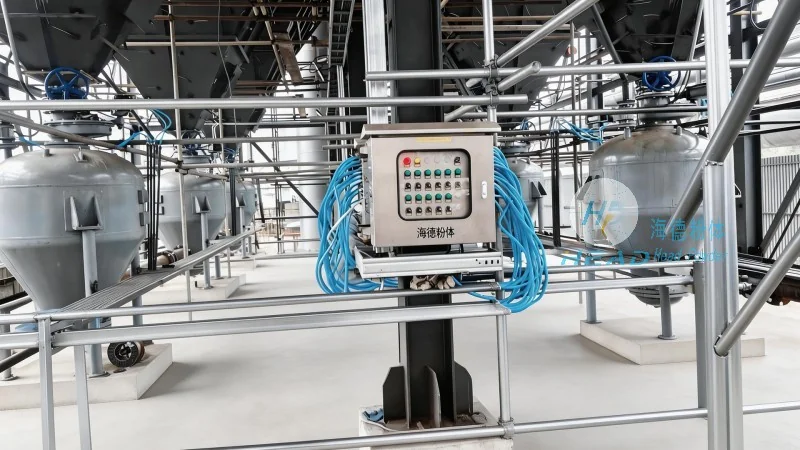
Application and Operational Advantages
HeadPowder's rare earth powder conveying systems are widely used in various industrial applications, including the production of rare earth magnets, catalysts, and other high-tech materials. The systems offer several operational advantages, including improved process efficiency, reduced labor costs, and enhanced product quality. By maintaining a consistent flow rate and particle size, the equipment ensures that downstream processes receive a uniform material, leading to better product consistency and reduced waste. Furthermore, the use of advanced control systems allows for real-time monitoring and adjustment of the conveying parameters, optimizing performance and minimizing energy consumption.
Conclusion and Company Information
HeadPowder Engineering Co., Ltd., based in Shandong, China, continues to innovate and provide cutting-edge solutions for rare earth powder handling. The company's commitment to quality, reliability, and customer satisfaction has made it a trusted partner for industries relying on efficient and safe powder transportation. With a focus on technological advancement and customer needs, HeadPowder remains at the forefront of developing advanced conveying systems that meet the evolving demands of modern manufacturing.