

Principle and Working Scene Characteristics of Feather Powder Conveying System Equipment
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, specializes in the design, development, and production of advanced feather powder conveying system equipment. The company has established itself as a key player in the field of powder handling technology, particularly for applications involving feather powder, which is widely used in various industries such as feed production, food processing, and chemical manufacturing.
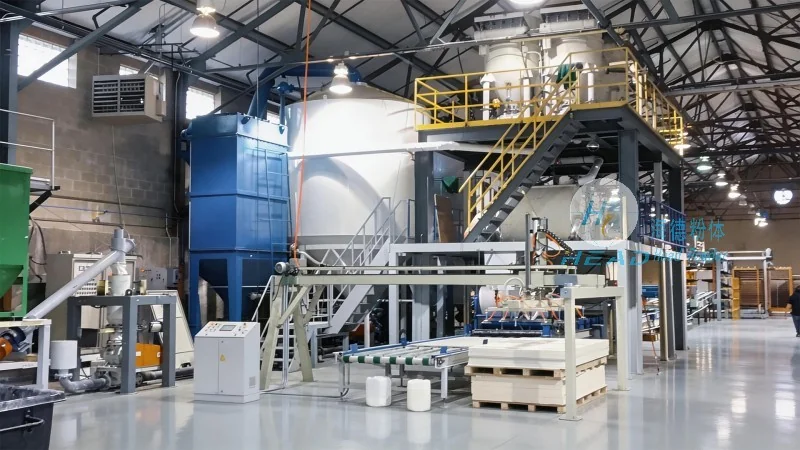
Overview of Feather Powder Conveying System Equipment
The feather powder conveying system equipment is engineered to efficiently transport fine powder materials, including feather powder, over long distances with minimal loss and contamination. This equipment is essential for industries that require reliable and hygienic powder handling solutions, ensuring product integrity and operational efficiency. The system typically integrates several key components, each playing a critical role in the overall conveying process.
Working Principle of the Conveying System
The core principle of the feather powder conveying system is based on pneumatic conveying technology. It utilizes a combination of air flow and pressure to move the powder particles through a network of pipes. The process begins with the feeding of feather powder into the system, where it is introduced into a hopper or feeder. From there, the powder is accelerated by a high-pressure air stream, which propels it through the conveying line. The system may employ different types of conveying modes, such as dilute phase or dense phase, depending on the specific requirements of the application. Dilute phase conveying uses low-pressure air to transport the powder in a dispersed state, while dense phase conveying employs higher pressure to move the powder in a more concentrated form, reducing particle separation and improving material handling.
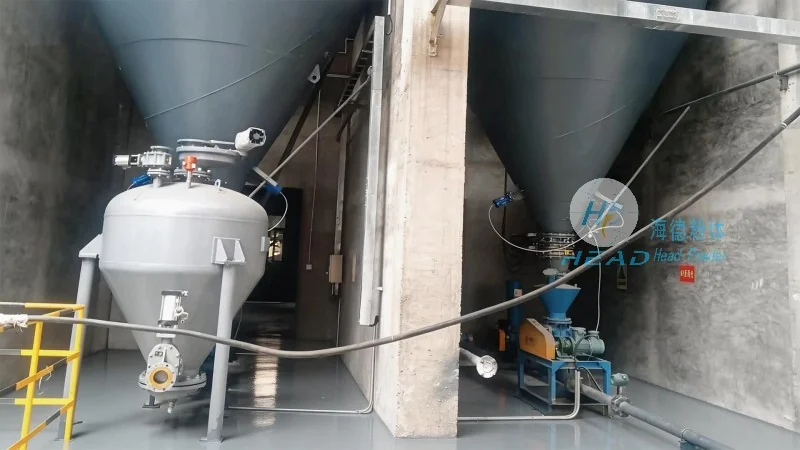
Key Components and Their Functions
The feather powder conveying system consists of several critical components that work in tandem to ensure smooth operation. The main components include the feeding device, conveying pipeline, separation and cleaning system, and control unit. The feeding device, such as a rotary valve or screw feeder, regulates the flow of feather powder into the system, preventing blockages and maintaining consistent material input. The conveying pipeline, made from materials like stainless steel or plastic, is designed to withstand the abrasive nature of the powder and resist corrosion. The separation and cleaning system, which may include cyclones or filters, removes any excess moisture or contaminants from the air, ensuring that the powder remains clean and free from impurities. The control unit monitors and adjusts the system parameters, such as air pressure and flow rate, to optimize performance and prevent system failures.
Working Scene Characteristics and Applications
The feather powder conveying system is designed to operate in diverse industrial environments, adapting to various working conditions and requirements. Its versatility makes it suitable for a wide range of applications, including feed mills, poultry processing facilities, and food processing plants. In feed mills, the system efficiently transports feather powder from storage silos to mixing and processing areas, ensuring uniform mixing with other feed ingredients. In poultry processing plants, it handles the powder generated during feather removal and processing, preventing dust accumulation and maintaining a clean working environment. The system's ability to handle fine powders without clogging or degradation makes it ideal for applications where product quality and purity are paramount.
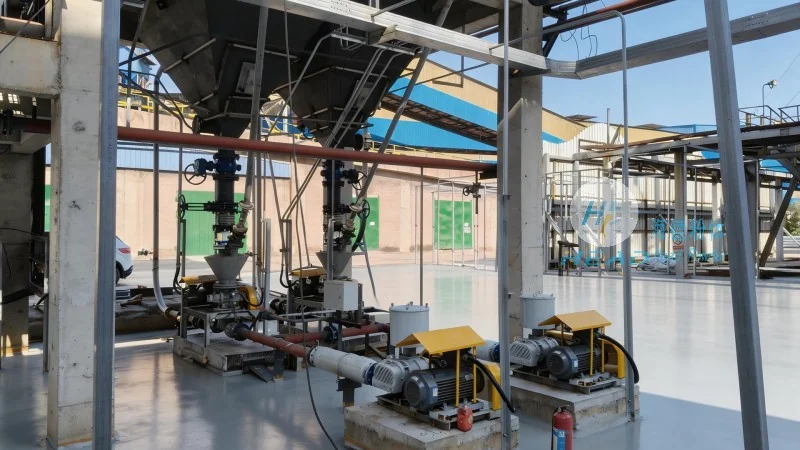
Advantages and Benefits of the System
Implementing the feather powder conveying system offers numerous advantages for industrial operations. One of the primary benefits is the reduction in labor costs and manual handling, as the system automates the entire powder transport process. This not only increases operational efficiency but also minimizes the risk of product contamination and worker exposure to dust. Additionally, the system reduces material loss and waste, as it minimizes the risk of spillage and dust dispersion during transport. The hygienic design of the equipment, with smooth surfaces and easy-to-clean components, ensures compliance with industry standards and regulations, particularly in food and feed processing industries. Furthermore, the system's energy efficiency, achieved through optimized air flow and pressure control, helps reduce operational costs and environmental impact.
Conclusion
Shandong HeadPowder Engineering Co., Ltd.'s feather powder conveying system equipment represents a reliable and efficient solution for industries requiring advanced powder handling technology. By leveraging pneumatic conveying principles and robust design, the system ensures consistent performance, minimal maintenance, and high product quality. With its adaptability to various working conditions and applications, the equipment is a valuable asset for businesses seeking to enhance their operational efficiency and maintain compliance with industry standards. The company's commitment to innovation and quality ensures that customers receive equipment tailored to their specific needs, supporting their long-term success in the market.