

Principle and Working Scene Characteristics of Head Powder Bulk Material Conveyors
HeadPowder, a professional manufacturer based in Shandong, China, specializes in the design and production of bulk material conveying equipment. The company, Shandong HeadPowder Engineering Co., Ltd., has been committed to providing efficient and reliable solutions for powder handling in various industrial applications. This article explores the fundamental principles behind the operation of their bulk material conveyors and highlights the key working scene characteristics that make these systems effective in real-world industrial settings.
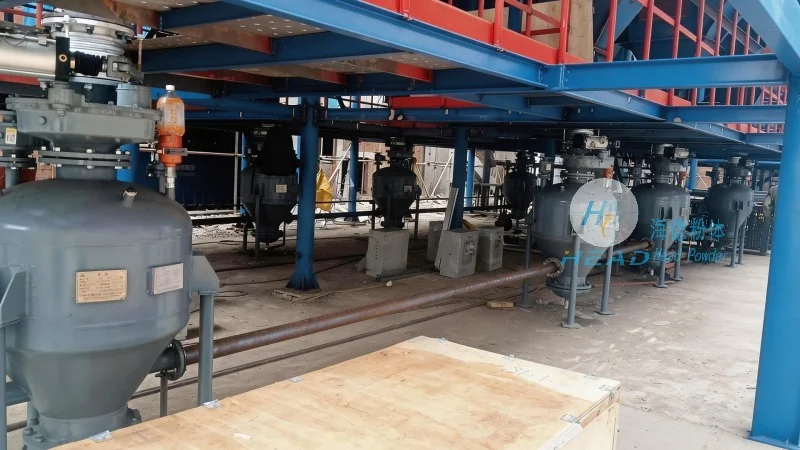
Overview of Bulk Material Conveyors by HeadPowder
HeadPowder's bulk material conveyors are engineered to handle a wide range of powders and granular materials with precision and efficiency. These systems are designed to meet the demands of industries such as food processing, pharmaceuticals, chemicals, and mining, where consistent and safe material transport is critical. The company's focus on innovation ensures that their conveyors are equipped with advanced features that enhance performance and durability.
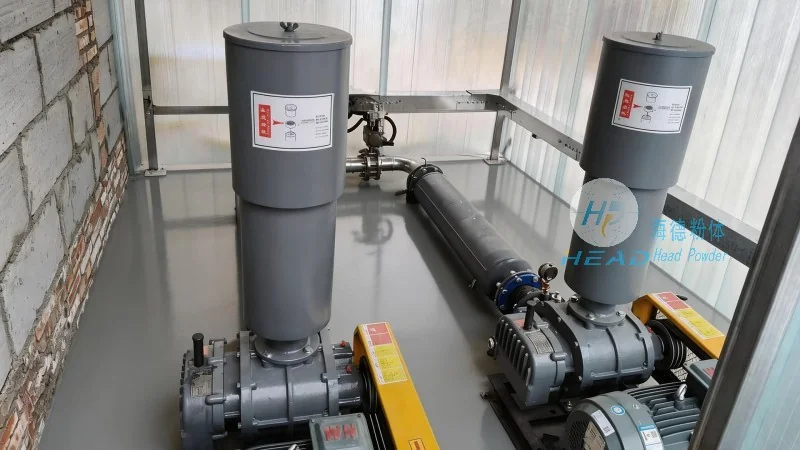
The Core Principle of Powder Material Conveying
The operation of HeadPowder's bulk material conveyors is based on the principle of pneumatic or mechanical transport, depending on the specific application requirements. For pneumatic systems, the conveyor uses compressed air to create a flow of material through a pipeline, while mechanical systems employ rotating components like screws or belts to move the material. Both methods are designed to maintain the integrity of the material, preventing segregation and ensuring uniform flow. The design incorporates features such as adjustable speed controls, material flow monitoring, and safety mechanisms to optimize performance and ensure operational safety.
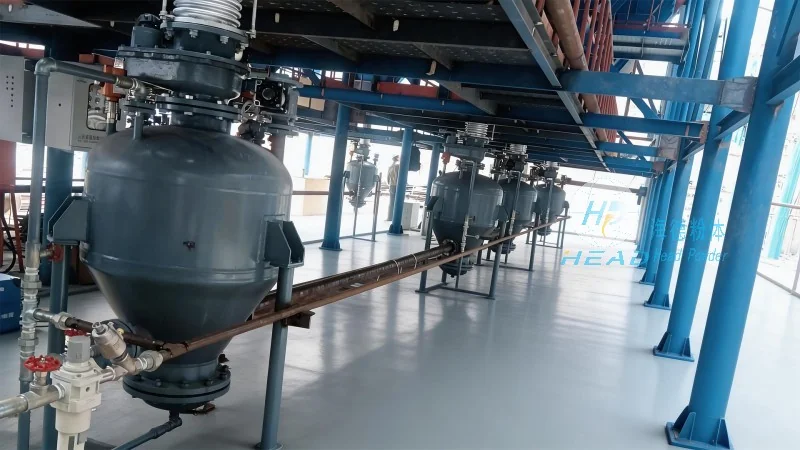
Working Scene Characteristics and Application Scenarios
The working scene characteristics of HeadPowder's conveyors are tailored to meet the diverse needs of industrial environments. These systems are designed for high efficiency, low maintenance, and adaptability to different material types and processing conditions. In food processing facilities, for example, the conveyors are constructed from food-grade materials and are equipped with sanitary designs to comply with hygiene standards. In pharmaceutical applications, the systems are sealed and sterilized to prevent contamination, ensuring product quality and safety. The conveyors are also suitable for handling abrasive materials, as the components are made from wear-resistant materials to extend the lifespan of the equipment.
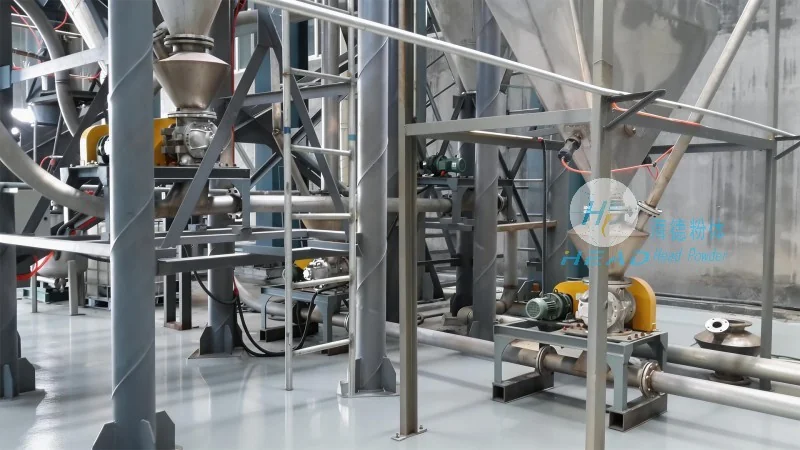
Key Features and Advantages in Real-World Applications
HeadPowder's bulk material conveyors offer several advantages that make them ideal for various industrial applications. The systems are capable of handling large volumes of material with minimal energy consumption, reducing operational costs. The design allows for easy integration into existing production lines, minimizing downtime during installation. Additionally, the conveyors are equipped with monitoring systems that provide real-time data on material flow and system performance, enabling proactive maintenance and troubleshooting. The company's commitment to quality ensures that each conveyor is manufactured to meet international standards, providing customers with reliable and long-lasting equipment.