

Principle and Working Scene Characteristics of Sugar Powder Conveying Systems
Sugar processing industries rely heavily on efficient and reliable equipment to handle bulk sugar powders. The sugar powder conveying system, specifically designed for transporting granular or powdered sugar, plays a pivotal role in ensuring smooth production workflows. This article delves into the fundamental principles of such systems and highlights key working scene characteristics that make them indispensable in modern sugar processing operations. From raw material handling to refined product distribution, these systems are integral to maintaining productivity and product quality in sugar processing facilities.
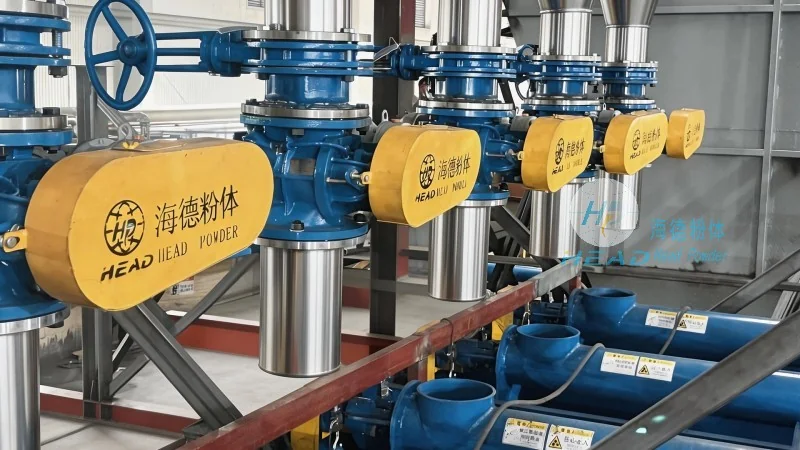
The Fundamental Principle of Sugar Powder Conveying Systems
At the heart of sugar powder conveying systems lies a mechanism that efficiently moves sugar powders from one location to another without compromising product quality or integrity. These systems typically operate on the principle of pneumatic or mechanical transport, leveraging air pressure or mechanical force to move the sugar particles. The design incorporates components such as hoppers, ducts, and control valves that work in tandem to regulate the flow and direction of the sugar powder. By understanding the underlying physics and engineering behind these systems, manufacturers can optimize performance, reduce downtime, and enhance overall operational efficiency. For instance, pneumatic conveying systems use compressed air to create a pressure differential that propels the sugar powder through the ductwork, while mechanical systems rely on screws, belts, or buckets to transport the material. Each method has its advantages and is chosen based on factors like material properties, distance, and required flow rate.
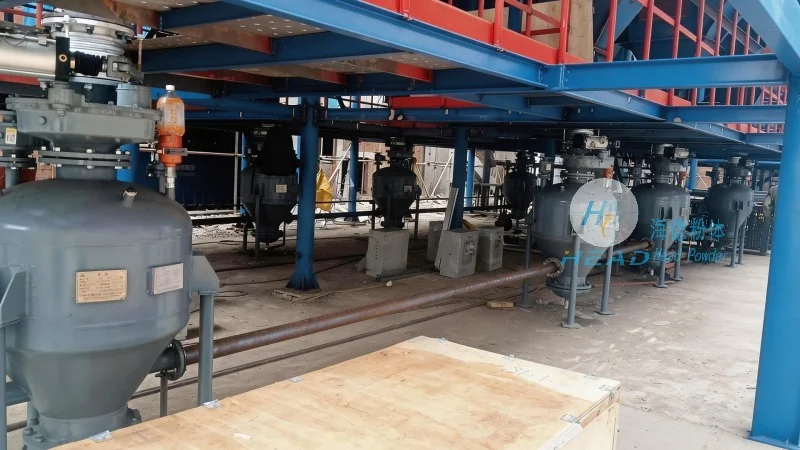
Key Working Scene Characteristics of Sugar Powder Conveying Systems
The effectiveness of sugar powder conveying systems is often determined by their adaptability to diverse working environments. Several key characteristics define their performance in real-world applications:
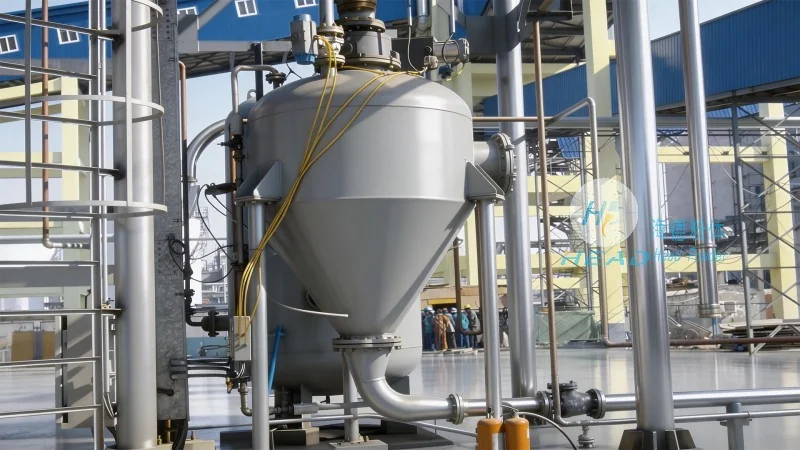
- High Capacity and Continuous Operation: These systems are engineered to handle large volumes of sugar powder, supporting continuous production lines without interruptions. The robust design ensures consistent flow rates, which is crucial for maintaining production schedules in sugar processing plants. For example, in a large-scale sugar mill, a conveying system may need to transport several tons of sugar per hour, and the system must maintain this throughput without any lag or blockage. This high capacity is achieved through optimized duct sizes, appropriate air pressure, and efficient material feeding mechanisms.
- Low Energy Consumption and Environmental Friendliness: Modern sugar powder conveying systems are designed with energy efficiency in mind. By minimizing air pressure requirements and optimizing material handling, they reduce operational costs while adhering to environmental regulations. This characteristic makes them suitable for long-term, sustainable operations in the sugar industry. The use of energy-efficient motors and advanced control systems further reduces the overall energy consumption. Additionally, the systems are designed to minimize dust emissions, contributing to a cleaner working environment and compliance with environmental standards.
- Easy Maintenance and Durability: Constructed from high-quality materials resistant to corrosion and wear, these systems require minimal maintenance. The modular design allows for easy replacement of components, reducing downtime and maintenance costs. This durability is essential for industries where equipment reliability directly impacts production output. For instance, the hopper and ducts are often made from stainless steel or corrosion-resistant alloys to withstand the acidic or humid conditions in sugar processing environments. The control valves and other moving parts are designed with wear-resistant materials to extend their service life.
- Customization for Specific Sugar Types: Different types of sugar, such as white sugar, brown sugar, or powdered sugar, may have varying particle sizes and moisture content. Sugar powder conveying systems can be customized to accommodate these variations, ensuring optimal performance for each specific application. This adaptability is a critical factor in meeting the diverse needs of sugar processing facilities. For example, a system designed for transporting fine powdered sugar may use smaller ducts and lower air pressure compared to a system handling coarse granular sugar. The ability to adjust parameters like air flow rate and material feed speed allows for precise control over the conveying process.
Application Scenarios in Sugar Processing Industries
Sugar powder conveying systems find widespread application across various stages of sugar production and processing. Some common working scenarios include:
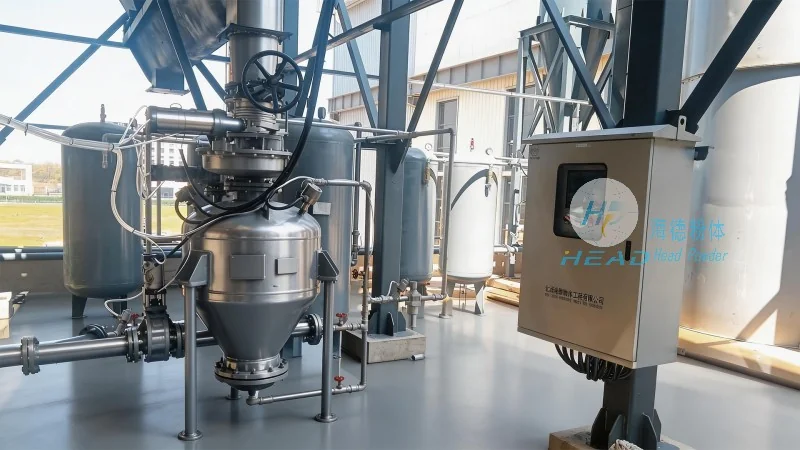
- Raw Sugar Handling and Transportation: In sugar mills, these systems are used to transport raw sugar from storage silos to processing units. The ability to handle bulk quantities efficiently ensures a steady supply of raw material for refining processes. The raw sugar, often in large bulk bags or silos, is fed into the conveying system, which then transports it to the refining equipment. This seamless transfer minimizes material handling time and reduces the risk of contamination.
- Refined Sugar Conveying: After refining, sugar is often in a powdered or granular form. The conveying systems transport refined sugar to packaging lines or storage areas, maintaining product purity and preventing contamination. The refined sugar, which is typically more delicate and prone to clumping, requires a gentle handling approach. The conveying system may use a low-pressure pneumatic design or a mechanical screw conveyor to prevent damage to the sugar particles. This ensures that the final product meets quality standards and is free from any mechanical damage.
- Industrial Sugar Processing: In industrial applications, such as the production of sugar-based products or food additives, these systems are used to move sugar powders between different processing stages. This ensures smooth integration of sugar into complex production workflows. For instance, in the production of sugar syrups or confectionery products, the sugar powder is conveyed to mixing tanks or reactors. The system must maintain a consistent flow rate to ensure uniform mixing and prevent overloading the processing equipment.
- Storage and Distribution: Sugar powder conveying systems are also employed in storage facilities to move sugar from bulk storage tanks to distribution points. This facilitates efficient inventory management and reduces the risk of product spoilage. The storage tanks are often large and located in remote areas, and the conveying system provides a reliable method to transport the sugar to packaging or shipping areas. This reduces the need for manual handling and minimizes the risk of accidents or spills.
About Shandong HeadPowder Engineering Co., Ltd.
As a leading manufacturer in the field of powder handling equipment, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and supplying high-quality sugar powder conveying systems. With years of experience and a commitment to innovation, the company has established itself as a trusted partner for sugar processing industries worldwide. HeadPowder's products are engineered to meet the unique demands of the sugar industry, ensuring reliability, efficiency, and durability. The company's headquarters is located in Shandong, China, where it continues to develop cutting-edge solutions for bulk material handling. By leveraging advanced engineering techniques and customer feedback, HeadPowder ensures that its conveying systems are tailored to the specific needs of each client. The company's team of experts provides comprehensive support, from initial design and installation to ongoing maintenance and troubleshooting. This commitment to customer satisfaction has made HeadPowder a preferred choice for sugar processing facilities seeking reliable and efficient equipment.