

Principle and Working Characteristics of Dust-Free Automatic Powder Conveying Machines
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced dust-free automatic powder conveying equipment. This article explores the fundamental principles behind these systems and highlights their key working characteristics and typical application scenarios.
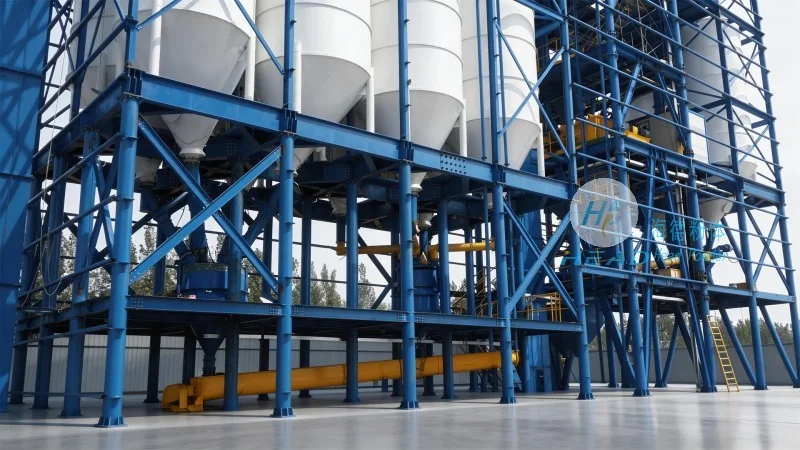
Core Principles of Dust-Free Powder Conveying
The dust-free automatic powder conveying machine operates on several core principles to ensure efficient and safe material transport. The primary goal is to maintain a controlled environment that prevents dust contamination and ensures product purity. Key components include sealed conveying lines, positive pressure or vacuum systems, and advanced filtration mechanisms. These elements work in tandem to move powders from the source to the destination without exposing the material to the external environment.
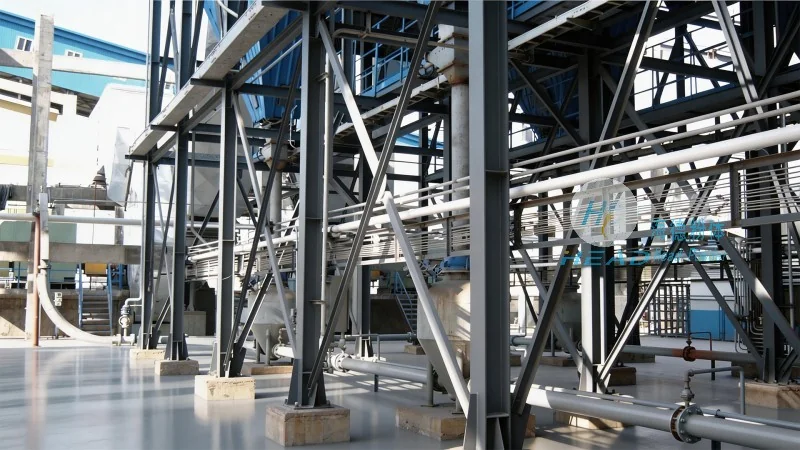
Key Working Characteristics
One of the most significant characteristics of these systems is their ability to handle a wide range of powder types, from fine powders to bulk materials. The equipment is designed with adjustable speed and pressure controls, allowing operators to optimize the conveying process for different material properties. Additionally, the sealed design minimizes dust emissions, making it suitable for applications where air quality and product integrity are critical. The systems also feature easy maintenance and cleaning protocols, ensuring consistent performance over time.
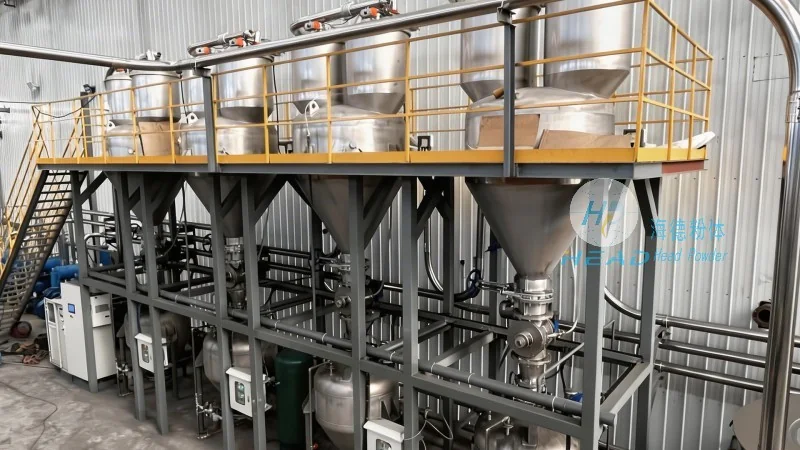
Typical Working Scenarios and Applications
Dust-free automatic powder conveying machines are widely used in various industries where powder handling is essential. In the pharmaceutical industry, for example, these systems are crucial for transporting active ingredients and excipients while maintaining sterile conditions. The food and beverage sector also relies on such equipment to handle ingredients like flour, sugar, and spices without contamination. In the chemical industry, they are used for transporting raw materials and finished products, ensuring safety and compliance with regulatory standards. Furthermore, in the manufacturing of cosmetics and personal care products, the systems help maintain product quality and prevent cross-contamination.
Advantages of Using Dust-Free Conveying Systems
Implementing dust-free automatic powder conveying systems offers several advantages for businesses. Firstly, they enhance product quality by preventing dust and contamination, which is vital in industries where product purity is non-negotiable. Secondly, they improve workplace safety by reducing the risk of dust explosions and respiratory issues. Thirdly, the sealed design helps maintain a clean environment, which is beneficial for both operational efficiency and regulatory compliance. Lastly, these systems are often more energy-efficient and cost-effective in the long run due to their durability and low maintenance requirements.
Conclusion
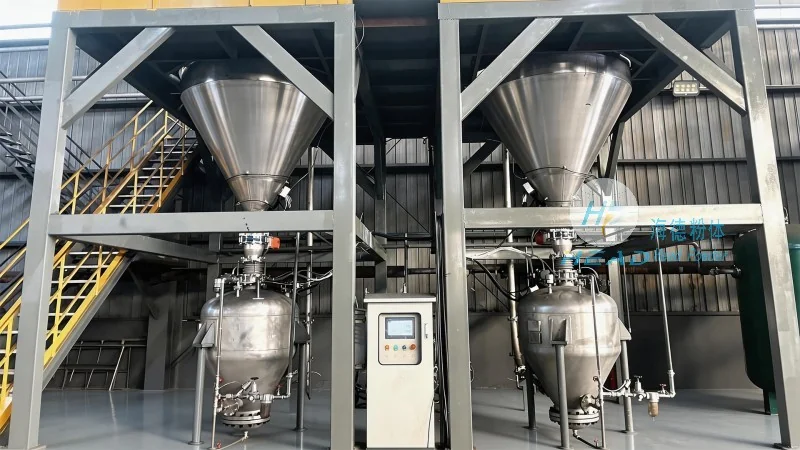
HeadPowder's dust-free automatic powder conveying machines represent a sophisticated solution for efficient and safe powder handling. By understanding the core principles and working characteristics of these systems, businesses can make informed decisions about integrating them into their operations. With a strong presence in Shandong, China, HeadPowder continues to innovate and provide high-quality equipment that meets the evolving needs of various industries.