

Principles and Working Scene Characteristics of Intelligent Powder Conveying Lines
HeadPowder, a leading enterprise in the powder conveying industry, specializes in the research, development, and manufacturing of intelligent powder conveying systems. With a strong technical background and years of practical experience, the company has become a trusted partner for many clients in various industries. This article will explore the principles and working characteristics of intelligent powder conveying lines, focusing on their core technology and typical application scenarios.
Principles of Intelligent Powder Conveying Lines
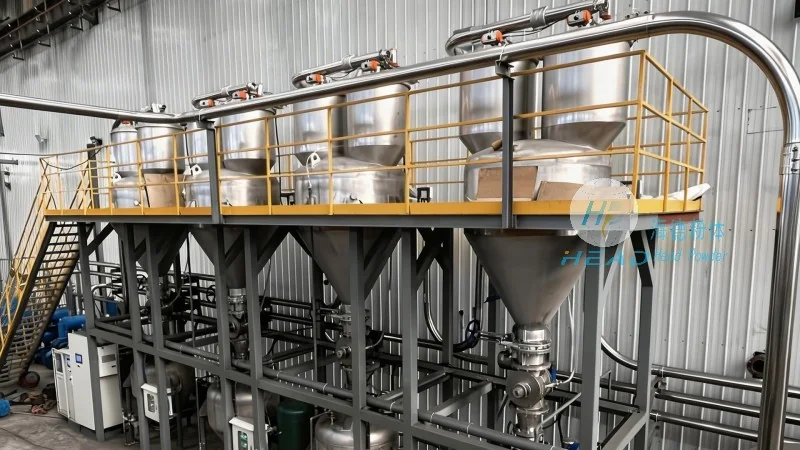
The intelligent powder conveying line is a highly automated system designed to transport bulk powders efficiently and safely. The core principle involves the use of advanced control technology and optimized mechanical components to ensure stable and reliable material flow. Key components include the feeding unit, conveying pipeline, control system, and monitoring devices. The feeding unit, often equipped with a rotary valve or screw feeder, ensures a consistent and controlled input of powder. The conveying pipeline, typically made of stainless steel or other corrosion-resistant materials, is designed to handle different types of powders without degradation. The control system, integrated with sensors and automation software, monitors parameters such as pressure, flow rate, and temperature in real-time. This allows for immediate adjustments to maintain optimal conveying conditions, preventing issues like blockages or material degradation. The monitoring devices provide visual and data feedback, enabling operators to track the system's performance and identify potential problems early. By combining these elements, the intelligent powder conveying line achieves high efficiency, low maintenance, and consistent material quality.
Working Scene Characteristics of Intelligent Powder Conveying Lines
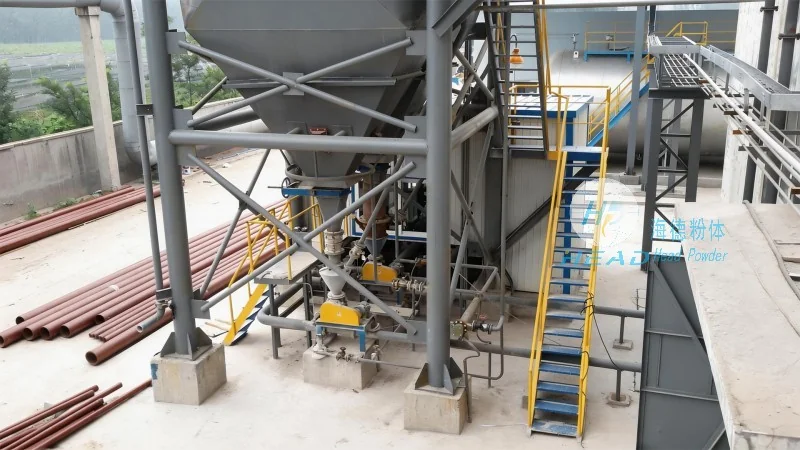
The application scenarios of intelligent powder conveying lines are diverse, catering to various industrial needs. In the pharmaceutical industry, for example, these systems are used to transport active pharmaceutical ingredients (APIs) and excipients with high precision and cleanliness. The strict hygiene requirements are met through stainless steel construction and sealed components, ensuring product purity. In the chemical industry, the systems handle a wide range of powders, from fine chemicals to bulk raw materials. The ability to handle different particle sizes and moisture content makes them suitable for processes like mixing, blending, and packaging. The food industry also benefits from these systems, as they are designed to maintain food safety standards. The gentle handling of powders prevents contamination and preserves product quality. In the mining and cement industries, the systems are used for bulk material transport, such as ore and cement. The high capacity and durability of the conveying lines make them ideal for heavy-duty applications. Additionally, in the chemical and petrochemical sectors, the systems are used for transporting reactive powders and chemicals, with safety features like explosion-proof designs to prevent accidents. Each application scenario is tailored to the specific requirements of the industry, ensuring that the intelligent powder conveying line meets the needs of the user while maintaining efficiency and reliability.
Key Features and Benefits
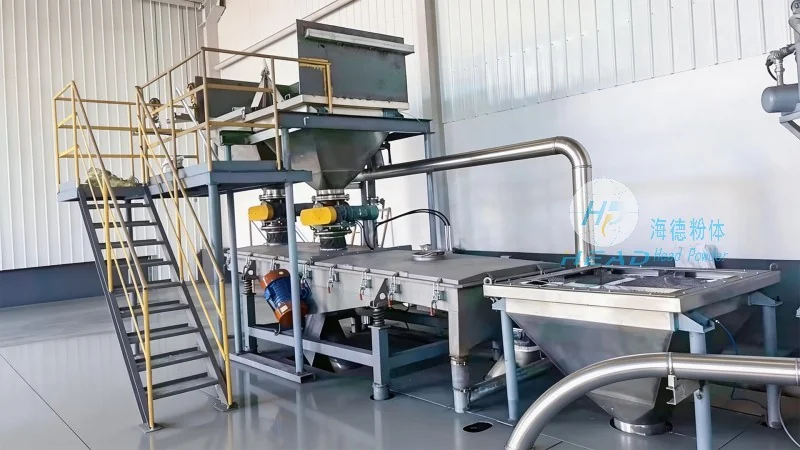
Intelligent powder conveying lines from Shandong HeadPowder Engineering Co., Ltd. offer several key features that set them apart from traditional conveying systems. One of the main advantages is the integration of advanced control technology, which allows for real-time monitoring and adjustment of conveying parameters. This results in improved process control and reduced downtime. The systems are also designed for easy maintenance, with modular components that can be replaced quickly without disrupting the entire operation. This reduces maintenance costs and increases system availability. Another important feature is the ability to handle a wide range of powder types, from fine powders to bulk materials. The adjustable speed and pressure settings ensure that different materials are conveyed efficiently without damage. The stainless steel construction provides durability and resistance to corrosion, making the systems suitable for harsh environments. Additionally, the systems are equipped with safety features such as overload protection and emergency stop buttons, ensuring safe operation. The monitoring devices provide detailed data on system performance, enabling operators to optimize the conveying process and improve overall efficiency. These features collectively contribute to the high performance and reliability of the intelligent powder conveying lines, making them a preferred choice for many industries.
Conclusion
Intelligent powder conveying lines from Shandong HeadPowder Engineering Co., Ltd. represent a significant advancement in bulk material handling technology. By combining advanced control systems, durable construction, and efficient design, these systems offer superior performance and reliability compared to traditional methods. The diverse application scenarios and key features make them suitable for various industries, including pharmaceuticals, chemicals, food, mining, and cement. As the demand for efficient and safe powder conveying increases, the intelligent powder conveying lines from HeadPowder continue to provide innovative solutions that meet the evolving needs of the market. With a strong commitment to quality and customer satisfaction, the company remains at the forefront of the powder conveying industry, delivering high-performance systems that enhance productivity and ensure product quality.