

What is a Purified Ash Material Conveying Line? What are its Design Principles?
For industrial facilities dealing with ash and other particulate materials, the efficient and safe transportation of these materials is crucial. A purified ash material conveying line, also known as a dust-free ash handling system, is a specialized system engineered to transport ash and similar materials from sources like boilers or incinerators to disposal or processing locations. This system is designed with stringent measures to minimize dust emissions and ensure environmental compliance, making it an essential component in modern waste management and industrial operations.
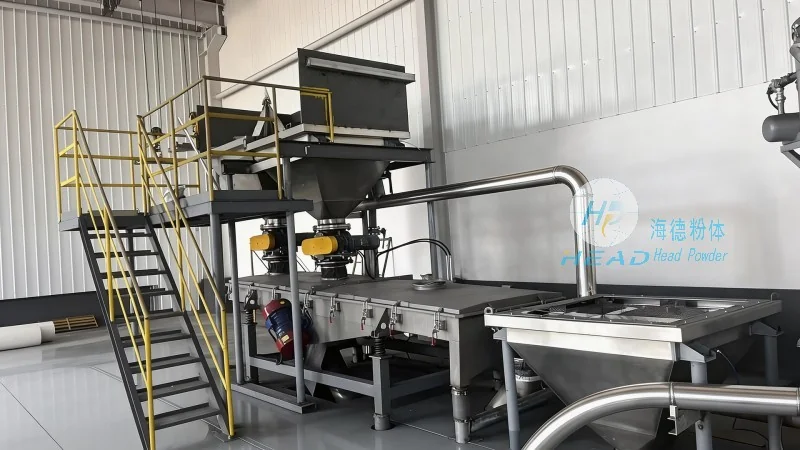
Key Components and Design Principles of the Conveying Line
The design of a purified ash material conveying line is built upon several core principles to ensure optimal performance, safety, and environmental protection. The primary components typically include ash feeders, conveyor belts or screw conveyors, dust collection systems, and control mechanisms. Each component is carefully selected and integrated to maintain a dust-free environment throughout the conveying process.
One of the fundamental design principles is the use of enclosed or sealed systems to prevent dust from escaping into the ambient air. This is achieved through features such as airtight feed hoppers, sealed conveyor sections, and integrated dust collection units. The system often employs negative pressure or positive pressure control to manage air flow and prevent dust leakage. Additionally, the materials used in the construction of the conveying line, including the conveyor belts and housing, are chosen for their resistance to abrasion and chemical corrosion, ensuring durability in harsh industrial environments.
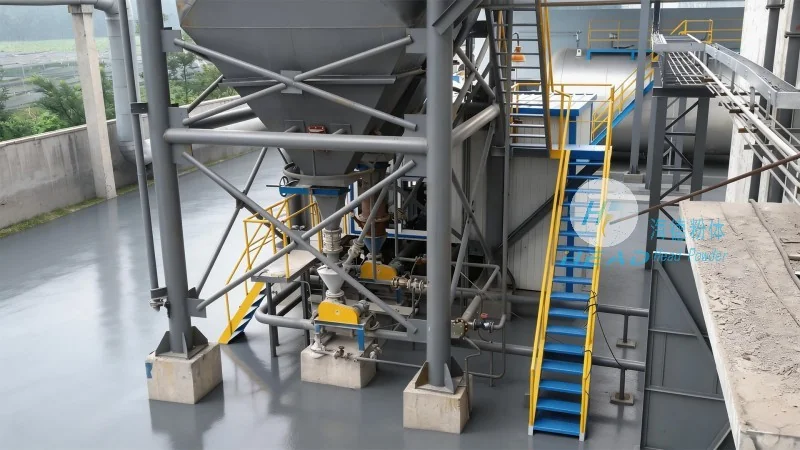
How the Conveying Line Works: A Step-by-Step Process
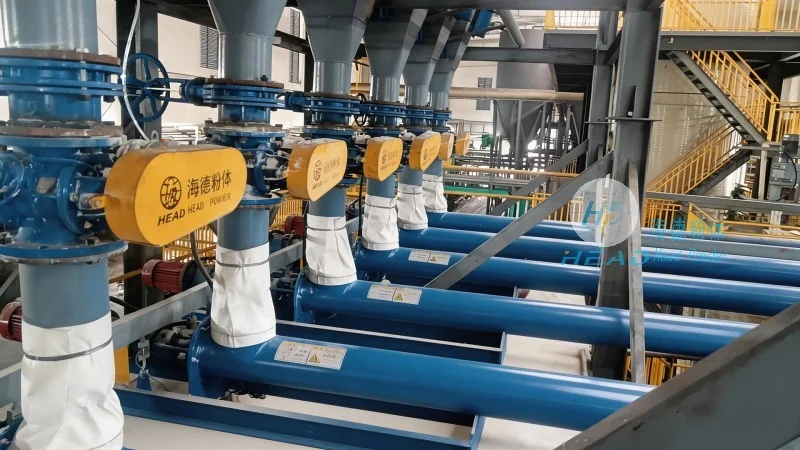
The operation of a purified ash material conveying line involves a systematic process that ensures the efficient and safe movement of ash from its source to the destination. The process typically begins with the ash being discharged from a boiler or storage silo into a feed hopper. The feed hopper is equipped with a feeder mechanism, such as a rotary valve or a screw feeder, which controls the flow rate of the ash into the conveyor system.
From the feed hopper, the ash is transferred to the conveyor section. This section may consist of a belt conveyor, a screw conveyor, or a pneumatic conveying system, depending on the specific requirements of the application. The conveyor transports the ash through the system, maintaining a consistent flow rate to prevent blockages or overloading. Along the conveyor path, dust collection units are strategically placed to capture any airborne particles, ensuring that the system remains dust-free.
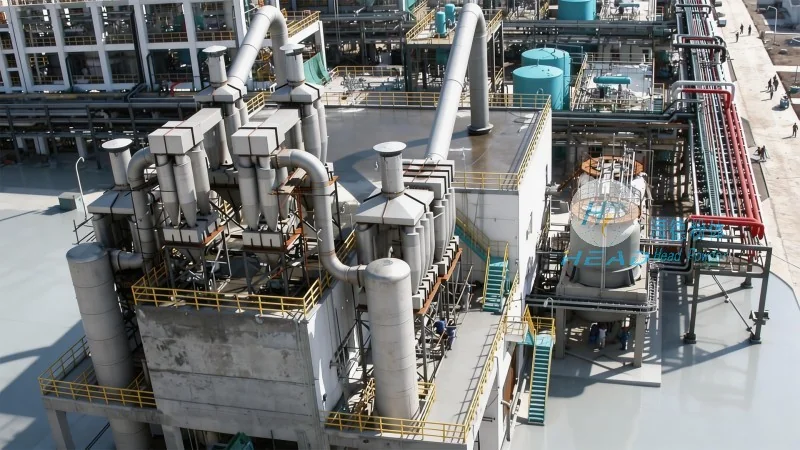
The conveying line terminates at the discharge point, where the ash is deposited into a disposal container or a processing unit. The entire system is monitored and controlled by a central control panel, which allows operators to adjust the flow rate, monitor system performance, and ensure compliance with environmental regulations.
Benefits of Using a Purified Ash Material Conveying Line
Implementing a purified ash material conveying line offers numerous benefits for industrial facilities. Firstly, it significantly reduces dust emissions, contributing to a cleaner working environment and compliance with environmental regulations. This is achieved through the enclosed and sealed design, which prevents dust from escaping into the air. Secondly, the system enhances operational efficiency by providing a continuous and reliable method of transporting ash, reducing downtime and labor costs associated with manual handling.
Thirdly, the use of durable materials and robust design ensures long-term reliability and low maintenance costs. The system is designed to withstand the harsh conditions of industrial environments, including high temperatures and abrasive materials, reducing the need for frequent repairs or replacements. Additionally, the automated control systems allow for precise monitoring and adjustment, improving overall operational performance and reducing human error.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of industrial conveying systems, including purified ash material conveying lines. With a strong commitment to quality and innovation, HeadPowder specializes in designing and manufacturing customized solutions tailored to the specific needs of its clients. The company's products are engineered to meet the highest standards of performance, safety, and environmental compliance, ensuring that clients receive reliable and efficient solutions for their ash handling requirements.
HeadPowder's team of experienced engineers and technicians work closely with clients to understand their unique challenges and develop tailored solutions. The company's state-of-the-art manufacturing facilities and rigorous quality control processes ensure that each product meets the highest standards of performance and durability. With a focus on customer satisfaction and long-term partnerships, HeadPowder has established itself as a trusted provider of industrial conveying systems in the global market.