

Principle and Working Scene Characteristics of Feather Pneumatic Conveying Equipment
Feather pneumatic conveying equipment is a specialized system designed for the efficient transportation of lightweight materials such as feathers, fine powders, and other low-density particulates. This technology leverages compressed air to move materials through a sealed pipeline system, offering advantages in terms of hygiene, dust control, and flexibility compared to traditional mechanical conveying methods. The equipment is widely used in industries where material handling requires precision and minimal contamination, making it a critical component in modern processing facilities.
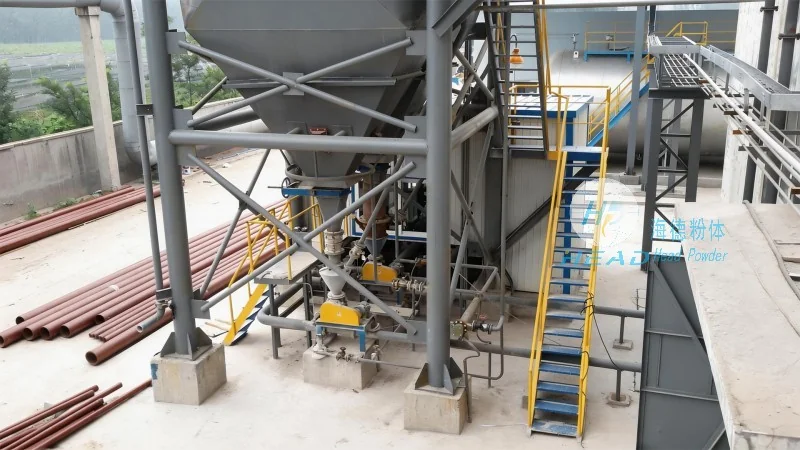
Core Principles of Pneumatic Conveying
The fundamental principle of pneumatic conveying involves the use of air as the conveying medium. In a typical system, a blower or compressor generates high-pressure air, which is then introduced into a hopper or feed point containing the material. As the air flows through the pipeline, it entrains the material particles, creating a mixture known as a "slurry" or "conveyed stream." The velocity of the air is carefully controlled to ensure that the material is fully suspended and transported without clogging or degradation. The system typically includes components such as a hopper, feeder, pipeline, and receiver, each playing a crucial role in the overall operation. The choice of conveying type—whether dense-phase or dilute-phase—depends on the material characteristics and the required distance or pressure drop.

Working Scene Characteristics and Applications
Feather pneumatic conveying equipment is particularly suited for applications where the material is delicate, hygienic requirements are stringent, or space constraints exist. For instance, in the poultry processing industry, this equipment is used to transport feathers from plucking stations to processing or storage areas, ensuring that the material remains clean and free from contamination. The system's ability to operate in a closed environment minimizes dust exposure and odor issues, which is essential for maintaining a safe and compliant workplace. Additionally, the flexibility of the pipeline layout allows for easy integration into existing production lines, adapting to changes in workflow or facility expansion. Industries such as food processing, pharmaceuticals, and cosmetics also benefit from this technology, as it provides a hygienic and efficient method for handling fine powders and granules.
Key Features and Advantages
One of the primary advantages of feather pneumatic conveying equipment is its ability to handle low-density materials that are difficult to transport using traditional methods. The system's design minimizes material degradation, as the particles are not subjected to mechanical abrasion or excessive pressure. This is particularly important for feathers, which can be easily damaged if handled roughly. The equipment also offers high efficiency in terms of material throughput, with the ability to transport large volumes of material over significant distances with minimal energy consumption. Furthermore, the closed system design enhances safety by preventing dust emissions and cross-contamination, aligning with industry standards for occupational health and environmental protection. The system's modularity allows for easy maintenance and repair, reducing downtime and operational costs.
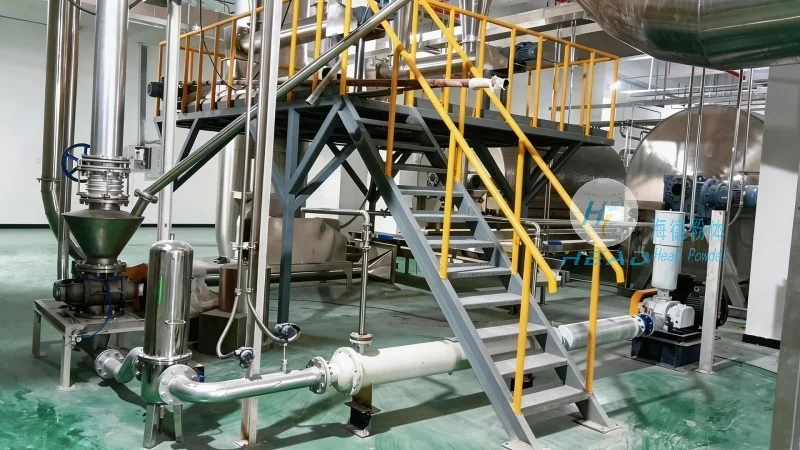
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer specializing in the design, development, and supply of pneumatic conveying systems. With a focus on innovation and customer-centric solutions, the company has established itself as a trusted partner in the material handling industry. HeadPowder's expertise lies in tailoring equipment to meet the specific needs of clients, ensuring that each system is optimized for the material being conveyed, the operational environment, and the production requirements. The company's facilities are located in Shandong, China, where it leverages advanced manufacturing capabilities and a skilled workforce to deliver high-quality products. HeadPowder's commitment to quality and reliability has earned it a reputation for excellence in the market, with clients ranging from small-scale processors to large industrial facilities.