

Working Principle and Features of Dense Phase Powder Handling Equipment
Understanding the working principle and features of dense phase powder handling equipment is crucial for industries that rely on efficient and reliable material transport. This equipment is designed to handle bulk powders in a dense, slurry-like state, offering significant advantages over traditional pneumatic or mechanical conveying methods. The technology is particularly beneficial for transporting fine, abrasive, or moisture-sensitive powders, where traditional methods may cause degradation or clogging.
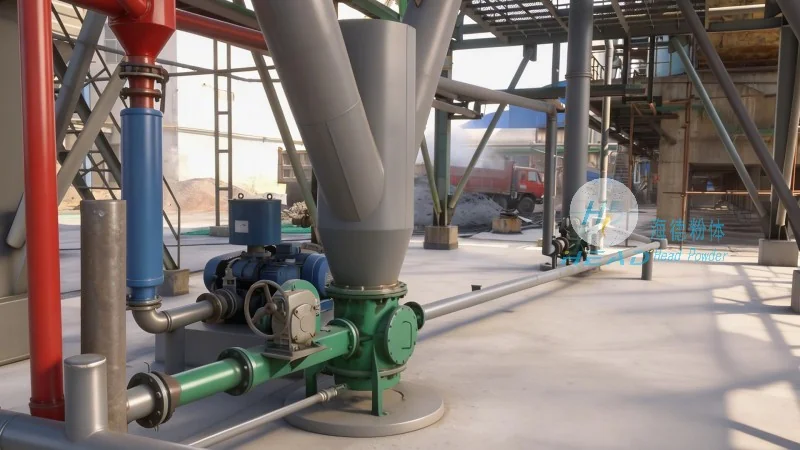
Working Principle of Dense Phase Powder Handling Equipment
Dense phase powder handling equipment operates by creating a high-pressure environment that forces the powder to move through a pipeline. The process typically involves a positive displacement pump or a high-pressure compressor that injects air or gas into the powder stream, forming a dense, non-eroding mixture. This mixture travels at a lower velocity compared to pneumatic conveying, which reduces wear on the pipeline and minimizes product degradation. The equipment ensures that the powder is transported in a continuous, stable flow, preventing clogging and ensuring consistent delivery to the destination. The pump or compressor maintains a constant pressure, which allows for precise control over the flow rate and solids concentration, enabling operators to adjust the system according to specific application requirements.
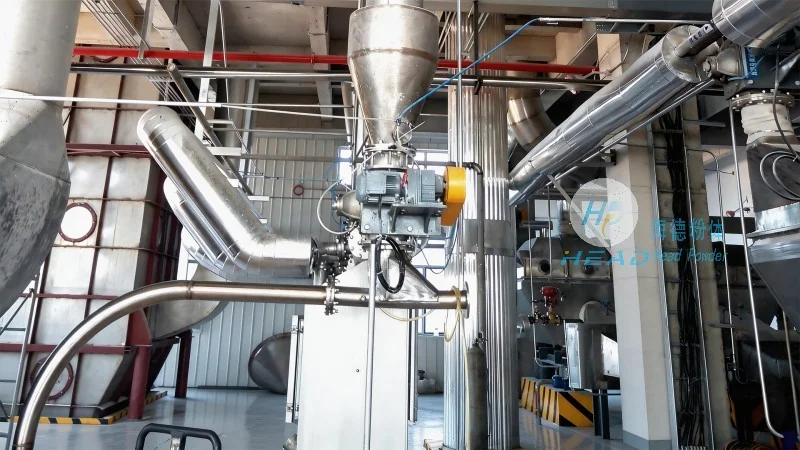
Key Features of Dense Phase Powder Handling Equipment
One of the primary features of dense phase powder handling equipment is its ability to handle a wide range of powder types, including fine, abrasive, and moisture-sensitive materials. The equipment is designed to maintain a high solids concentration, typically ranging from 30% to 70% by weight, which increases the conveying capacity and reduces the need for additional equipment. Another key feature is the low pressure drop across the system, which minimizes energy consumption and operational costs. For example, dense phase conveying systems can transport materials over long distances with minimal pressure loss, making them suitable for applications where traditional methods would require multiple pumps or compressors. Additionally, dense phase conveying systems are highly flexible, allowing for easy integration with existing production lines and the ability to transport materials in various orientations, such as vertical or horizontal pipelines. The equipment also includes features like pressure relief valves and flow meters to monitor and control the system, ensuring safe and efficient operation.
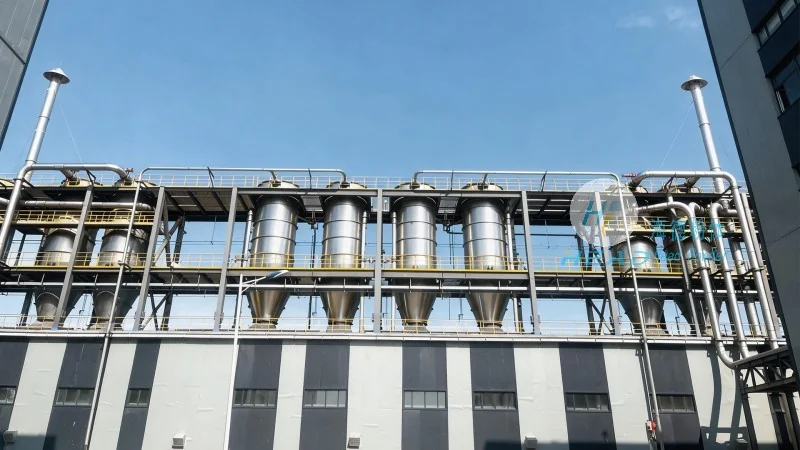
Advantages in Industrial Applications
Dense phase powder handling equipment offers several advantages in industrial applications. For example, in the chemical and pharmaceutical industries, it is used to transport sensitive powders without causing contamination or degradation. The dense phase process prevents the powder from becoming airborne, reducing the risk of dust explosions and ensuring product purity. In the food and beverage industry, the equipment ensures that powders are handled hygienically and efficiently, maintaining product quality and meeting regulatory standards. The equipment is also suitable for transporting materials in the mining and construction sectors, where large volumes of bulk materials need to be moved over long distances. The low maintenance requirements and long service life of dense phase systems make them a cost-effective solution for many industrial applications. Furthermore, the ability to transport materials in a continuous flow reduces production downtime and increases overall productivity, which is critical for businesses operating in competitive markets.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of dense phase powder handling equipment. With a focus on innovation and quality, the company has developed advanced solutions that meet the diverse needs of various industries. HeadPowder's products are designed to provide reliable and efficient material transport, ensuring that customers can achieve their production goals with minimal downtime and operational costs. The company's commitment to customer satisfaction and technical excellence has made it a trusted partner for businesses worldwide. HeadPowder's team of engineers and technicians works closely with clients to understand their specific requirements and provide customized solutions that optimize material handling processes. The company's manufacturing facilities are equipped with state-of-the-art technology and adhere to international quality standards, ensuring that each product meets the highest performance and safety requirements. HeadPowder's dedication to research and development has led to the introduction of new features and improvements in existing equipment, such as energy-efficient pumps and advanced control systems, which further enhance the performance and reliability of dense phase powder handling systems.