

Working Principle and Features of Malt Powder Conveying Systems
Understanding the core components and operational mechanisms of malt powder conveying systems is essential for optimizing industrial processes in the food and beverage sector. These systems are designed to handle the unique challenges posed by malt powder, ensuring efficient and reliable material transport while maintaining product integrity.
Working Principle of Malt Powder Conveying Systems
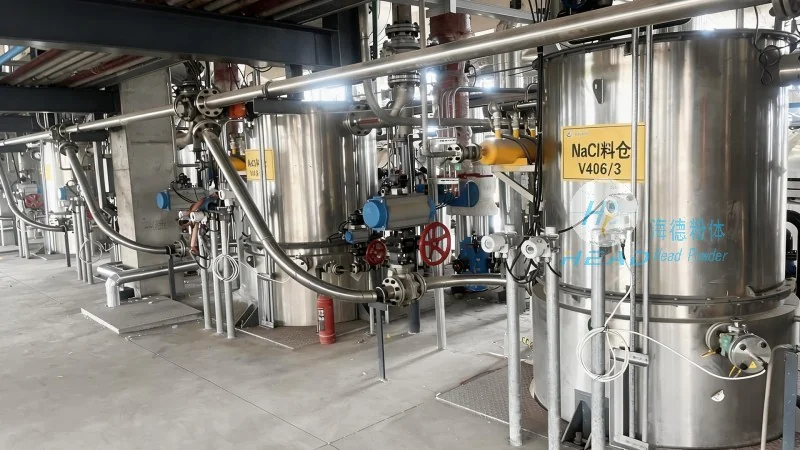
The working principle of a typical malt powder conveying system involves several key stages. Initially, the malt powder is fed into the system, often through a hopper or a loading mechanism. From there, the material is drawn into a conveying device, such as a pneumatic or mechanical conveyor. The system utilizes controlled airflow or mechanical action to move the powder through the pipeline, ensuring minimal segregation and loss. The design incorporates features like airlocks and rotary valves to prevent backflow and maintain a consistent flow rate. The entire process is regulated by a control panel that monitors pressure, flow rate, and other critical parameters, allowing for real-time adjustments to optimize performance.
Key Features of Malt Powder Conveying Systems
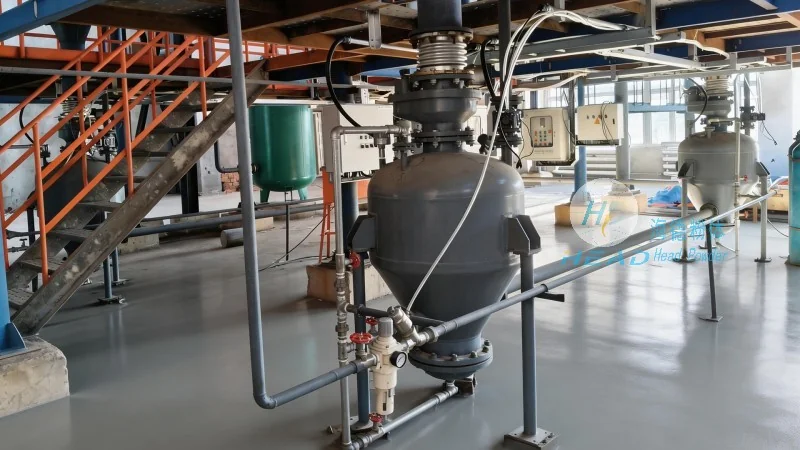
HeadPowder Engineering Co., Ltd. specializes in the design and manufacturing of advanced malt powder conveying systems, offering several distinctive features that enhance operational efficiency and product quality. One of the primary features is the use of stainless steel construction, which ensures durability and resistance to corrosion, critical for handling malt powder in food processing environments. The systems are equipped with high-efficiency filters and dust collection mechanisms to maintain a clean and safe working environment, complying with industry standards for hygiene and safety. Additionally, the conveyors are designed with adjustable speed controls, allowing operators to fine-tune the flow rate based on specific production requirements. The integration of automated monitoring systems provides real-time data on system performance, enabling proactive maintenance and reducing downtime. Another notable feature is the compact design, which minimizes space requirements while maximizing conveying capacity, making it suitable for both small-scale and large-scale production facilities.
Benefits of Using Advanced Malt Powder Conveying Systems
Implementing a well-designed malt powder conveying system from HeadPowder Engineering Co., Ltd. offers numerous benefits for industrial operations. Firstly, the system significantly improves material handling efficiency, reducing the time and labor required for transporting malt powder from storage to processing areas. This leads to increased production throughput and reduced operational costs. Secondly, the advanced filtration and dust control features help maintain product purity, preventing contamination and ensuring consistent quality of the malt powder. This is particularly important in the food and beverage industry, where product safety and regulatory compliance are paramount. Thirdly, the automated monitoring and control systems enhance operational reliability, minimizing the risk of system failures and downtime. By providing real-time data and alerts, these systems enable quick troubleshooting and maintenance, further improving overall system uptime. Lastly, the durable construction and low maintenance requirements contribute to long-term cost savings, as the systems are built to withstand the rigors of continuous operation in industrial settings.
Application Scenarios and Customization Options
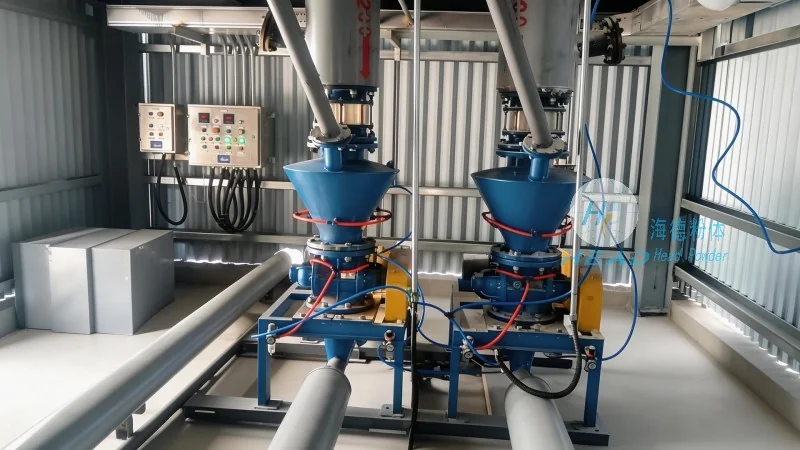
Malt powder conveying systems from HeadPowder Engineering Co., Ltd. are versatile and can be customized to meet the specific needs of various applications. They are commonly used in breweries, malting facilities, and food processing plants where malt powder needs to be transported between different stages of production. The systems can be adapted for different powder types, including different varieties of malt and other similar granular materials. Customization options include adjustable conveying capacities, different pipeline configurations, and integration with existing production lines. The company also offers technical support and consultation services to help clients select the most suitable system for their specific requirements, ensuring optimal performance and compliance with industry standards.