

What is a Pulse Jet Dust Collector with Powder Pneumatic Conveying Equipment? Understanding Its Desi
When considering industrial solutions for dust control and material handling, the integration of pulse jet dust collectors with powder pneumatic conveying systems represents a sophisticated approach to addressing these challenges. This article explores the components, operation, and design principles of such equipment, providing insights into its application in various industrial settings.
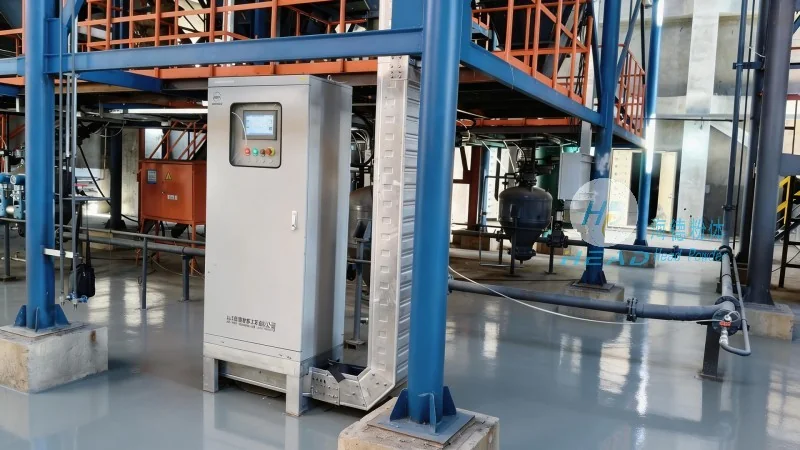
Introduction to Pulse Jet Dust Collectors and Powder Pneumatic Conveying Systems
A pulse jet dust collector is a type of air filtration system that uses compressed air pulses to clean filter media, ensuring continuous and efficient dust removal. When combined with a powder pneumatic conveying system, this technology offers a comprehensive solution for both dust collection and material transport. The synergy between these two systems enhances operational efficiency and environmental compliance in industrial processes.
The Core Components of a Pulse Jet Dust Collector
The pulse jet dust collector consists of several critical components that work in tandem to capture and clean airborne particles. The primary components include filter cartridges, which are designed to trap fine dust particles; a pulse valve system that delivers high-pressure air pulses to clean the filters; a hopper for collecting the collected dust; and a control panel that manages the cleaning cycles and system operation. The filter cartridges are typically made of materials like polyester or fiberglass, chosen for their high filtration efficiency and durability under industrial conditions.
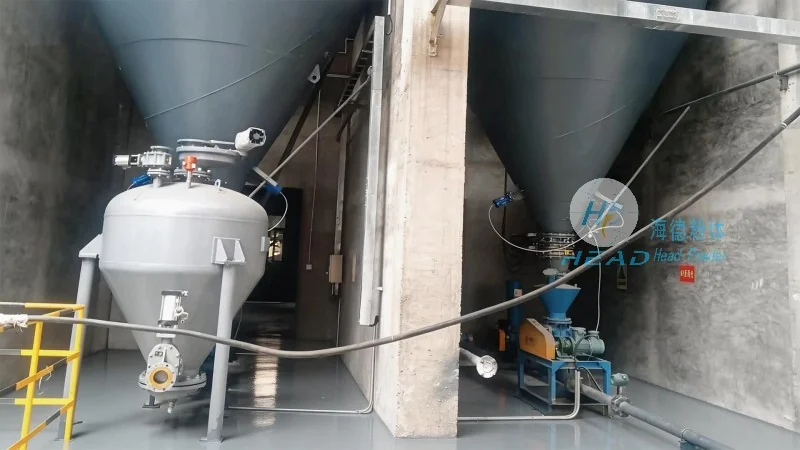
How Pneumatic Conveying Works in the System
Pneumatic conveying is the method by which dry powders and other bulk materials are transported through a system using air or other gases. In a pulse jet dust collector with pneumatic conveying, the system draws material from a hopper or storage bin and transports it to a processing unit or storage location. The conveying process can operate under positive or negative pressure, depending on the specific application requirements. The integration of pneumatic conveying with the dust collector allows for a seamless transition from dust collection to material transport, minimizing manual handling and reducing the risk of contamination.
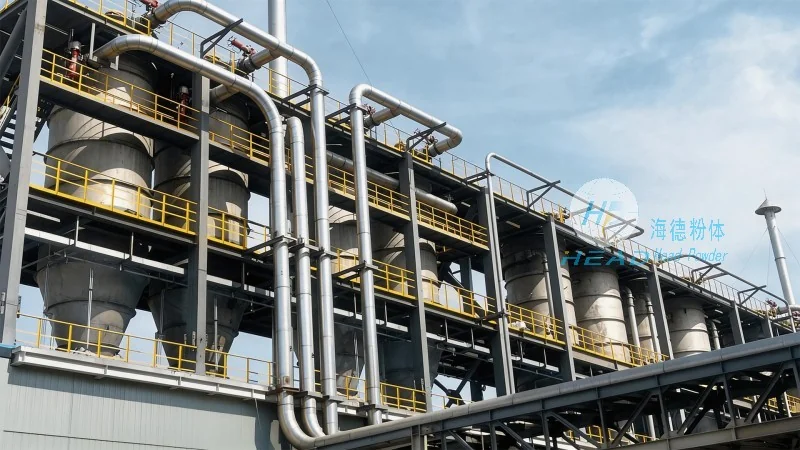
Design Principles for Efficient Operation
The design of a pulse jet dust collector with pneumatic conveying equipment follows several key principles to ensure optimal performance. These principles include selecting appropriate filter media based on the particle size and type, optimizing pulse pressure and frequency to minimize filter clogging and maximize cleaning effectiveness, and properly sizing the hopper and conveying lines to handle the material flow rates. Additionally, the system's control system is engineered to monitor pressure, temperature, and filter status, providing real-time feedback for maintenance and operational adjustments. This proactive monitoring helps maintain the system's efficiency and extends the lifespan of the components.
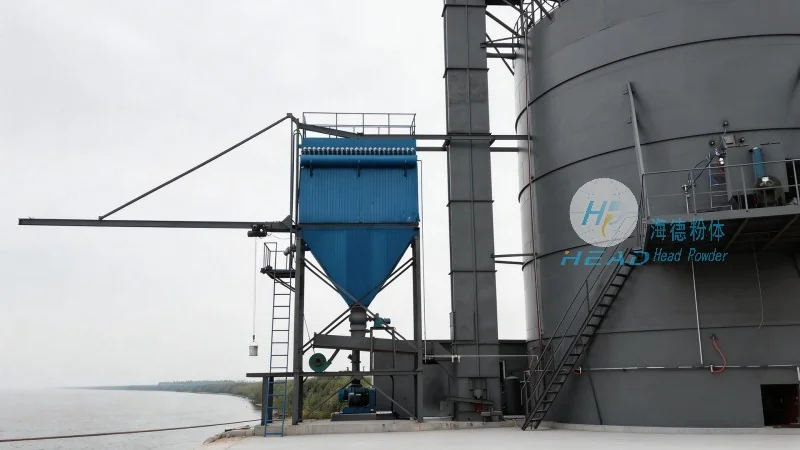
Applications and Benefits in Industrial Settings
The combination of pulse jet dust collection and pneumatic conveying is widely utilized in industries such as pharmaceuticals, food processing, chemical manufacturing, and metalworking. The benefits of this system include improved air quality, reduced labor costs due to automated operation, and increased material handling efficiency. By effectively capturing dust and transporting materials, these systems contribute to a safer and more productive work environment. For example, in pharmaceutical manufacturing, the system ensures that powders are handled without contamination, while in food processing, it maintains hygiene standards and prevents product spoilage.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. is a professional manufacturer specializing in the design, production, and installation of industrial dust collection and material handling equipment. With a strong commitment to quality and innovation, the company has established itself as a leader in the industry. HeadPowder Engineering provides customized solutions tailored to the specific needs of its clients, ensuring that each system is optimized for the unique requirements of the application. The company's products are known for their durability, efficiency, and compliance with international safety and environmental standards. By leveraging advanced technology and expert engineering, HeadPowder Engineering delivers reliable equipment that enhances operational performance and reduces environmental impact.