

What is an Aggregate Powder Conveying System Equipment? What Are Its Design Principles?
An aggregate powder conveying system equipment is a specialized industrial device engineered to transport bulk materials, particularly aggregates and powders, from one location to another. These systems are integral to numerous industries, including construction, mining, and manufacturing, where efficient material handling is critical for maintaining operational efficiency and productivity. The equipment is designed to handle a wide spectrum of materials, ranging from fine powders to coarse aggregates, ensuring smooth and reliable transport under various conditions. By integrating advanced technology and robust engineering, these systems enable businesses to streamline their material handling processes, reduce downtime, and enhance overall operational performance.
Key Components and Their Functions
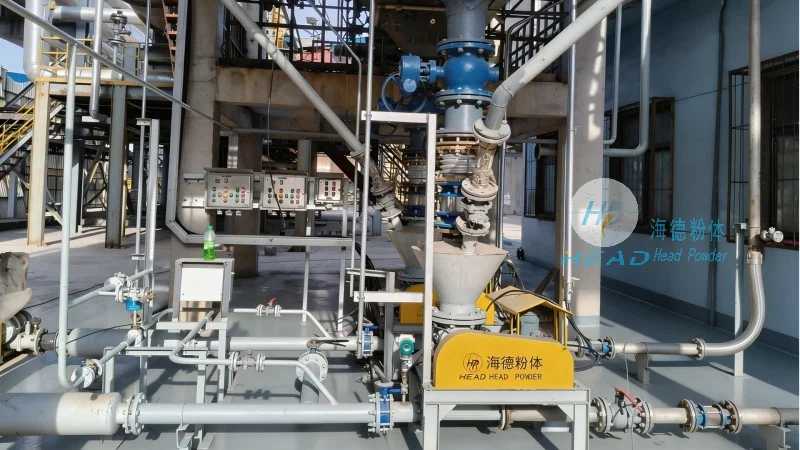
The aggregate powder conveying system equipment typically comprises several key components, each playing a crucial role in the overall operation. The primary components include hoppers, feeders, conveyors, and control systems. Hoppers are used to store and feed the material into the system, while feeders regulate the flow rate to prevent overloading and ensure consistent material delivery. Conveyors, such as belt conveyors or pneumatic conveyors, transport the material through the system, and control systems monitor and adjust the operation to maintain optimal performance. Additionally, accessories like dust collectors and safety sensors may be included to enhance system safety and efficiency. Each component is carefully designed and manufactured to withstand the demands of industrial environments, ensuring long-term reliability and minimal maintenance.
Design Principles of Aggregate Powder Conveying Systems
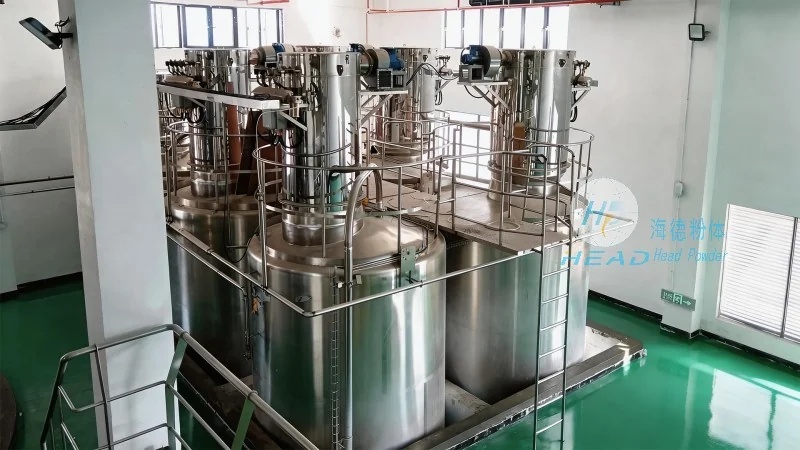
The design of an aggregate powder conveying system equipment is guided by several fundamental principles that prioritize efficiency, reliability, and durability. These principles include material flow optimization, energy efficiency, and system integration. Material flow optimization involves designing the system to minimize friction and resistance, ensuring smooth and consistent material movement. This is achieved through the use of inclined or horizontal conveyor designs, as well as adjustable feed mechanisms that regulate the material flow rate. Energy efficiency is a critical consideration, as industrial systems often operate continuously and consume significant energy. Designers focus on using low-friction components, such as high-quality belts or smooth conveyor surfaces, and efficient motor drives to minimize energy consumption while maintaining high conveying rates. System integration is another key principle, as the equipment must seamlessly integrate with existing production lines and processes. This involves designing the system to be compatible with various control systems and interfaces, allowing for easy integration and operation. Furthermore, durability is ensured by using robust materials and corrosion-resistant coatings that can withstand the harsh conditions of industrial environments, including exposure to dust, moisture, and temperature fluctuations.
Applications and Benefits
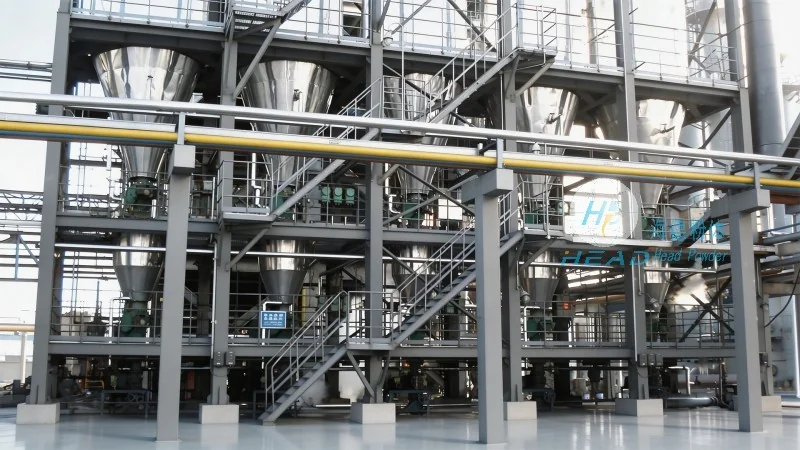
Aggregate powder conveying system equipment finds wide applications across various industries, offering numerous benefits to businesses. In the construction industry, these systems are used to transport aggregates and cement for concrete production, ensuring consistent material supply and reducing manual labor. In mining operations, they help transport ore and other minerals from extraction sites to processing facilities, improving operational efficiency and reducing transportation costs. In manufacturing, they are used to convey raw materials and finished products, streamlining production processes and enhancing overall productivity. The benefits of using these systems include increased operational efficiency, reduced labor costs, minimized material loss, and improved safety. By automating the material handling process, businesses can reduce the risk of accidents and injuries associated with manual material handling, while also improving the quality and consistency of the final product.
About HeadPowder Engineering
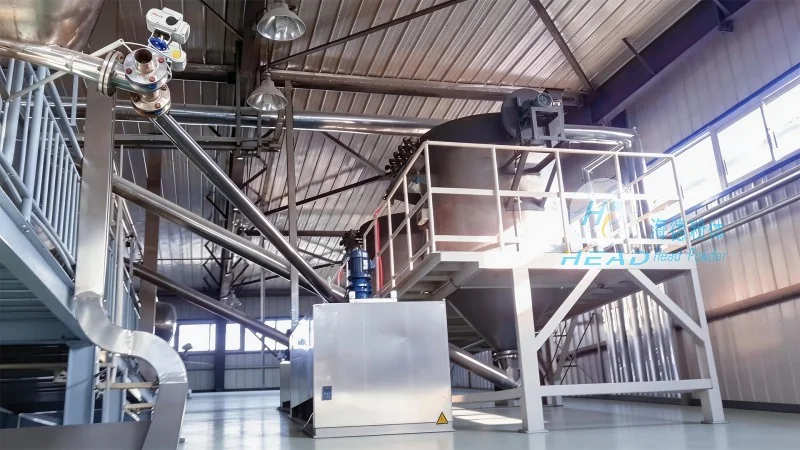
HeadPowder Engineering Co., Ltd., a leading manufacturer of aggregate powder conveying system equipment, is committed to providing high-quality, reliable solutions for material handling needs. With its headquarters in Shandong, China, HeadPowder has established itself as a trusted partner in the industry, delivering innovative and efficient equipment to clients worldwide. The company's expertise lies in designing and manufacturing equipment that meets the specific requirements of various applications, ensuring that clients receive tailored solutions that enhance their operational efficiency. HeadPowder's team of experienced engineers and technicians works closely with clients to understand their unique needs and develop customized solutions that address their specific challenges. The company's commitment to quality and innovation has made it a preferred choice for businesses seeking dependable and efficient material conveying systems. HeadPowder's products are known for their durability, efficiency, and ease of maintenance, making them a valuable investment for any business looking to improve its material handling capabilities.