

Principle of Coffee Powder Pneumatic Conveying Equipment
For businesses involved in the coffee industry, efficient and reliable material handling is crucial. Coffee powder, with its fine particles and potential for dust generation, requires specialized equipment to ensure safe and effective transport. The pneumatic conveying system, a key technology in this field, offers a solution that combines precision, safety, and operational efficiency. This article explores the fundamental principles behind coffee powder pneumatic conveying equipment, highlighting the technical aspects that make it suitable for coffee processing applications. As a leading provider in the industry, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing such equipment tailored to the unique needs of coffee processing facilities.
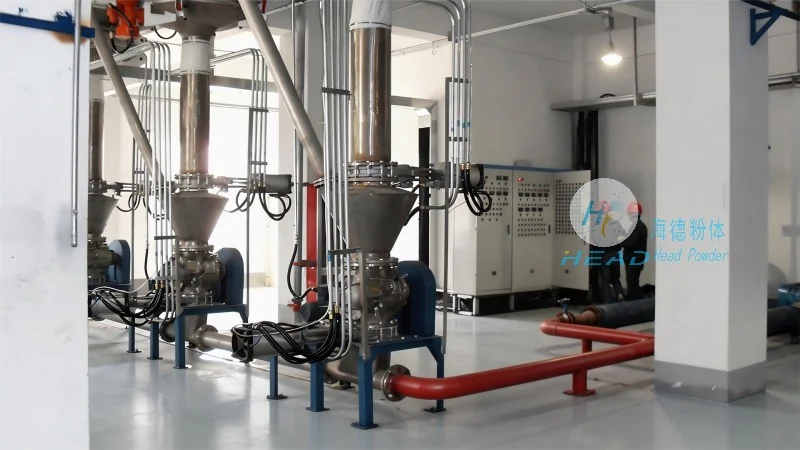
Core Components and Working Principle
The pneumatic conveying system for coffee powder typically consists of several key components, each playing a vital role in the overall operation. The primary elements include a material hopper or feeder, a conveying line (often equipped with a venturi or pressure drop device), a filter system, and a receiver or discharge unit. The process begins with the coffee powder being fed from the hopper into the conveying line under controlled pressure. As the powder enters the line, it is accelerated by the airflow, which can be generated by a positive pressure blower or a vacuum pump, depending on the system design. The venturi or pressure drop device creates a pressure differential that propels the coffee powder through the pipeline. This method ensures that the fine coffee particles are transported without clogging or degradation, maintaining product quality throughout the process.
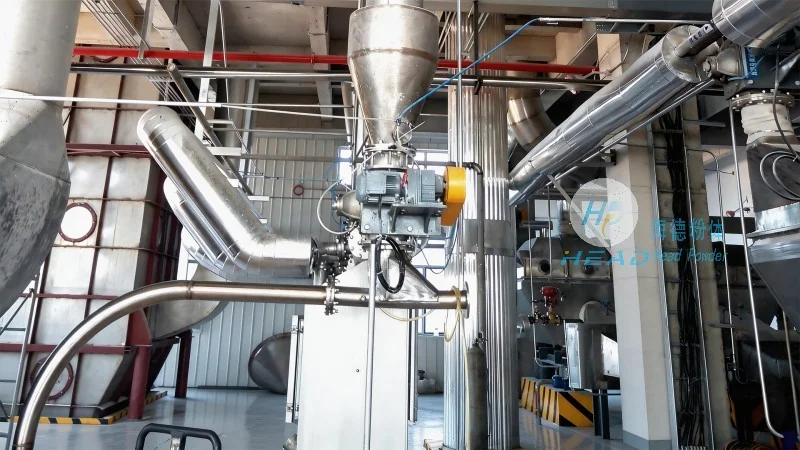
Advantages of Pneumatic Conveying for Coffee Powder
Compared to traditional mechanical conveying methods, such as screw conveyors or belt conveyors, pneumatic conveying offers several distinct advantages for coffee powder handling. First, it eliminates the need for physical contact between the material and the conveying equipment, reducing the risk of contamination and product degradation. Coffee powder is highly sensitive to moisture and temperature changes, and pneumatic systems can maintain consistent conditions, preserving the flavor and aroma of the coffee. Second, the system is highly flexible, allowing for changes in the conveying route without significant modifications. This adaptability is particularly beneficial in coffee processing plants where layout adjustments may be required. Third, pneumatic conveying can handle high volumes of material with minimal maintenance, as there are no moving parts in direct contact with the powder, reducing wear and tear. Additionally, the system can be integrated with dust collection and filtration systems, ensuring compliance with environmental regulations and maintaining a clean working environment.
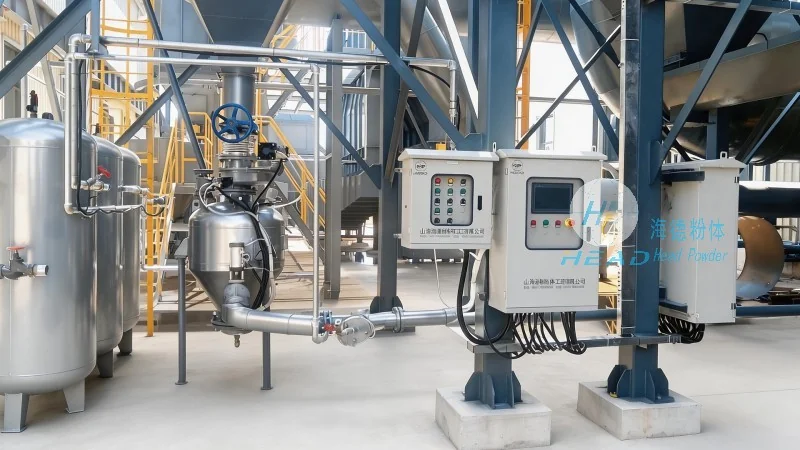
Application Considerations and Best Practices
When implementing a coffee powder pneumatic conveying system, several factors must be considered to optimize performance and ensure longevity. The first consideration is the particle size and moisture content of the coffee powder, as these characteristics directly impact the system's efficiency. Fine particles may require higher air velocities to prevent clogging, while higher moisture content can affect the air-powder ratio needed for effective transport. The system design should also account for the required conveying distance and height, as these parameters influence the pressure requirements and equipment selection. Regular maintenance is critical to prevent system failures, including cleaning of the filter system, checking for air leaks, and inspecting the conveying line for blockages. Proper training for operators on the safe operation of the equipment is also essential to prevent accidents and ensure consistent performance. By adhering to these best practices, coffee processing facilities can maximize the benefits of pneumatic conveying while minimizing operational risks.
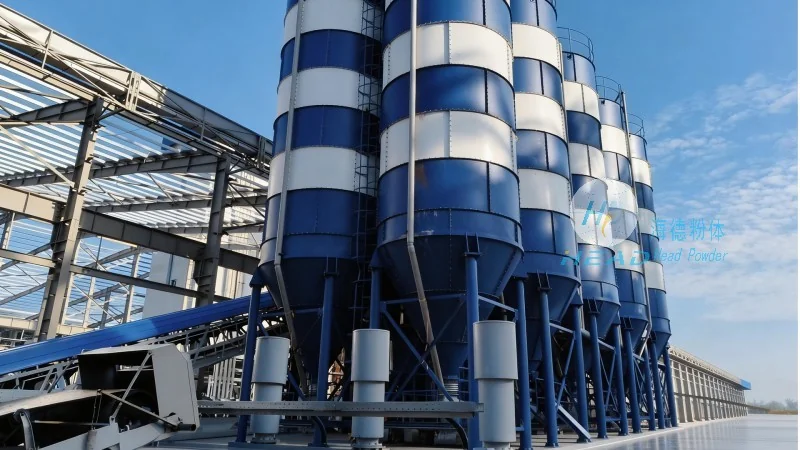
Conclusion
Coffee powder pneumatic conveying equipment represents a sophisticated solution for the efficient handling of fine, sensitive materials in the coffee industry. By leveraging the principles of air flow and pressure differential, these systems provide a reliable, hygienic, and flexible method for transporting coffee powder from storage to processing or packaging areas. The technology not only enhances operational efficiency but also helps maintain the quality and integrity of the coffee product. For companies seeking to improve their material handling processes, investing in a well-designed pneumatic conveying system is a strategic decision that aligns with both productivity and product quality goals. As the coffee industry continues to evolve, the adoption of advanced conveying technologies like pneumatic systems will remain essential for meeting the demands of modern coffee production. Shandong HeadPowder Engineering Co., Ltd. remains committed to delivering high-quality, customized solutions to meet the diverse requirements of coffee processing clients, ensuring optimal performance and long-term reliability.