

Principle and Working Scene Characteristics of Limestone Powder Conveying System Equipment
HeadPowder, a leading provider of industrial powder handling solutions, specializes in the design, manufacturing, and implementation of advanced limestone powder conveying systems. These systems are critical for efficiently transporting limestone powder, a key raw material in various industrial applications, from storage to processing units. This article explores the fundamental principles behind such equipment and highlights the distinct characteristics of their operational environments.
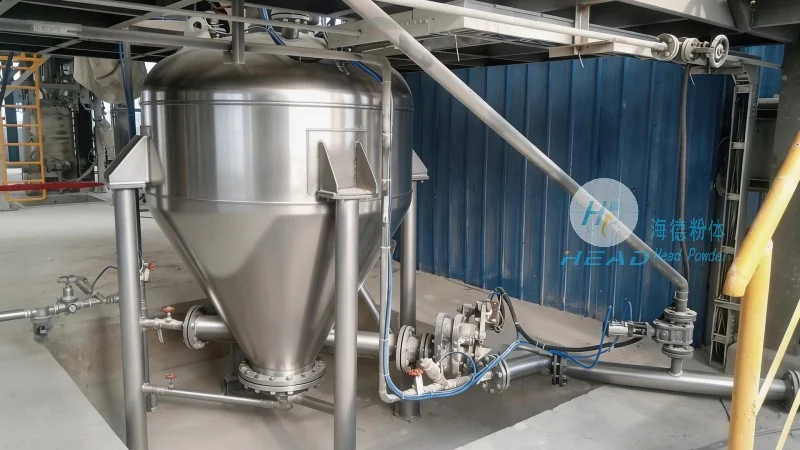
Introduction to Limestone Powder Conveying Systems
Limestone powder conveying systems are engineered to handle the transportation of fine limestone particles, which are commonly used in industries like cement production, chemical manufacturing, and environmental remediation. The efficiency of these systems directly impacts production throughput, material handling costs, and overall operational safety. At Shandong HeadPowder Engineering Co., Ltd., located in Shandong, China, we focus on developing customized solutions that meet the specific demands of our clients, ensuring optimal performance in diverse industrial settings.
Principle of Limestone Powder Conveying Equipment
The core principle of limestone powder conveying systems involves the use of either pneumatic or mechanical methods to move the fine powder from one location to another. Pneumatic conveying systems utilize air pressure to transport the powder through pipelines, while mechanical systems employ screw conveyors, belt conveyors, or bucket elevators. For limestone powder, which is typically dry and free-flowing, pneumatic systems are often preferred due to their ability to handle fine particles without clogging. The equipment design must consider factors such as particle size, moisture content, and the required conveying distance to ensure reliable operation. Our systems are equipped with advanced control mechanisms that regulate air flow, pressure, and speed, maintaining consistent material transport and preventing system downtime.
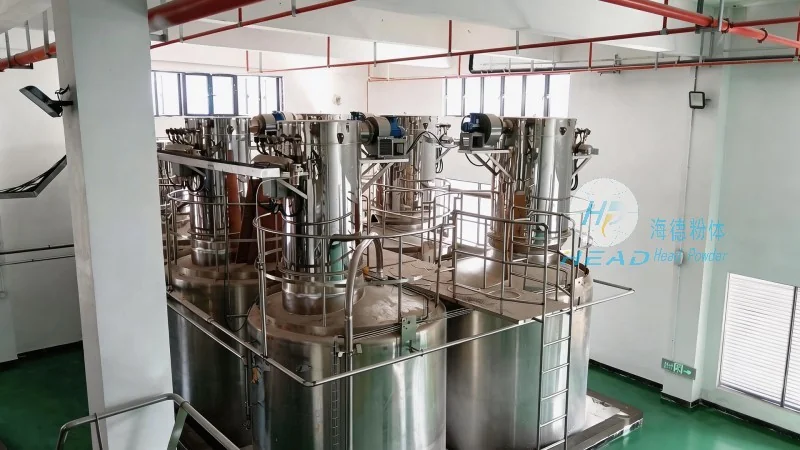
Working Scene Characteristics of Limestone Powder Conveying Systems
The operational environment of limestone powder conveying systems varies significantly depending on the application. In industrial production facilities, these systems are often integrated into larger production lines, requiring seamless coordination with other equipment like mixers, grinders, and reactors. The working scene may involve high-volume material handling, with continuous or batch processing modes. Environmental factors, such as temperature and humidity, also play a role in system performance. For example, in outdoor applications or in regions with high humidity, the system may need additional moisture control measures to prevent material clumping or pipeline blockages. Additionally, safety considerations are paramount, as limestone powder can be dusty and pose respiratory hazards. Our systems incorporate dust collection and filtration systems to maintain a safe working environment and comply with environmental regulations.
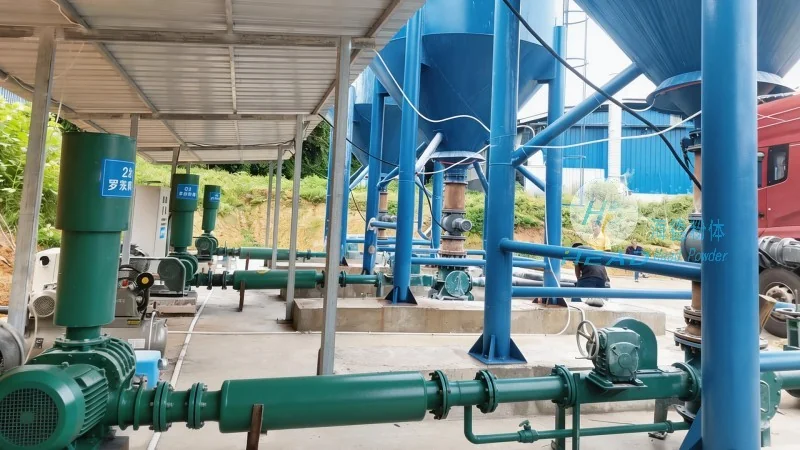
Application Scenarios and Practical Benefits
Limestone powder conveying systems find extensive applications across multiple industries. In the cement industry, they are used to transport limestone from storage silos to grinding mills, ensuring a steady supply of raw material for cement production. In chemical manufacturing, these systems facilitate the transport of limestone for use in processes like flue gas desulfurization, where limestone is used to neutralize acidic emissions. Environmental applications, such as in waste treatment facilities, also rely on limestone powder conveying systems to handle lime for pH adjustment in wastewater treatment. The practical benefits of these systems include reduced labor costs, minimized material loss, and improved process efficiency. By automating the material handling process, companies can achieve higher production rates and lower operational expenses. Moreover, the use of advanced control systems allows for real-time monitoring and adjustment, enhancing system reliability and reducing maintenance requirements.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, operating from Shandong, China, is a reputable company dedicated to providing high-quality industrial powder handling solutions. With years of experience in the field, we have developed a strong reputation for delivering reliable and efficient limestone powder conveying systems. Our team of engineers and technicians is committed to understanding our clients' specific needs and designing customized solutions that meet their operational requirements. We prioritize quality and innovation, investing in research and development to stay at the forefront of industry advancements. Our systems are built to withstand the rigors of industrial environments, ensuring long-term performance and minimal downtime. By choosing HeadPowder, clients can expect not only superior equipment but also excellent customer support and after-sales service. We are dedicated to helping our clients optimize their material handling processes and achieve their business objectives.