

Working Principle and Features of Desulfurization and Dust Removal Fly Ash Material Handling Systems
Desulfurization and dust removal processes in power plants and industrial facilities generate large volumes of fly ash, which requires efficient material handling systems for safe and reliable transport. The material handling system for desulfurization and dust removal fly ash is a critical component in managing these byproducts, ensuring they are transported to storage or disposal sites without compromising safety or environmental standards.
Working Principle of the Material Handling System
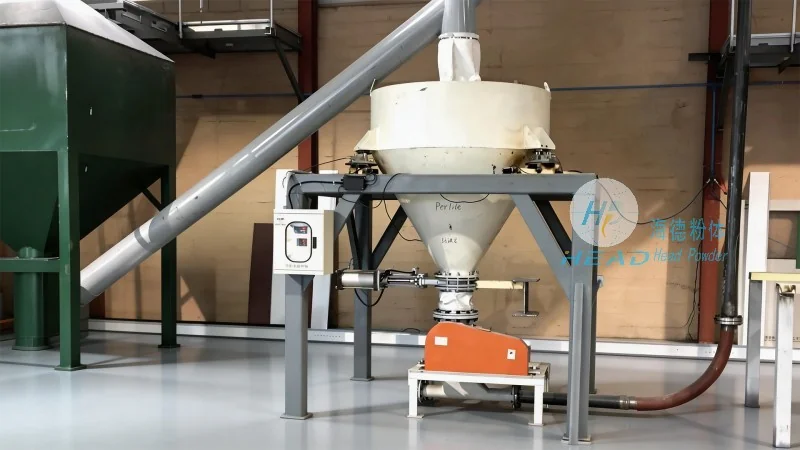
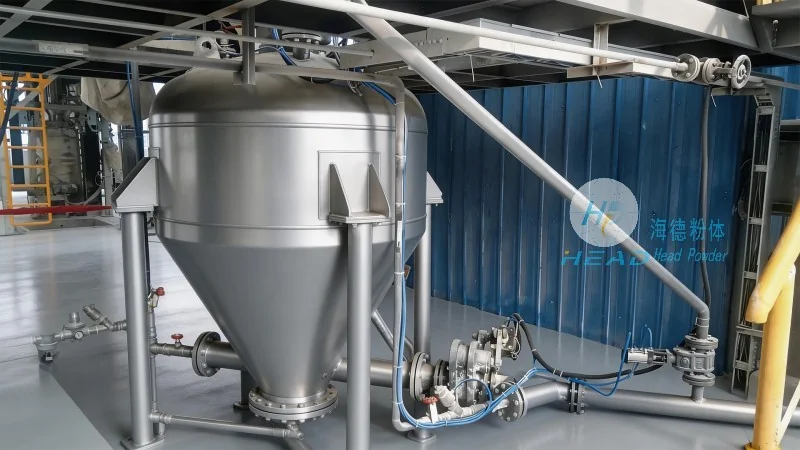
The material handling system for desulfurization and dust removal fly ash operates based on a combination of mechanical and pneumatic principles. Typically, the system starts with the collection of fly ash from the desulfurization and dust removal equipment, such as electrostatic precipitators or bag filters. The collected ash is then transferred to a hopper or storage silo through a series of conveyor belts or screw conveyors. From there, the ash is fed into a pneumatic conveying system, which uses compressed air to transport the material through pipelines to the designated storage or disposal location. The system may also incorporate components like rotary valves, airlocks, and dust collectors to ensure smooth and dust-free operation. The entire process is designed to maintain a consistent flow rate, minimize material loss, and prevent contamination from external sources.
Key Features of the Material Handling System
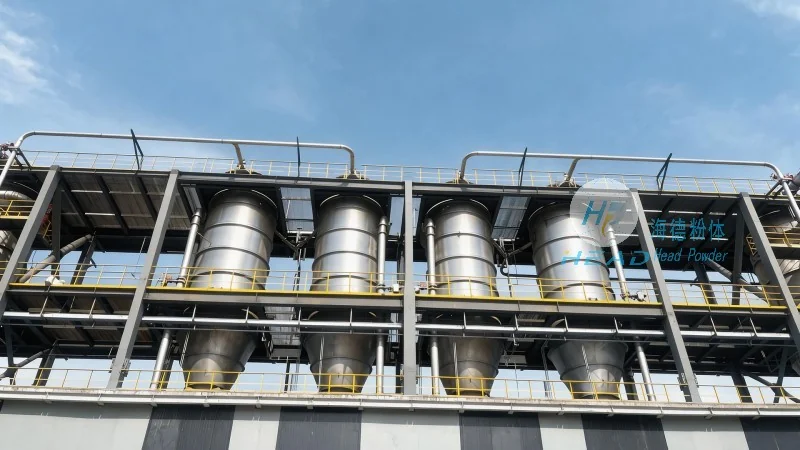
The material handling system for desulfurization and dust removal fly ash is characterized by several key features that enhance its performance and reliability. Firstly, it is designed to handle high-volume ash flows, ensuring that the system can keep up with the production rates of desulfurization and dust removal units. The system incorporates robust materials and components that can withstand the abrasive nature of fly ash, reducing wear and tear and extending the service life of the equipment. Additionally, the system is equipped with advanced control systems that allow for real-time monitoring and adjustment of the conveying process, ensuring optimal performance under varying conditions. The pneumatic conveying aspect of the system provides a dust-free and enclosed transport method, which is crucial for maintaining environmental compliance and worker safety. Furthermore, the system is designed for easy maintenance and repair, with accessible components and modular design that allows for quick replacement of parts without disrupting the entire operation. The integration of safety features, such as pressure relief valves and emergency shutdown systems, ensures that the operation is safe and compliant with industrial safety regulations.
Company Introduction: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading provider of engineering solutions for material handling and processing, specializes in designing and manufacturing systems tailored to the needs of desulfurization and dust removal applications. With a focus on innovation and quality, HeadPowder has developed advanced material handling systems that meet the highest standards of efficiency and reliability. The company's expertise in pneumatic conveying and bulk material handling has enabled it to deliver solutions that address the unique challenges of fly ash transport. HeadPowder's systems are designed to be durable, low-maintenance, and environmentally friendly, ensuring that clients can operate their facilities with minimal downtime and maximum productivity. The company's commitment to customer satisfaction and technical excellence has made it a trusted partner for power plants and industrial facilities worldwide. HeadPowder's systems are manufactured in China, with a dedicated team of engineers and technicians ensuring that each project is executed with precision and care. The company's location in Shandong, China, provides easy access to raw materials and a skilled workforce, enabling HeadPowder to deliver high-quality products at competitive prices. HeadPowder's dedication to continuous improvement and customer support ensures that clients receive not only a high-performance material handling system but also long-term partnership and support.