

Design of Cement Raw Material Pneumatic Conveying Equipment
Shandong HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying systems tailored for cement raw material transport. The company leverages decades of industry experience to deliver customized solutions that enhance operational efficiency and product quality in cement production facilities.
Core Components and Functional Design
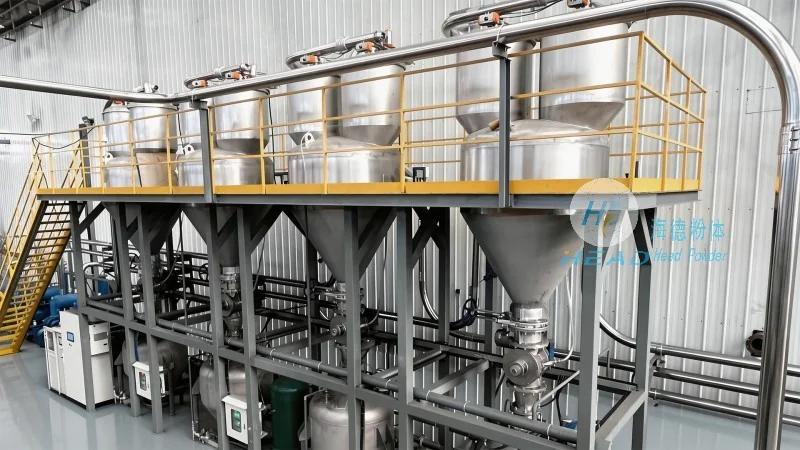
The cement raw material pneumatic conveying equipment developed by HeadPowder Engineering comprises several integral components that work in harmony to ensure reliable material transport. The system typically includes a material feeding hopper, a rotary valve or feeder for controlled material discharge, a conveying pipeline network, and an air compressor or vacuum system to generate the necessary pressure or suction. The design prioritizes material flow consistency by incorporating adjustable feed controls and pressure regulation mechanisms.
Material handling efficiency is optimized through the selection of appropriate pipeline diameters and air velocities. For instance, limestone and clay, common cement raw materials, are conveyed at air velocities between 20-30 m/s to prevent particle segregation and ensure smooth transport. The system may employ positive pressure (pressure pneumatic conveying) or negative pressure (vacuum pneumatic conveying) depending on the plant layout and material characteristics. Positive pressure systems are often preferred for long-distance transport due to their ability to maintain consistent pressure and prevent air leakage.
Advanced Control and Monitoring Systems
Modern cement raw material pneumatic conveying systems integrate sophisticated control and monitoring technologies to enhance operational reliability and performance. The system features real-time pressure sensors, flow meters, and temperature gauges that provide continuous feedback on the conveying process. Automated control panels allow operators to adjust parameters such as air pressure, feed rate, and pipeline pressure dynamically, ensuring optimal material throughput and preventing system overloads or blockages.
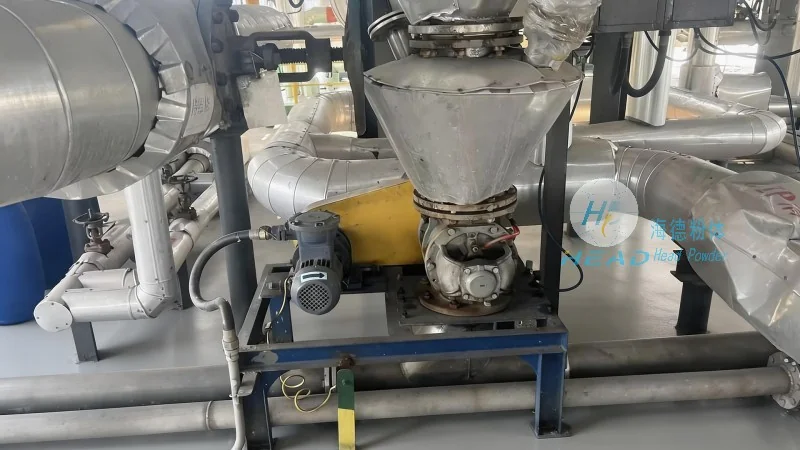
Integrated safety features are standard in the design, including pressure relief valves, emergency shut-off switches, and interlocks that prevent operation under abnormal conditions. The control system may also include data logging capabilities, enabling plant managers to track performance metrics over time and identify areas for improvement. This data-driven approach helps in optimizing energy consumption and reducing maintenance costs through predictive maintenance strategies.
Material Compatibility and Wear Resistance
The cement raw material pneumatic conveying equipment is engineered to handle the abrasive and corrosive nature of cement raw materials, such as limestone, clay, and iron ore. The components in contact with the material, including hoppers, feeders, and pipeline sections, are constructed from high-quality materials like stainless steel, special alloys, and wear-resistant coatings. These materials are selected to withstand the mechanical stress and chemical exposure associated with cement production, ensuring extended service life and minimal downtime.
For particularly abrasive materials, the system may incorporate special wear-resistant liners or replaceable components. The design also considers the potential for material buildup and blockages, with features such as in-line mixers and classifiers to maintain material homogeneity and prevent clogging. The use of smooth, non-porous pipeline surfaces further reduces friction and wear, contributing to the overall durability of the system.
Integration with Existing Plant Infrastructure
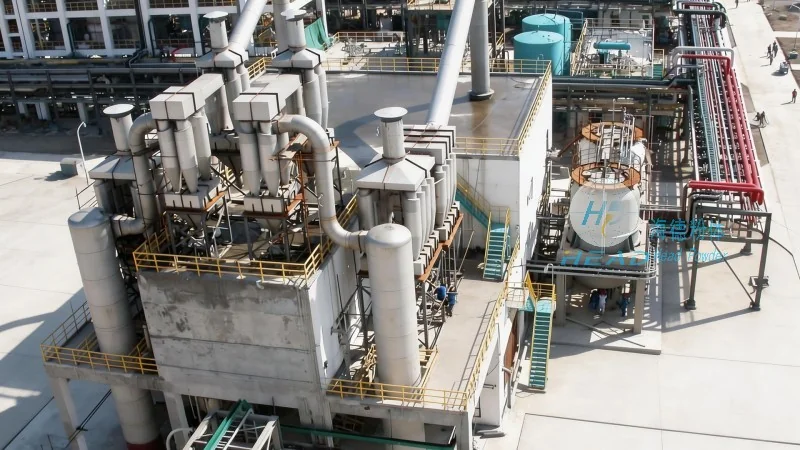
HeadPowder Engineering recognizes that cement plants often have existing infrastructure and operational constraints. The cement raw material pneumatic conveying system is designed with flexibility to integrate seamlessly with existing production lines, minimizing disruption during installation and commissioning. The system can be adapted to various plant layouts, including vertical and horizontal conveying configurations, and can accommodate different material feed points and discharge locations.
The company provides comprehensive engineering support, including site surveys, process analysis, and detailed design documentation. This ensures that the final solution aligns with the client's operational requirements and complies with local regulations and industry standards. The team of experienced engineers works closely with clients to develop tailored solutions that optimize material handling, reduce operational costs, and enhance overall plant productivity.
Performance Optimization and Cost Efficiency
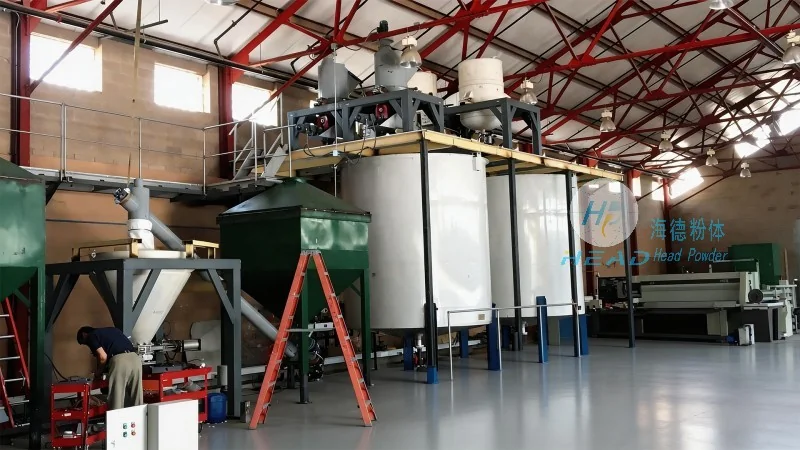
The cement raw material pneumatic conveying system from HeadPowder Engineering is engineered for maximum performance and cost efficiency. By reducing material handling time and labor requirements compared to traditional methods like belt conveyors or bucket elevators, the system lowers operational costs significantly. The consistent material flow and reduced segregation also contribute to improved cement quality and reduced variability in the final product, leading to higher customer satisfaction and market competitiveness.
Energy efficiency is a key consideration in the system's design. Optimized air velocity and pipeline design minimize energy consumption, resulting in lower electricity bills and reduced environmental impact. The system's modular construction allows for easy scale-up or modification as production needs evolve, providing long-term value and adaptability. Additionally, the reduced need for manual handling enhances workplace safety by minimizing the risk of accidents and injuries.
Conclusion
Shandong HeadPowder Engineering Co., Ltd. offers a comprehensive range of cement raw material pneumatic conveying equipment designed to meet the evolving needs of the cement industry. With its focus on innovation, quality, and customer-centric solutions, the company provides reliable systems that enhance operational efficiency, improve product quality, and reduce costs. The expertise and experience of HeadPowder make it a trusted partner for cement manufacturers seeking to upgrade their material handling infrastructure and maintain a competitive edge in the global market.