

Cement Pneumatic Conveying System Solutions
Efficient and reliable transport of cement and other fine bulk materials is essential for modern industrial operations. Pneumatic conveying systems have emerged as a preferred solution due to their ability to handle powders with minimal degradation and high throughput. These systems operate by using compressed air to move material through pipelines, offering a flexible and cost-effective alternative to traditional methods like belt conveyors or bucket elevators. The design of a cement pneumatic conveying system involves careful consideration of factors such as material properties, conveying distance, and required flow rates, ensuring optimal performance and longevity.
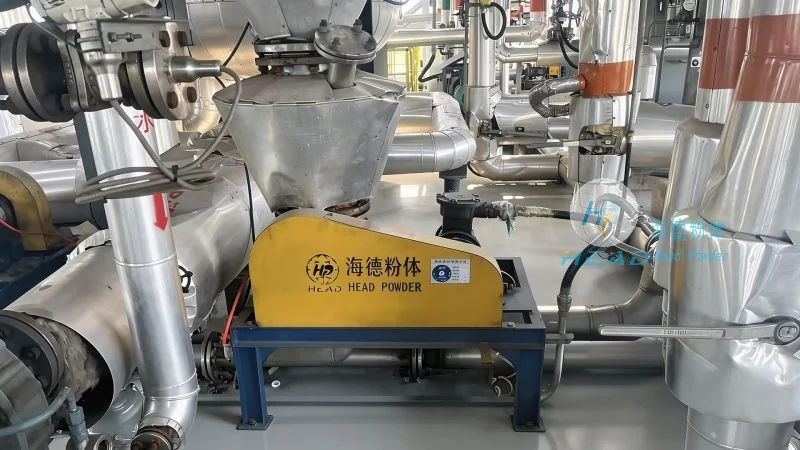
HeadPowder: Your Expert in Cement Pneumatic Conveying
Shandong HeadPowder Engineering Co., Ltd., commonly referred to as HeadPowder, is a leading engineering firm specializing in bulk material handling solutions. With headquarters in Shandong, China, HeadPowder has built a reputation for delivering high-quality, customized pneumatic conveying systems tailored to the specific needs of clients across various industries. The company's team of experienced engineers and technicians leverages advanced technology and industry best practices to design, manufacture, and implement systems that enhance operational efficiency and reduce costs.
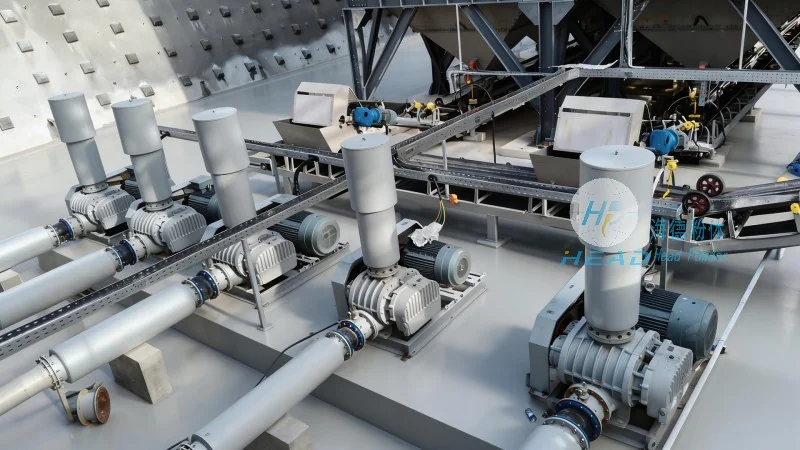
Key Features of Cement Pneumatic Conveying Systems
The effectiveness of a cement pneumatic conveying system is determined by its key components and operational design. High-pressure systems, typically used for longer distances or higher flow rates, generate sufficient air pressure to move material through pipelines efficiently. Low-pressure systems, on the other hand, are suitable for shorter distances and lower material volumes. Both types may incorporate rotary air locks to control material flow and prevent backflow, while cyclone separators and dust collectors ensure that the material remains clean and free from contaminants. The selection of these components is critical to maintaining system efficiency and extending equipment lifespan.
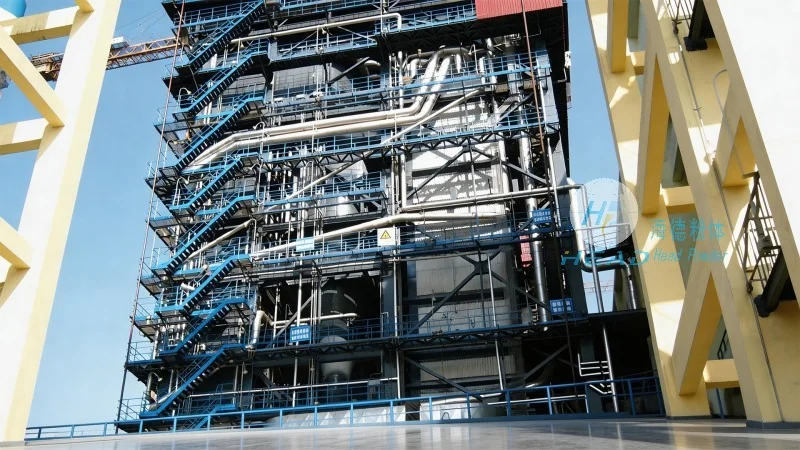
Applications and Industries Served
Cement pneumatic conveying systems find widespread application in the cement manufacturing industry, where they are used to transport raw materials like limestone and clinker, as well as finished cement products. In construction, these systems enable quick and reliable delivery of cement to job sites, improving project timelines and reducing labor costs. The chemical and pharmaceutical industries also benefit from pneumatic conveying, as it minimizes material exposure to the environment and ensures consistent quality. Additionally, in food processing and agricultural sectors, where hygiene and material purity are paramount, pneumatic systems provide a safe and efficient method for handling powders.
Customization and Integration Capabilities
HeadPowder recognizes that no two projects are identical, and thus offers comprehensive customization options for cement pneumatic conveying systems. The company works closely with clients to understand their operational requirements, including conveying distance, material characteristics, and available space. Based on this information, HeadPowder designs systems that may include multiple pipelines, branching configurations, or integrated storage silos. The systems can be integrated with existing production lines or designed as standalone solutions, ensuring seamless operation and minimal disruption to current workflows. Furthermore, HeadPowder provides technical support throughout the entire project lifecycle, from initial design and installation to ongoing maintenance and system optimization.
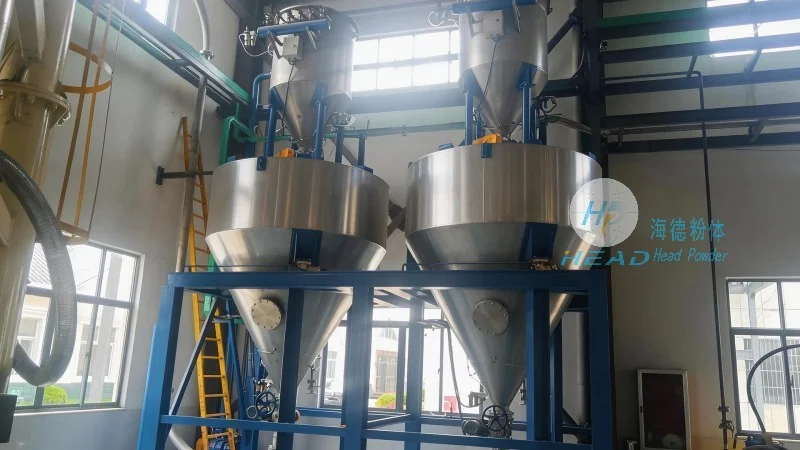
Quality Assurance and Technical Support
At HeadPowder, quality is not just a standard but a core value. The company adheres to international engineering standards and employs rigorous testing protocols to ensure the durability and reliability of its pneumatic conveying systems. Each system undergoes comprehensive performance testing, including pressure tests, flow rate validation, and material handling simulations, to confirm it meets the specified requirements. The use of high-quality materials and advanced manufacturing processes further enhances the longevity of the equipment. Beyond the initial delivery, HeadPowder offers comprehensive technical support, including on-site installation assistance, regular maintenance services, and remote monitoring capabilities. This commitment to after-sales support ensures that clients can rely on their systems for long-term, trouble-free operation, maximizing return on investment.