

Operation Process and Working Principle of Vanadium Oxide Material Handling System Equipment
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design, manufacturing, and implementation of advanced material handling systems tailored for the processing of vanadium oxide materials. This article provides a detailed overview of the operational process and underlying principles of such systems, ensuring a comprehensive understanding for industry professionals and potential clients.
Company Overview and Core Expertise
HeadPowder Engineering Co., Ltd. is a reputable enterprise dedicated to providing high-quality engineering solutions for material handling in the chemical and mineral processing sectors. With a focus on precision and efficiency, the company has established itself as a trusted partner for clients requiring specialized equipment for handling vanadium oxide and other similar materials. The company's headquarters is located in Shandong, China, where a team of experienced engineers and technicians work collaboratively to develop and refine material handling systems that meet stringent industry standards.
System Components and Design Philosophy
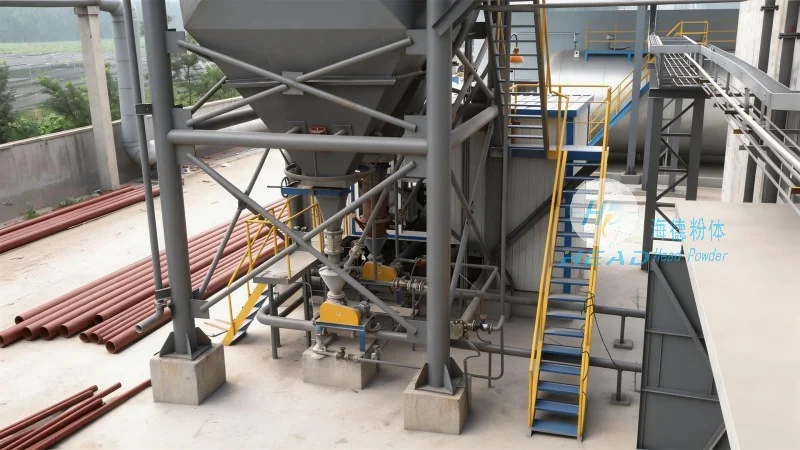
The vanadium oxide material handling system typically comprises several key components, each designed to work in harmony to ensure smooth and efficient material transport. These components include feeders, conveyors, storage silos, and control systems, all engineered to handle the unique properties of vanadium oxide, such as its density, particle size, and chemical reactivity. The design philosophy emphasizes durability, low maintenance, and adaptability to varying production demands. For instance, the feeders are often equipped with adjustable speed controls to regulate the flow rate of material, preventing overloading or underflow. The conveyors may utilize belt or screw mechanisms, selected based on the specific characteristics of the vanadium oxide and the required transport distance. Storage silos are constructed with corrosion-resistant materials to protect the material from degradation and ensure long-term storage stability.
Operation Process: Step-by-Step Workflow
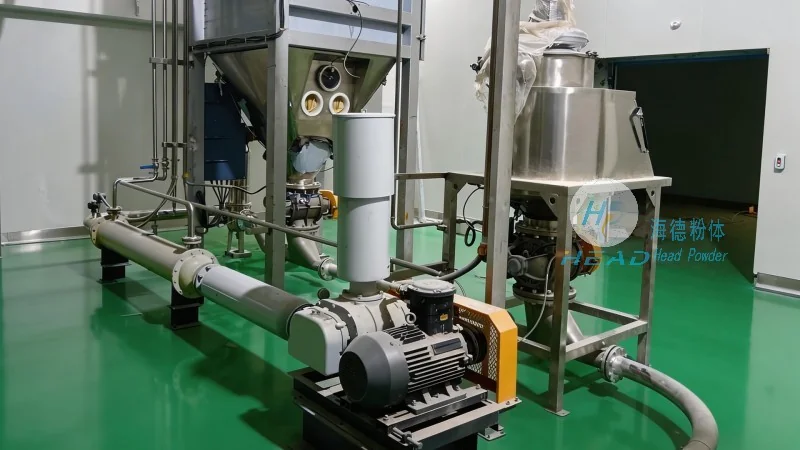
The operation of the vanadium oxide material handling system follows a systematic workflow that ensures consistent and reliable material movement from the source to the processing unit. The process begins with the material being fed into the system, either from a bulk storage container or an external source. The feeder then regulates the flow of material into the conveyor system. The conveyor transports the material to the storage silo or directly to the processing equipment, depending on the production requirements. During this stage, the control system continuously monitors the flow rate, pressure, and temperature to maintain optimal operating conditions. The system may also include sensors to detect blockages or abnormalities, triggering automatic shutdowns or alerts to prevent damage to equipment or material loss. After reaching the processing unit, the material is further handled according to the specific requirements of the downstream processes, such as grinding, mixing, or chemical treatment.
Working Principle: Mechanical and Control Integration
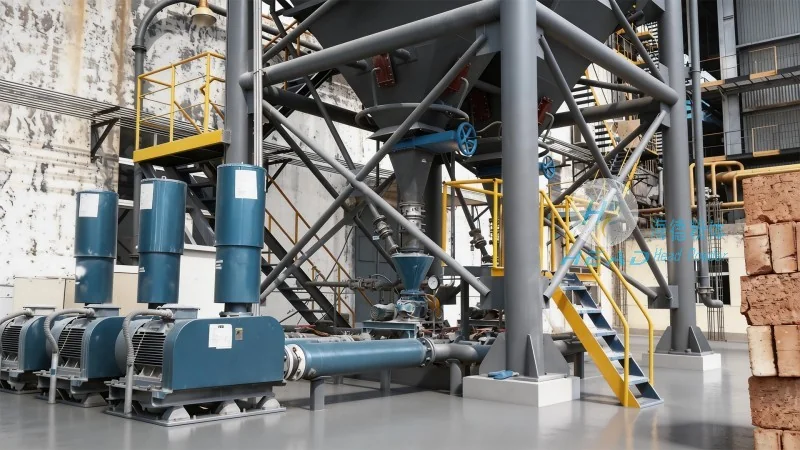
The working principle of the vanadium oxide material handling system integrates mechanical components with advanced control technology to achieve precise and efficient material handling. The mechanical components, such as conveyors and feeders, convert electrical energy into mechanical motion to move the material. The control system, often based on programmable logic controllers (PLCs) or industrial computers, manages the operation of these components by receiving input from sensors and sending output signals to actuators. This integration allows for real-time monitoring and adjustment of the system's performance. For example, the control system can adjust the speed of the conveyor based on the material flow rate detected by the sensors, ensuring that the material is transported at an optimal rate without causing congestion or spillage. Additionally, the system may incorporate safety features, such as emergency stop buttons and overload protection, to prevent accidents and protect personnel and equipment.
Key Advantages and Industry Applications
HeadPowder's vanadium oxide material handling systems offer several advantages that make them suitable for various industrial applications. These include high efficiency in material transport, reduced labor costs due to automated operations, and enhanced safety through integrated control systems. The systems are particularly beneficial in the production of vanadium compounds, where consistent material handling is crucial for maintaining product quality and reducing waste. Additionally, the systems are designed to be flexible, allowing for easy integration with existing production lines or expansion as production needs grow. The durability of the equipment, combined with low maintenance requirements, results in long-term cost savings for clients. In summary, the vanadium oxide material handling systems from HeadPowder are engineered to meet the demanding requirements of modern industrial processes, providing reliable and efficient solutions for material handling in the chemical and mineral processing sectors.