

Operation Process and Working Principle of Ammonium Sulfate Material Handling System Equipment
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, specializes in the design, manufacturing, and installation of industrial material handling systems. With a focus on efficient and reliable solutions for bulk material transport, the company has established itself as a leading provider in the field, particularly for applications involving ammonium sulfate and other similar chemical compounds.
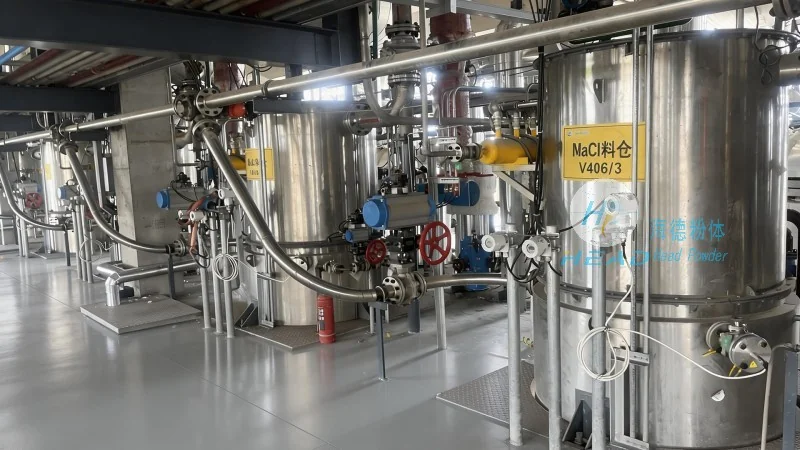
Operation Process of Ammonium Sulfate Material Handling Equipment
The operation of the ammonium sulfate material handling system begins with the loading of raw materials into the storage silo. The system utilizes a series of conveyor belts, feeders, and pneumatic or mechanical transport mechanisms to move the material from the storage area to the processing or packaging stages. Each component is designed to handle the specific characteristics of ammonium sulfate, such as its granular structure and potential moisture content, ensuring minimal material degradation and loss during transit. The process typically involves the following steps: material intake, initial feeding, conveyance through the system, and final discharge into the next processing unit. The system is equipped with sensors and control panels that monitor the flow rate, pressure, and temperature to maintain optimal operating conditions. Operators can adjust the system parameters in real-time to adapt to varying production demands, ensuring smooth and continuous operation.
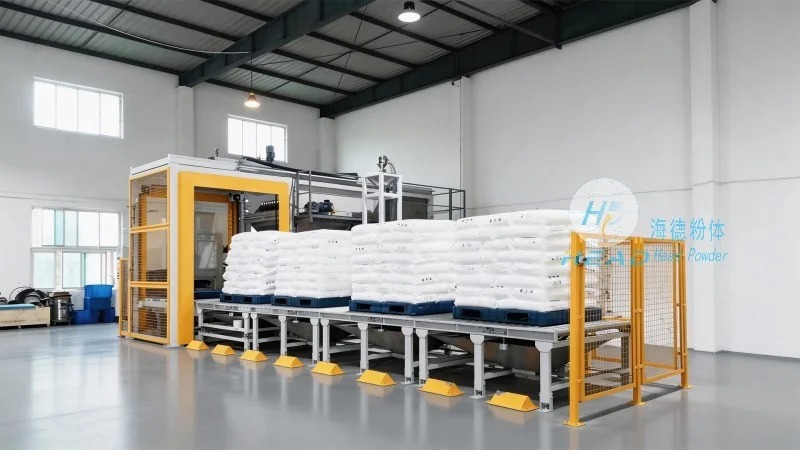
Working Principle of the Ammonium Sulfate Material Handling System
The core of the system's functionality lies in its integrated design, which combines mechanical, pneumatic, and sometimes hydraulic components to achieve efficient material transport. The system operates on the principle of gravity and controlled force application, where material is moved from a higher elevation to a lower one, or horizontally across the facility. Conveyor belts, often equipped with special belts or buckets, are used to transport the material in a continuous flow. For vertical transport, bucket elevators or pneumatic conveying lines are employed, which use air pressure to move the material through pipes. The system's control system manages the flow by regulating the speed of conveyors, the rotation of fans in pneumatic lines, and the operation of feeders. This ensures that the material is moved at a consistent rate, preventing blockages and maintaining system efficiency. The working principle also incorporates safety features, such as overload protection and emergency stop mechanisms, to safeguard both the equipment and the personnel operating the system.
Key Features of the Ammonium Sulfate Material Handling System
HeadPowder's ammonium sulfate material handling system is engineered with several key features that enhance its performance and reliability. One of the primary features is the use of high-quality, corrosion-resistant materials for all components, which is essential for handling ammonium sulfate and other chemical substances that may be abrasive or reactive. The system is designed to minimize dust generation, incorporating sealed conveyor sections and dust collection systems to maintain a clean and safe working environment. Additionally, the system is equipped with automated control systems that allow for remote monitoring and operation, reducing the need for manual intervention and improving operational efficiency. The modular design of the system allows for easy expansion or modification as production needs change, providing flexibility for growing businesses. Another important feature is the integration of maintenance-friendly components, such as easily accessible bearings and replaceable parts, which reduces downtime and maintenance costs over the system's lifespan.

Applications and Industries Served
The ammonium sulfate material handling system is widely used in various industries that require the efficient transport of bulk chemical materials. These include the fertilizer industry, where ammonium sulfate is a common nitrogen source for agricultural applications. The system is also used in chemical manufacturing plants, where it helps in the transport of raw materials and intermediate products. Additionally, the system is suitable for use in food processing facilities, where it can handle ammonium sulfate used as a food additive or preservative. The system's versatility makes it applicable in any setting where bulk material handling is required, ensuring that the material is moved safely and efficiently from storage to processing or packaging stages.