

Operation Process and Working Principle of Denitrizer Material Handling System
For industrial facilities that rely on selective catalytic reduction (SCR) technology to control nitrogen oxide emissions, the efficient and reliable transport of denitrifier materials is a critical component of the overall process. The denitrifier material handling system, as provided by Shandong HeadPowder Engineering Co., Ltd., is designed to ensure seamless and safe operation from material storage to injection point. This article will explore the operation process and working principle of such a system, highlighting key components and their functions.
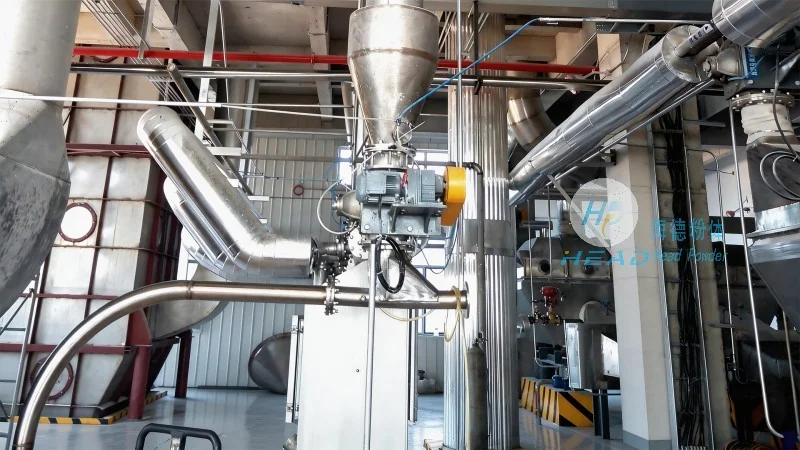
Key Components of the Denitrizer Material Handling System
The denitrifier material handling system typically consists of several integrated components that work in concert to achieve optimal performance. These components include bulk material storage silos, material feeders, conveyor systems, pneumatic or mechanical conveying equipment, and injection or dosing units. Each component plays a vital role in maintaining the flow of denitrifier chemicals, such as urea or ammonia-based solutions, to the SCR reactor.
Operation Process of the Denitrizer Material Handling System
The operation process of the denitrizer material handling system can be broken down into several sequential steps. First, the denitrifier material is stored in bulk silos under controlled conditions to prevent degradation or moisture absorption. The material is then fed from the silo to a feeder, which regulates the flow rate based on the required dosage. The feeder may be a rotary valve, a screw feeder, or a vibratory feeder, depending on the material characteristics and system design. From the feeder, the material is conveyed to the injection point via a conveyor or pneumatic system. The conveying system ensures that the material is transported at the correct velocity and pressure to maintain a consistent flow. Finally, the material is injected into the SCR reactor, where it reacts with nitrogen oxides to form harmless nitrogen and water.
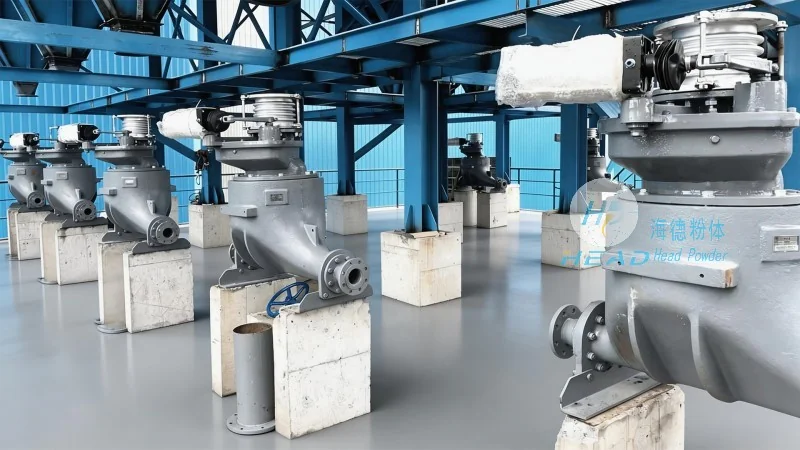
Working Principle of the Denitrizer Material Handling System
The working principle of the denitrizer material handling system is based on the principles of material flow and chemical reaction control. The system utilizes a combination of mechanical and pneumatic forces to move the denitrifier material from the storage silo to the injection point. The feeder controls the initial flow rate, while the conveyor or pneumatic system maintains the material's velocity and pressure. The injection unit then atomizes or disperses the material into the flue gas stream, ensuring thorough mixing with nitrogen oxides. The entire process is monitored and controlled by a programmable logic controller (PLC) or a distributed control system (DCS), which adjusts parameters such as flow rate, pressure, and temperature to maintain optimal denitrification efficiency.
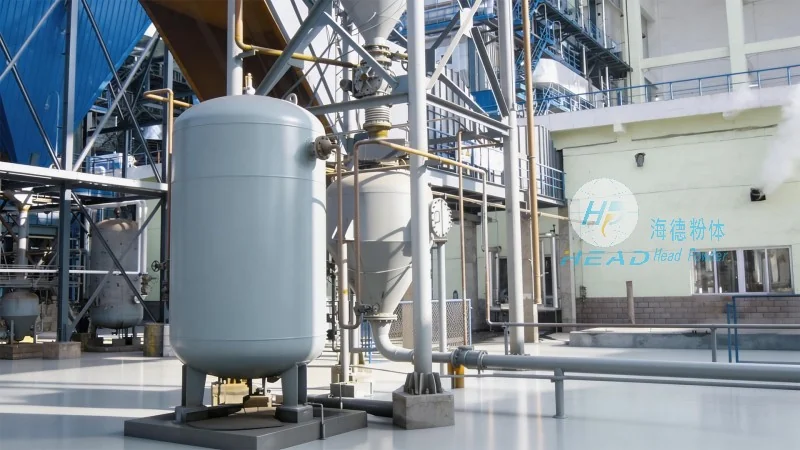
Advantages of the Denitrizer Material Handling System
Implementing a well-designed denitrifier material handling system offers several advantages for industrial plants. Firstly, it ensures consistent and accurate dosing of denitrifier chemicals, which directly impacts the efficiency of the SCR process. This leads to lower nitrogen oxide emissions and compliance with environmental regulations. Secondly, the system enhances operational safety by preventing material buildup, clogging, or overpressure in the conveying lines. Thirdly, the automated control system reduces the need for manual intervention, minimizing human error and labor costs. Finally, the modular design of the system allows for easy maintenance and scalability, adapting to changes in production capacity or process requirements.
Conclusion
The denitrizer material handling system is a critical component of modern industrial processes that rely on SCR technology for nitrogen oxide control. By understanding the operation process and working principle of such a system, plant operators can optimize performance, ensure compliance, and reduce operational costs. Shandong HeadPowder Engineering Co., Ltd. specializes in providing high-quality denitrifier material handling systems tailored to the specific needs of industrial facilities, ensuring reliable and efficient operation.