

Principle and Application Scenarios of Wood Chip Powder Pneumatic Conveying
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a professional manufacturer and supplier specializing in pneumatic conveying systems for wood chip powders. HeadPowder is headquartered in Shandong, China, and has established itself as a key player in the industry by providing efficient and reliable solutions for wood chip material handling.
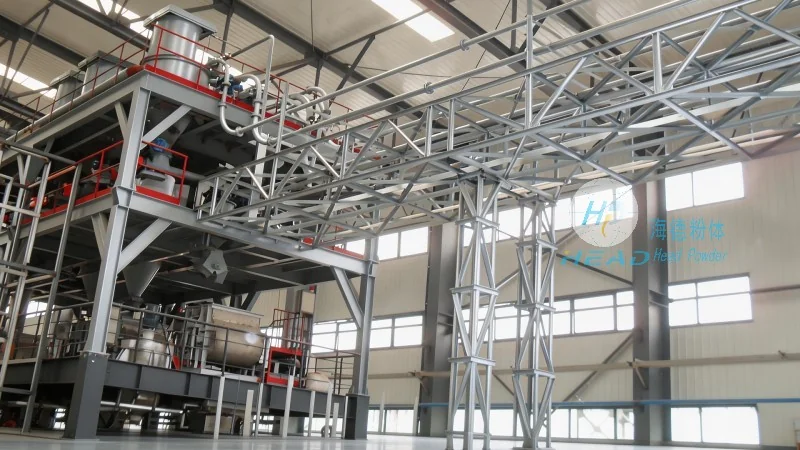
Principle of Pneumatic Conveying for Wood Chip Powders
Pneumatic conveying, also known as air conveying, is a method of transporting bulk materials like wood chips through a pipeline using compressed air. The core principle involves creating a pressure differential between the inlet and outlet of the conveying system. In this process, wood chips are fed into the system, and a fan or blower generates the necessary airflow to move the material. The system typically consists of a hopper, a conveyor line, and a receiver. The compressed air forces the wood chips to flow through the pipeline, ensuring a continuous and controlled transfer. This method eliminates the need for mechanical components such as belts or screws, reducing maintenance and operational costs. The efficiency of pneumatic conveying depends on factors like the particle size of the wood chips, the air pressure, and the pipeline design. HeadPowder's systems are engineered to optimize these parameters, ensuring high conveying rates and minimal material degradation.
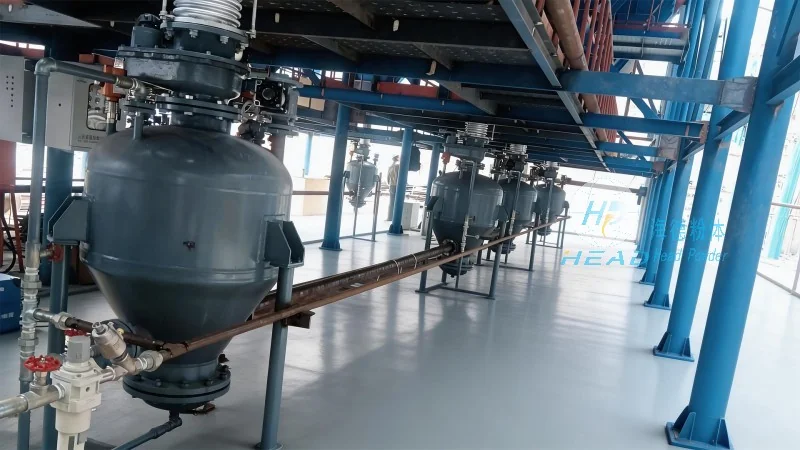
Key Application Scenarios and Characteristics
Wood chip pneumatic conveying systems are widely used in various industrial settings, each with distinct characteristics that make them suitable for specific applications. One common scenario is in the wood processing industry, where wood chips are transported from storage areas to processing facilities. In this context, the system must handle large volumes of material while maintaining low energy consumption. HeadPowder's solutions are designed to meet these demands, with robust construction and energy-efficient components. Another application is in the biofuel sector, where wood chips are conveyed to biomass boilers or pelletizing machines. Here, the system needs to ensure consistent material flow to maintain the efficiency of the combustion process. The characteristics of wood chip pneumatic conveying include high capacity, flexibility in pipeline layout, and the ability to handle abrasive materials without significant wear. Additionally, the system can be adapted for different particle sizes, from fine powders to larger chips, making it versatile for various processing needs. HeadPowder's expertise lies in customizing these systems to match the specific requirements of each client, ensuring optimal performance and longevity.
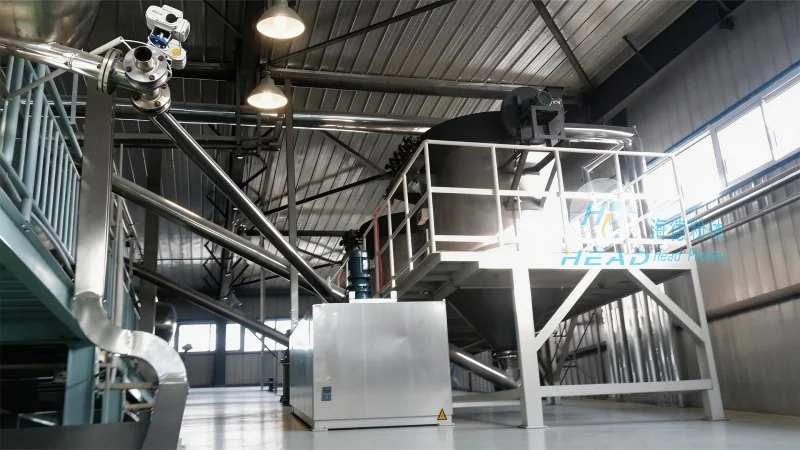
System Components and Operational Advantages
The pneumatic conveying system for wood chips typically includes several key components that work in tandem to ensure smooth operation. The primary components are the material hopper, which stores the wood chips and feeds them into the system; the air compressor or fan, which generates the necessary airflow; the conveying pipeline, which transports the material; and the receiver, where the wood chips are deposited. The hopper is designed with a feeding mechanism, such as a rotary valve or a screw feeder, to control the flow of wood chips into the pipeline. The air compressor provides the pressure required to move the material, with options ranging from positive pressure to negative pressure systems. The pipeline is usually made of stainless steel or other corrosion-resistant materials to withstand the abrasive nature of wood chips. The receiver is equipped with a dust collection system to prevent air leakage and maintain a clean environment. Operational advantages of wood chip pneumatic conveying include high conveying rates, which can reach several tons per hour, and the ability to transport materials over long distances without the need for intermediate storage. The system also offers flexibility in terms of layout, as pipelines can be installed in various configurations to fit the space constraints of the facility. HeadPowder's systems are designed with these advantages in mind, ensuring that clients can achieve efficient material handling with minimal downtime and maintenance.