

Principles and Application Scenarios of Coal Granular Material Conveying
Coal granular material conveying is a critical process in various industrial sectors, particularly in the mining and energy industries. The efficient transport of coal particles from one location to another is essential for maintaining operational productivity and ensuring the smooth flow of resources. This article explores the fundamental principles underlying coal granular material conveying systems and highlights the key characteristics of different working scenarios where such systems are commonly employed.
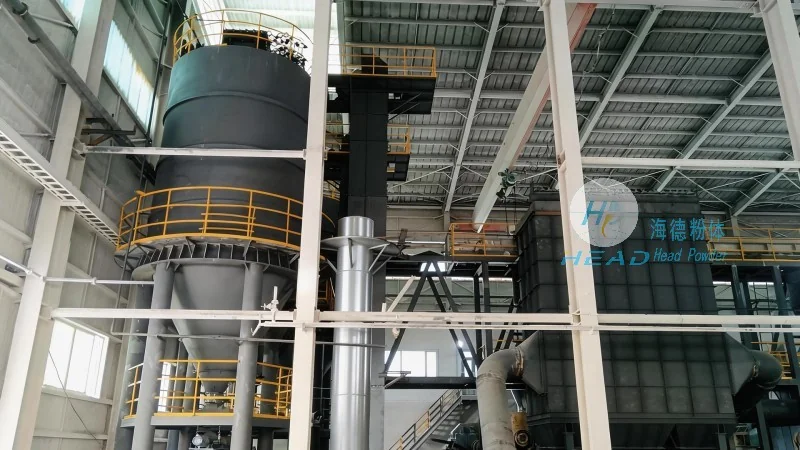
Understanding the Core Principles of Coal Granular Material Conveying
The conveyance of coal granular materials typically involves mechanical systems designed to handle bulk materials with specific properties. These systems are engineered to manage the challenges posed by coal's particle size, density, and moisture content. The primary principles include the use of gravity, mechanical force, or a combination of both to move materials along a defined path. Common conveying methods include belt conveyors, screw conveyors, and pneumatic conveyors, each with distinct advantages and applications.
Belt conveyors, for instance, are widely used due to their high capacity and ability to transport materials over long distances. They consist of a continuous loop of material that moves items from the loading point to the discharge point. The design of the belt, including its width, speed, and inclination, is carefully optimized to ensure efficient material handling. Screw conveyors, on the other hand, use a rotating helical screw to push materials forward, making them suitable for vertical or inclined transport. Pneumatic conveyors utilize air pressure to move materials through a pipeline, which is ideal for dusty or hazardous environments.
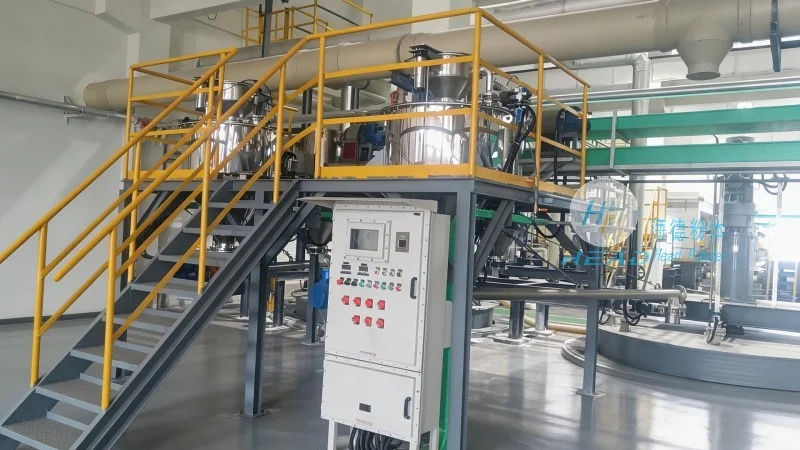
Key Working Scene Characteristics of Coal Granular Material Conveying Systems
The effectiveness of coal granular material conveying systems is heavily influenced by the specific working scenarios in which they operate. These scenarios can vary significantly based on the industry, the scale of operations, and the environmental conditions. For example, in coal mining operations, the system must be robust enough to handle large volumes of raw coal from the mine face to processing facilities. The working environment in such cases is often harsh, with high dust levels and potential for mechanical stress, requiring durable and reliable equipment.
In power plants and thermal energy facilities, the conveying system must ensure a steady supply of coal to the boilers. Here, the focus is on consistent flow rates and minimal downtime. The working scene may involve multiple stages of processing, such as crushing, screening, and storage, each requiring specialized conveying equipment to maintain the material's quality and integrity. Additionally, the system must be integrated with other plant processes, such as fuel handling and combustion systems, to ensure seamless operation.
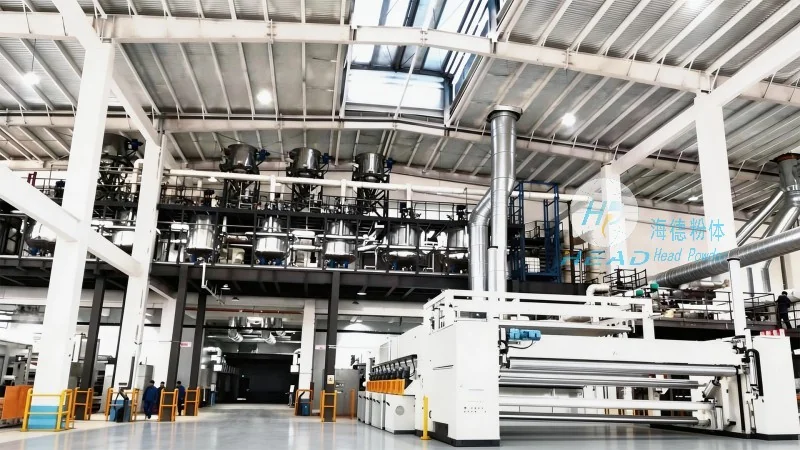
In industrial manufacturing and processing plants, coal granular material conveying may be used for secondary applications, such as in the production of coal-based chemicals or as a fuel source for industrial furnaces. The working scene in these settings often involves smaller-scale operations compared to mining or power generation, but still demands precision and efficiency. The equipment used may include smaller belt conveyors or specialized screw conveyors tailored to the specific requirements of the manufacturing process.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading provider of advanced conveying solutions for coal granular materials. With a strong presence in China, particularly in Shandong province, the company specializes in designing, manufacturing, and implementing customized conveying systems that meet the unique needs of its clients. Headpowder's expertise lies in understanding the diverse working scenarios and adapting its technology to optimize material transport efficiency.
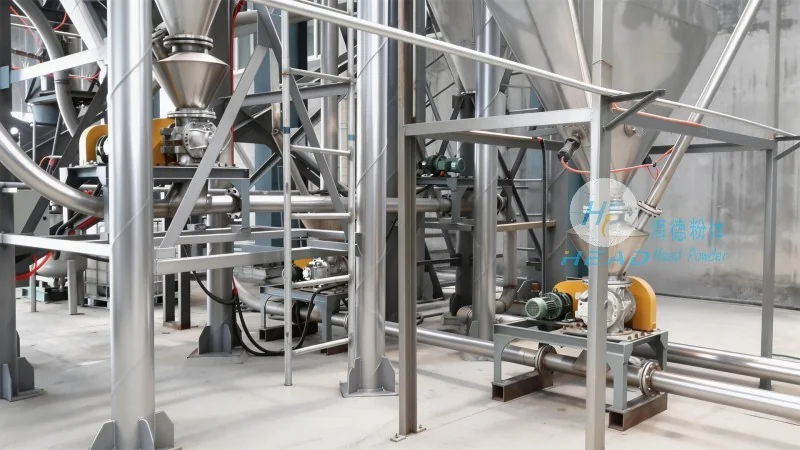
The company's commitment to quality and innovation has enabled it to serve a wide range of industries, from traditional coal mining to modern power generation and industrial applications. By leveraging cutting-edge engineering and robust manufacturing processes, headpowder ensures that its conveying systems are durable, reliable, and capable of withstanding the demanding conditions of coal handling operations. The company's team of experienced engineers and technicians work closely with clients to develop tailored solutions that enhance operational productivity and reduce maintenance costs.
Headpowder's facilities in Shandong are equipped with state-of-the-art technology and adhere to strict quality control standards. This enables the company to deliver high-performance conveying equipment that meets international standards while addressing the specific challenges of coal granular material transport. The company's focus on customer satisfaction and technical excellence has established it as a trusted partner in the industry, providing comprehensive support from system design to installation and maintenance.