

Design of Bentonite Pneumatic Conveying Equipment
Headpowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying systems tailored for bentonite transport. This article provides a detailed overview of the design considerations, technical specifications, and operational advantages of our specialized equipment, ensuring efficient and reliable material handling for industrial applications.
Key Design Considerations for Bentonite Pneumatic Conveying Systems
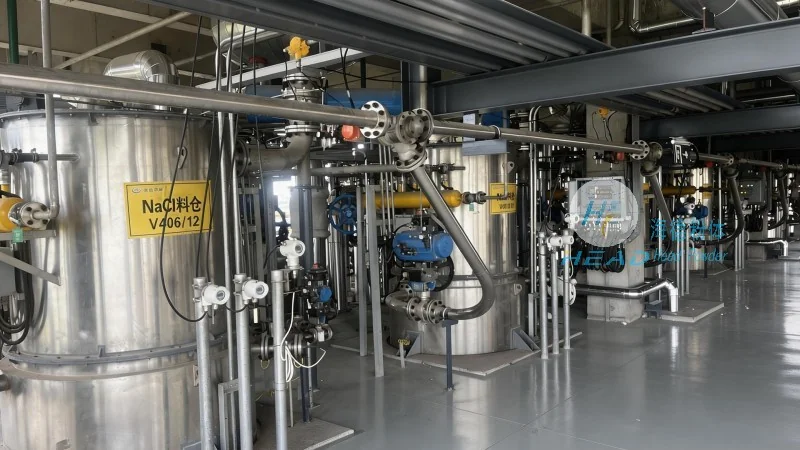
The design of a bentonite pneumatic conveying system involves several critical factors that directly impact its performance, efficiency, and longevity. First, the material properties of bentonite, such as its density, moisture content, and flowability, must be thoroughly analyzed. Bentonite is a fine, cohesive powder that can present challenges in terms of blockage and clogging if not handled properly. Our engineers conduct comprehensive material testing to determine the optimal air velocity, pressure, and system configuration. Additionally, the system's capacity requirements, including the desired throughput rate and distance of material transport, are carefully evaluated to ensure the design meets operational demands. The choice of equipment components, such as the air compressor, cyclone separator, and material feeders, is also a key design decision. We select high-quality, durable components from reputable manufacturers to guarantee long-term reliability and minimal maintenance.
System Components and Their Functions
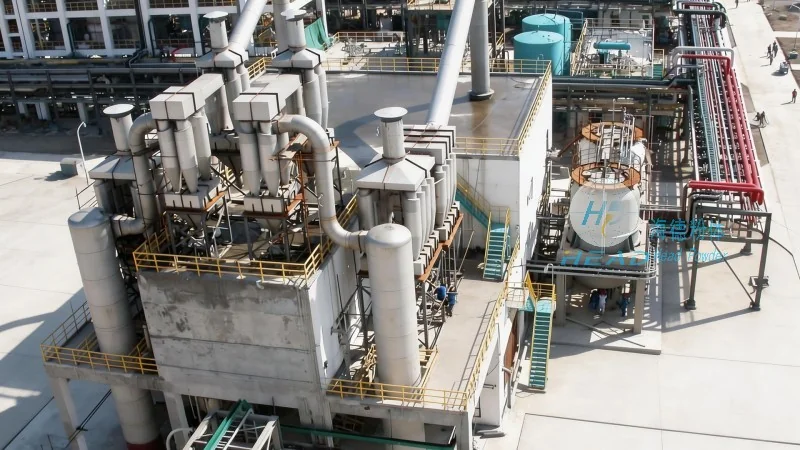
A typical bentonite pneumatic conveying system consists of several interconnected components that work in tandem to achieve efficient material transport. The primary components include a material hopper or silo for storage, a rotary valve or feeder to control the flow of bentonite into the system, an air compressor to generate the necessary pressure and airflow, a pipeline network to transport the material, a cyclone separator to separate the bentonite from the air, and a dust collection system to ensure environmental compliance. The material hopper is designed with a sloped bottom and a discharge valve to prevent material bridging and ensure smooth feeding. The rotary valve acts as a controlled gate, regulating the flow rate of bentonite into the pipeline. The air compressor provides the driving force, with pressure levels typically ranging from 5 to 15 bar, depending on the system's requirements. The pipeline is constructed from corrosion-resistant materials like stainless steel or PVC to withstand the abrasive nature of bentonite. The cyclone separator uses centrifugal force to separate the fine particles from the air stream, with the separated bentonite collected in a discharge bin. The dust collection system, often a baghouse or cartridge filter, captures any residual dust particles, ensuring clean air emissions and compliance with environmental regulations.
Advantages of Our Bentonite Pneumatic Conveying Solutions
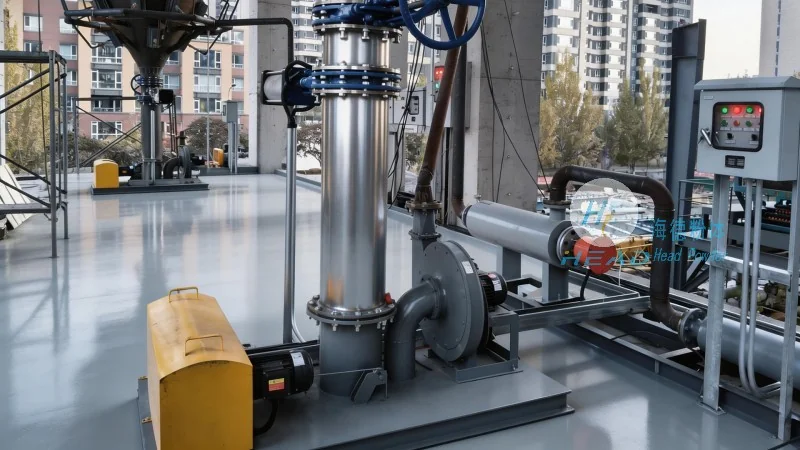
Implementing a pneumatic conveying system for bentonite offers numerous advantages over traditional mechanical conveying methods. First, it eliminates the need for moving parts in the material handling process, reducing maintenance costs and downtime. The absence of mechanical components also minimizes the risk of material contamination and damage. Additionally, pneumatic systems can handle high volumes of material over long distances with minimal energy consumption compared to other methods. The enclosed pipeline design prevents dust emissions, improving workplace safety and environmental sustainability. Our systems are also highly flexible, allowing for easy integration with existing production lines and future expansion. The automated control systems enable precise regulation of material flow, enhancing process consistency and reducing human error. Furthermore, the compact design of our equipment saves valuable floor space in industrial facilities, making it ideal for applications with limited installation area. The durability of the components, combined with regular maintenance protocols, ensures a long service life, providing a high return on investment for our clients.
Application Scenarios and Industry Use Cases
Bentonite pneumatic conveying systems are widely used in various industries where bentonite is a critical raw material. In the oil and gas sector, bentonite is used as a drilling fluid additive to maintain wellbore stability and prevent fluid loss. The pneumatic system efficiently transports bentonite from storage silos to the drilling site, ensuring a consistent supply of material. In the paper and pulp industry, bentonite is added to paper to improve its strength and water resistance. The system delivers the bentonite to the paper manufacturing process with precision, maintaining the required quality standards. The chemical industry utilizes bentonite as a catalyst or adsorbent in various processes, and our conveying systems ensure reliable transport of the material to reactors and processing units. Additionally, in the pharmaceutical and food industries, where bentonite is used as a filler or binder, the enclosed and sanitary design of our equipment meets stringent hygiene and safety requirements. The versatility of our pneumatic conveying solutions makes them suitable for a wide range of applications, from small-scale laboratory use to large-scale industrial production.
Customization and Engineering Support
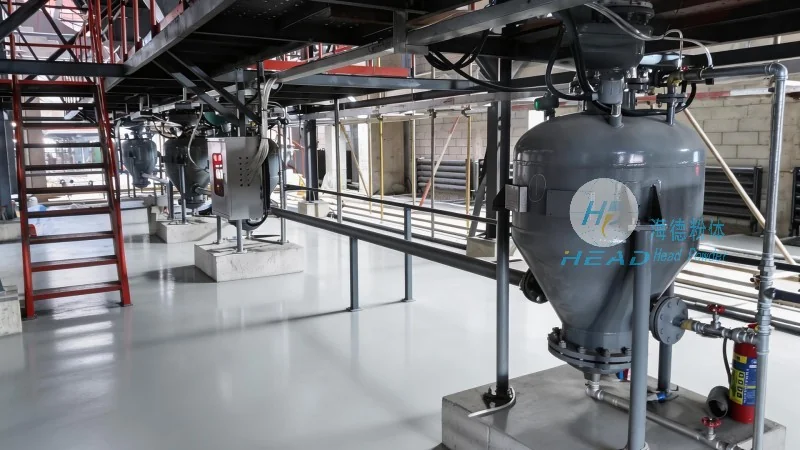
Headpowder understands that each industrial application has unique requirements, and we offer comprehensive customization options to meet specific client needs. Our engineering team works closely with clients to analyze their operational parameters, material characteristics, and space constraints to design a tailored pneumatic conveying system. We provide detailed engineering drawings, 3D models, and performance simulations to ensure the system meets all functional and safety requirements before installation. Our team of experienced engineers and technicians offers on-site installation, commissioning, and training services to ensure smooth integration and operation. We also provide long-term maintenance and support services, including regular inspections, component replacement, and troubleshooting assistance. Our commitment to quality and customer satisfaction is reflected in our ISO-certified manufacturing processes and adherence to international standards. By partnering with Headpowder, clients gain access to a reliable and efficient solution for bentonite transport, backed by our expertise and dedication to excellence.