

Design of Dust Pneumatic Conveying Equipment
At Shandong HeadPowder Engineering Co., Ltd., we specialize in the design and development of advanced dust pneumatic conveying systems tailored to meet the diverse needs of industrial applications. Our expertise lies in creating efficient, reliable, and cost-effective solutions for handling and transporting fine powders and dust materials. The design of such equipment is a critical process that involves meticulous consideration of material properties, operational requirements, and environmental factors to ensure optimal performance and safety.
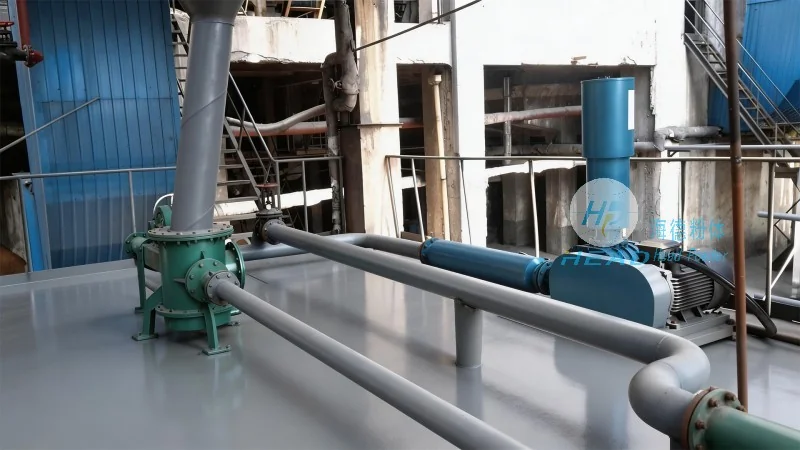
Key Design Considerations for Dust Pneumatic Conveying Systems
When designing a dust pneumatic conveying system, several key factors must be carefully evaluated to achieve the best results. First, the physical and chemical properties of the material being conveyed, such as particle size, density, moisture content, and abrasiveness, play a crucial role in determining the appropriate conveying method and equipment configuration. For example, fine powders with low bulk density may require high-pressure systems to maintain flow, while abrasive materials necessitate robust components to prevent wear and tear. Additionally, the distance and layout of the conveying line, including vertical and horizontal runs, impact the selection of blower type, pipeline diameter, and pressure requirements. Our team conducts thorough material analysis and process simulations to optimize these parameters, ensuring the system operates within safe and efficient limits.
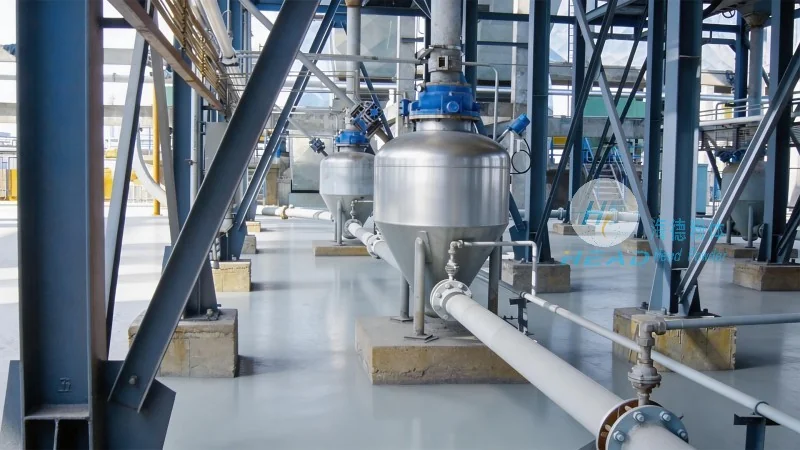
Components and Technologies in Dust Pneumatic Conveying Equipment
The core components of a dust pneumatic conveying system include the blower or compressor, conveying pipeline, material feeders, and control systems. The blower is responsible for generating the necessary airflow and pressure to move the material through the pipeline. We offer a range of blower types, including rotary lobe, centrifugal, and positive displacement blowers, each with specific advantages depending on the application. The pipeline design is critical for minimizing pressure drop and ensuring smooth material flow; we use high-quality materials like stainless steel or coated steel to withstand the abrasive nature of dust and prevent clogging. Material feeders, such as rotary valves or star feeders, regulate the flow rate and prevent backflow, while control systems monitor pressure, flow, and temperature to maintain system stability. Advanced technologies, such as variable frequency drives (VFDs) and real-time monitoring, enhance energy efficiency and operational reliability.
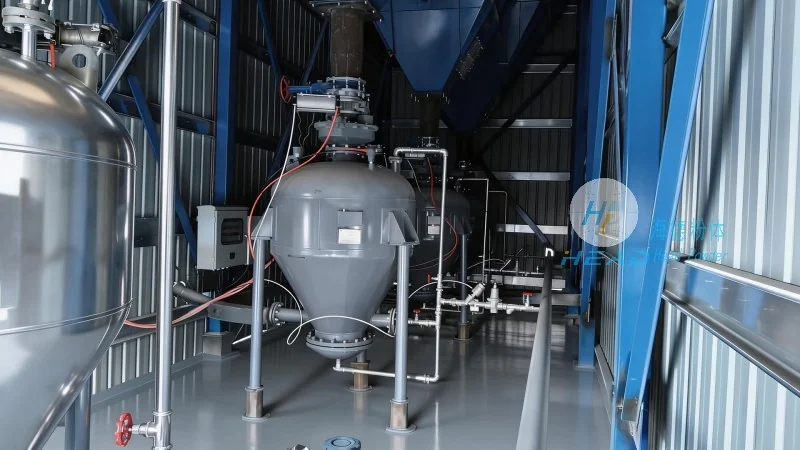
Application Examples and Performance Benefits
Dust pneumatic conveying equipment is widely used in various industries, including pharmaceuticals, food processing, chemical manufacturing, and mining. For instance, in the pharmaceutical industry, our systems are designed to handle sensitive powders with strict contamination control measures, ensuring compliance with regulatory standards. In the food sector, we provide hygienic and sanitary designs that meet food-grade requirements, with components made from food-safe materials and easy-to-clean surfaces. The performance benefits of our dust pneumatic conveying systems include improved material handling efficiency, reduced labor costs, and enhanced safety by eliminating manual handling of dust. Additionally, our designs minimize product degradation and contamination, preserving the quality of the conveyed materials. By optimizing the conveying process, we help our clients achieve higher throughput, lower energy consumption, and increased productivity.
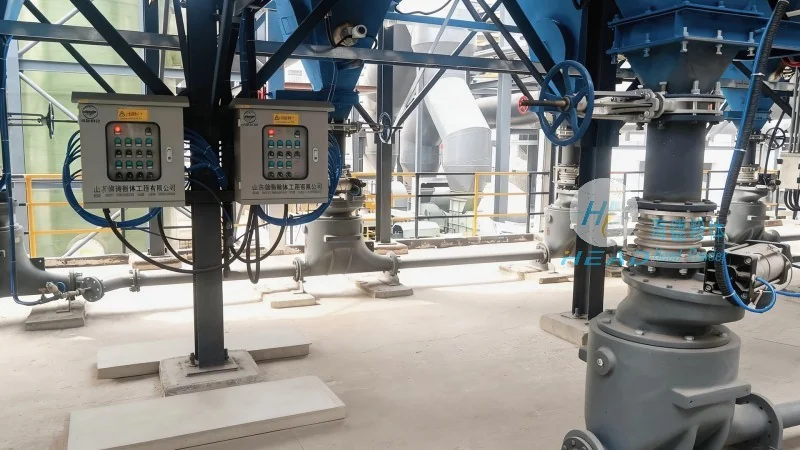
Customization and After-Sales Support
At Shandong HeadPowder Engineering Co., Ltd., we understand that each industrial application has unique requirements. Therefore, we offer customized dust pneumatic conveying solutions tailored to specific needs. Our engineering team works closely with clients to understand their process challenges and develop tailored designs that address their operational goals. We provide comprehensive after-sales support, including installation, commissioning, and maintenance services, to ensure the long-term performance and reliability of our equipment. Our commitment to quality and customer satisfaction has made us a trusted partner for many industries, providing reliable and efficient dust handling solutions.