

Principle and Working Scene Characteristics of Barley Powder Conveying Machines
Barley powder conveying machines are essential equipment in the processing and handling of barley-derived products. These specialized devices are designed to efficiently transport fine barley powder, a critical ingredient in various food and industrial applications. Understanding the fundamental principles and operational characteristics of such machines is vital for optimizing production processes and ensuring consistent quality in barley-based products.
The Working Principle of Barley Powder Conveying Machines
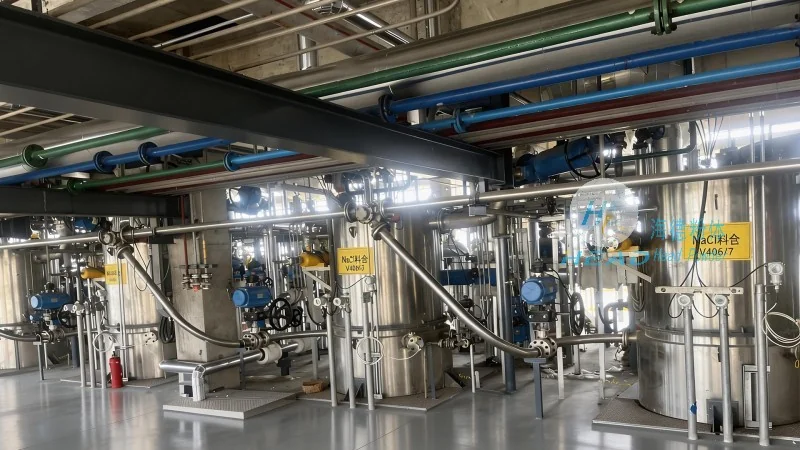
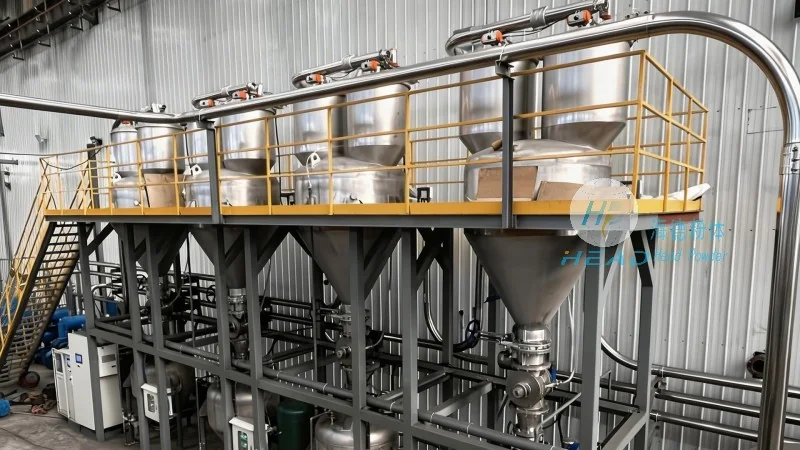
The core of barley powder conveying machines involves a sophisticated system that integrates mechanical and pneumatic components to facilitate the movement of barley powder. The primary mechanism operates by using a hopper to store the powder, followed by a series of valves and a conveying tube. As the powder is released from the hopper, it is drawn into the conveying tube through a pressure differential created by a fan or blower. This pressure difference ensures smooth and clog-free transportation, preserving the integrity of the barley particles.
Key components include the feeding hopper, designed to handle bulk quantities of barley powder, and the conveying system, which may use flexible hoses or rigid pipes. The fan or blower unit generates the necessary airflow to move the powder, while the control system allows precise regulation of the conveying rate. This combination ensures efficient and reliable operation, even when handling fine, powdery materials.
Working Scene Characteristics of Barley Powder Conveying Machines
The operational characteristics of barley powder conveying machines are tailored to meet diverse industrial demands. These machines are commonly employed in food processing facilities to streamline the production of barley-based products like flour, malt, and brewing ingredients. Their design enables easy integration into existing production lines, reducing downtime and boosting overall productivity.
Beyond food processing, barley powder conveying machines are utilized in industrial applications such as animal feed production and biofuel manufacturing. Their versatility makes them suitable for small-scale and large-scale industrial facilities alike. The ability to handle varying particle sizes and moisture contents of barley powder enhances adaptability in different working environments.
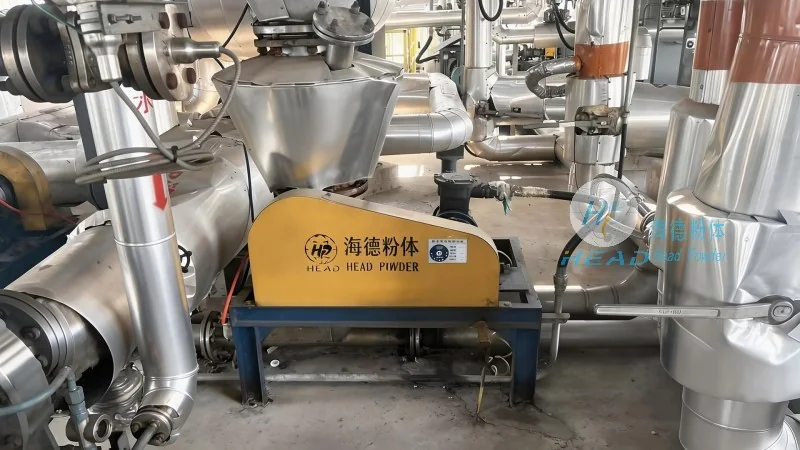
A key advantage is the minimized product contamination and loss during transportation. The enclosed conveying system prevents dust and particles from escaping, while smooth components reduce material buildup and clogging. This improves hygiene and extends equipment lifespan.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., known as HeadPowder, is a leading manufacturer of advanced powder handling equipment. With a focus on innovation and quality, HeadPowder serves clients in the food, pharmaceutical, and industrial sectors. The company’s headquarters is in Shandong, China, operating a state-of-the-art facility with cutting-edge technology and skilled personnel.
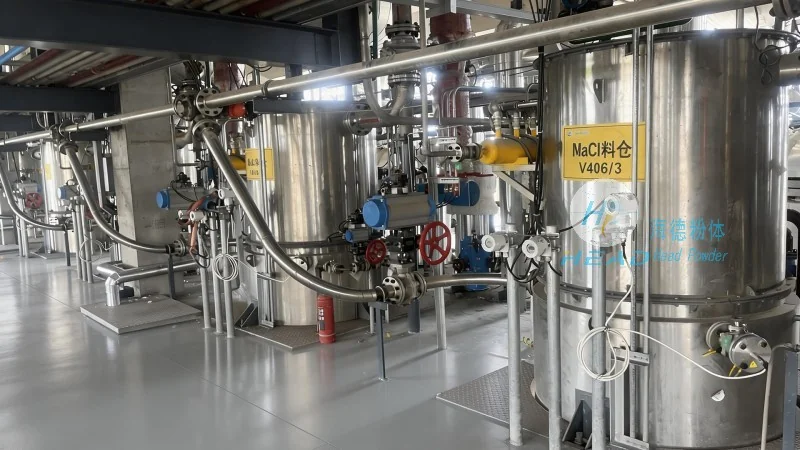
HeadPowder specializes in customizing powder conveying solutions to meet unique client needs. Engineers and technicians collaborate closely with customers to understand requirements and develop efficient, high-quality solutions. Leveraging industry experience, HeadPowder ensures products meet top performance and reliability standards.
HeadPowder’s commitment to customer satisfaction is reflected in comprehensive after-sales support, including technical assistance, maintenance, and repairs. This dedication has built a strong market reputation and long-term client relationships.