

Principle and Working Scene Characteristics of Aluminum Foil Powder Conveyors
Aluminum foil powder conveyors are specialized industrial equipment engineered for the efficient and safe transportation of aluminum foil powders across various applications. These systems are integral to material handling processes, ensuring consistent flow rates, maintaining product integrity, and enhancing operational efficiency in industries such as food processing, pharmaceuticals, and chemical manufacturing. The design of aluminum foil powder conveyors prioritizes factors like dust containment, material purity, and mechanical reliability, making them essential for handling fine or abrasive powders where quality and safety are non-negotiable.
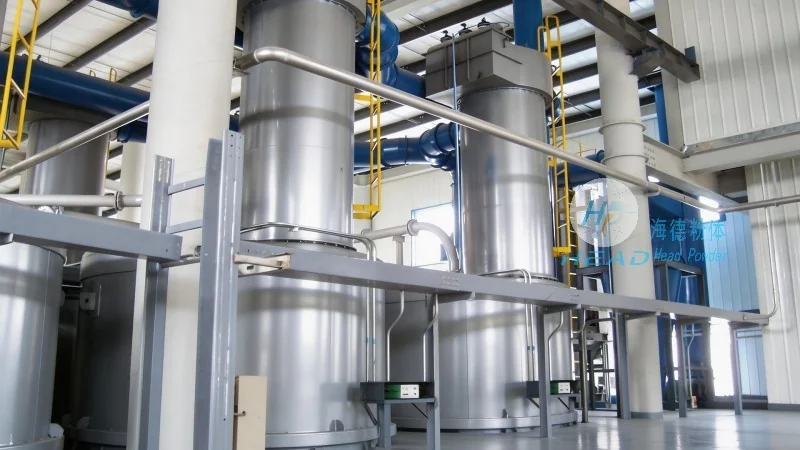
The Working Principle of Aluminum Foil Powder Conveyors
The core operation of aluminum foil powder conveyors relies on either positive displacement or pneumatic mechanisms to move powders through a sealed or semi-sealed system. Positive displacement conveyors, typically featuring rotary lobe or screw designs, compress the material in discrete increments, ensuring a steady and controlled flow. This method is ideal for powders with high density or those prone to caking, as it prevents material backflow and maintains uniform transport. Pneumatic conveyors, on the other hand, utilize air pressure to propel powders through a network of pipes, making them suitable for lighter or more delicate powders. The choice between these systems depends on the powder's properties, required flow rate, and the distance of material transport. Both designs incorporate air filtration and material containment to minimize dust emissions and maintain a clean working environment, aligning with industrial hygiene standards.
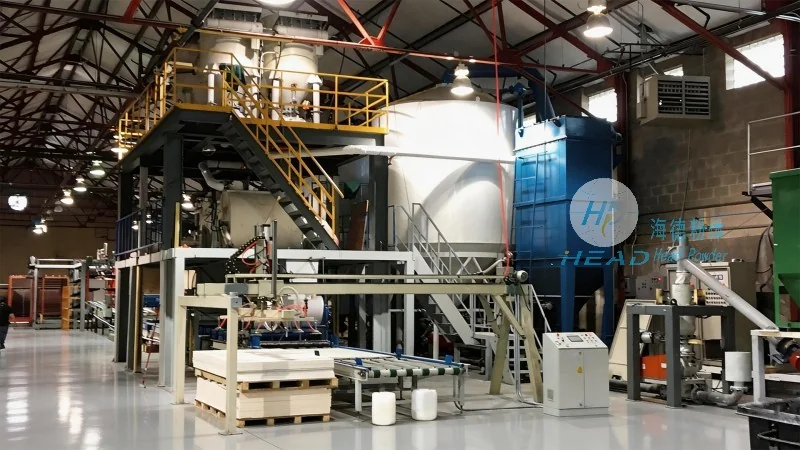
Key Working Scene Characteristics of Aluminum Foil Powder Conveyors
Aluminum foil powder conveyors are tailored to meet the diverse demands of different industrial settings, each with unique characteristics that define their performance and suitability. In food processing facilities, these conveyors are constructed from stainless steel and designed with easy-to-clean components to adhere to strict hygiene regulations. This ensures that the conveyed aluminum foil powders remain free from contamination, which is critical for products like food additives or packaging materials. The working scene characteristics also include the ability to handle varying particle sizes and densities, as aluminum foil powders can range from fine, powdery forms to coarser, granular materials. Adjustable speed controls and flow meters are integrated to maintain precise material handling, which is vital for processes such as blending and packaging. Additionally, the systems are engineered to minimize product degradation, preserving the physical and chemical properties of the aluminum foil powders during transport. This is particularly important in applications where the powder's quality directly impacts the final product's quality, such as in the production of aluminum-based coatings or additives.
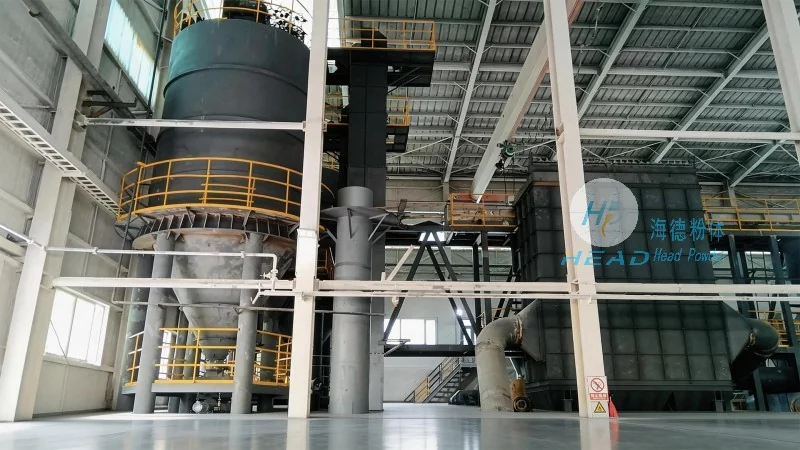
Application Scenarios in Industrial Settings
HeadPowder, a leading manufacturer of material handling equipment, provides aluminum foil powder conveyors that are widely utilized across various industrial sectors. In the pharmaceutical industry, these conveyors are employed to transport aluminum foil powders used in the production of tablets and capsules, where precision and cleanliness are paramount. The systems are designed to prevent cross-contamination and maintain sterile conditions, ensuring compliance with stringent regulatory requirements. In the chemical manufacturing sector, aluminum foil powder conveyors are utilized for handling reactive or hazardous powders, where the sealed design and robust construction of the equipment are essential for safety. Features like explosion-proof components and pressure relief valves mitigate risks associated with volatile materials. Furthermore, in the food and beverage industry, these systems are used to transport aluminum foil powders used in food packaging, where the equipment's ability to handle hygienic and non-stick surfaces is crucial. The working scene characteristics, such as low maintenance requirements and easy cleaning, make these conveyors ideal for high-volume production environments.
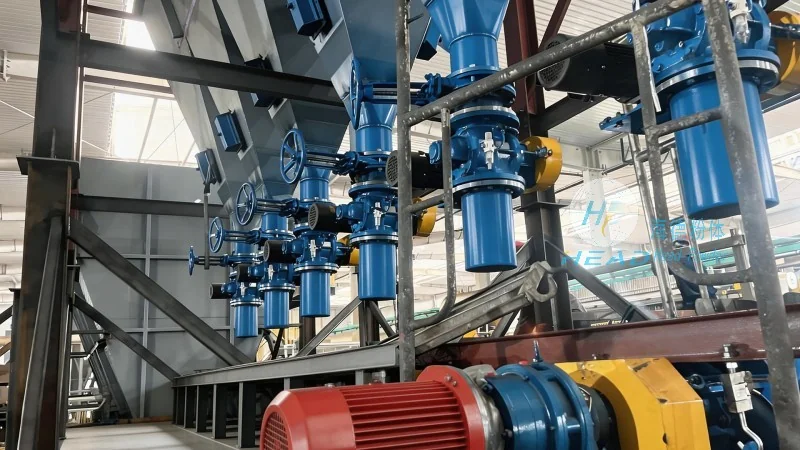
Advantages and Performance Metrics
Aluminum foil powder conveyors from Shandong HeadPowder Engineering Co., Ltd. offer several advantages that enhance operational efficiency and product quality. One primary benefit is the ability to maintain a consistent flow rate, which is critical for processes requiring precise material control. The positive displacement design ensures controlled material movement, reducing the risk of clogging or uneven distribution. Another advantage is the equipment's durability and longevity, constructed from high-quality materials to withstand continuous operation. The systems are also designed for low maintenance, with replaceable parts and easy access for servicing, minimizing downtime and operational costs. Performance metrics, such as capacity and efficiency, are optimized for each application. For example, the conveyor's capacity can be adjusted based on the powder's density and particle size, ensuring peak efficiency. Additionally, monitoring features like flow sensors and pressure gauges allow real-time performance tracking and adjustments.