

Principle and Working Scene Characteristics of Pneumatic Conveying for Rice Grains
For rice processing facilities, the efficient and reliable transport of rice grains is crucial to maintaining quality and operational efficiency. Pneumatic conveying systems have emerged as a preferred solution, offering a clean, dust-free method to move rice from storage to processing stages. This article explores the fundamental principles behind pneumatic conveying for rice grains and highlights the key working scene characteristics that make it an ideal choice for various applications.
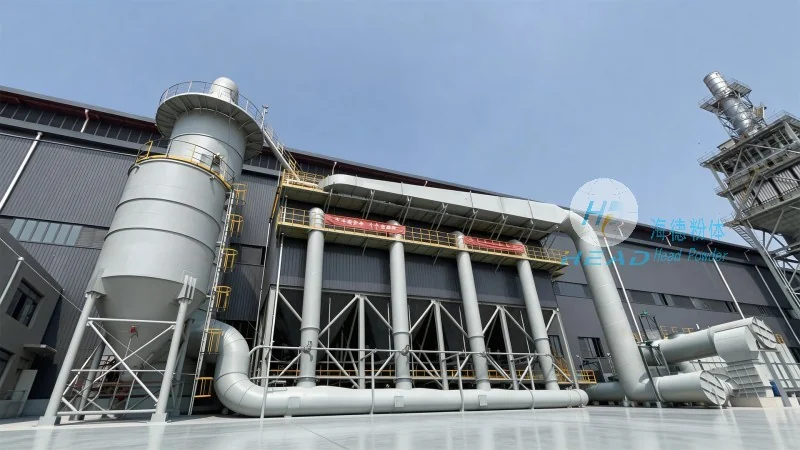
The Fundamental Principle of Pneumatic Conveying in Rice Processing
Pneumatic conveying operates by using a stream of air to transport solid particles, such as rice grains, through a pipeline. The process typically involves creating a pressure differential—either positive or negative—within the system. In positive pressure systems, air is forced into the conveying line, carrying the rice grains along with it. Negative pressure systems, on the other hand, draw air and particles into the line using a vacuum. For rice grains, which are relatively light and have a consistent size, the positive pressure method is often preferred due to its ability to handle larger volumes and minimize particle degradation. The key to effective pneumatic conveying lies in controlling the air velocity and pressure to ensure that rice grains are transported without breakage or segregation. This requires precise engineering to match the specific characteristics of rice, including its density, moisture content, and flowability.
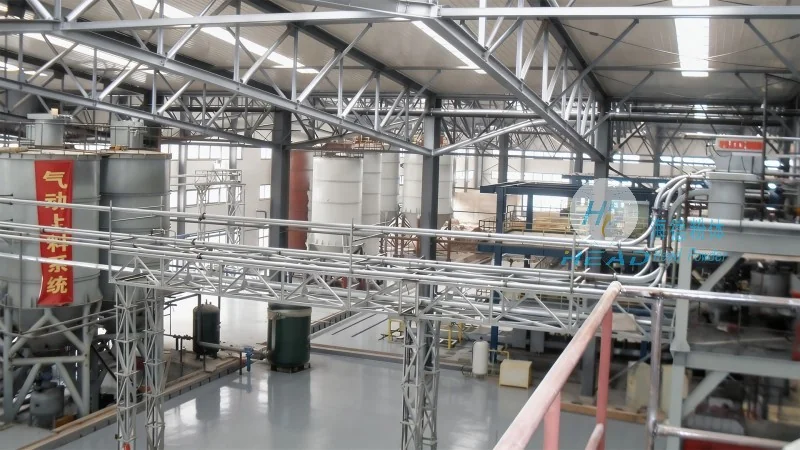
Key Working Scene Characteristics and Applications
The working scene characteristics of pneumatic conveying for rice grains are tailored to meet the demands of different operational environments. In warehouse settings, for example, pneumatic systems are used to transfer rice from bulk storage silos to processing lines, ensuring a continuous flow without the need for manual handling. This is particularly beneficial in large-scale operations where manual labor is costly and inefficient. In processing plants, the system can be integrated into the production line to move rice from cleaning and sorting stages to milling or packaging. The flexibility of pneumatic conveying allows it to adapt to various layouts, making it suitable for both new installations and retrofits in existing facilities. Additionally, the system can be designed to handle different types of rice, including raw grains, milled rice, and even rice with additives, providing versatility in diverse production scenarios.
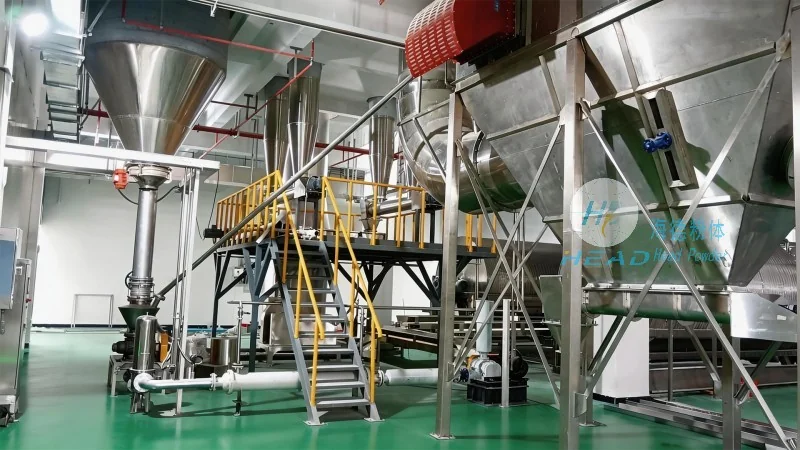
Technical Advantages in Handling Rice Grains
When compared to traditional methods like belt conveyors or bucket elevators, pneumatic conveying offers several advantages for rice grain handling. One of the most significant benefits is the reduction of dust and contamination, which is critical for maintaining the quality of rice products. Unlike mechanical systems that can generate dust through friction or impact, pneumatic systems keep the rice grains enclosed within the pipeline, minimizing exposure to the environment. This not only improves product quality but also enhances workplace safety by reducing the risk of respiratory issues associated with dust inhalation. Another advantage is the ability to handle delicate rice grains without causing breakage or damage. The controlled air flow and gentle transport mechanism prevent the rice from being crushed or broken, preserving its texture and nutritional value. Furthermore, pneumatic conveying systems are energy-efficient, as they use less power to move the same volume of rice compared to mechanical systems. This leads to lower operational costs and a reduced environmental footprint, making it an environmentally friendly choice for rice processing facilities.
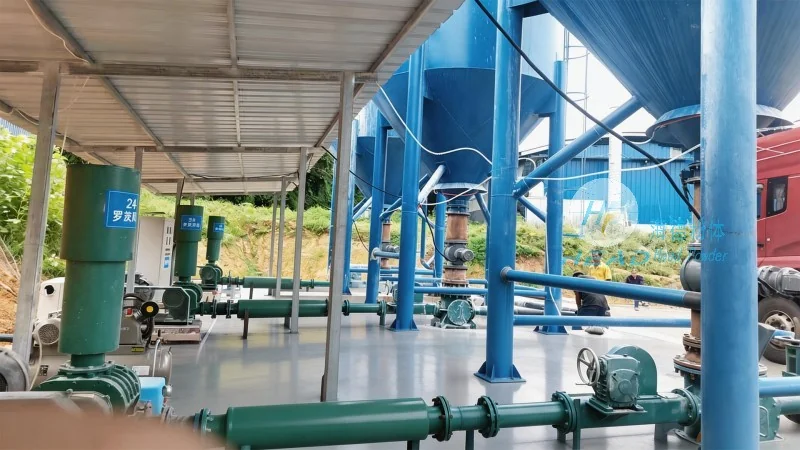
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of pneumatic conveying solutions tailored for the rice processing industry. With headquarters in Shandong, China, the company specializes in designing, manufacturing, and installing advanced pneumatic systems that meet the unique needs of rice grain handling. HeadPowder's expertise lies in understanding the specific challenges of rice processing, such as the need for dust-free transport and the preservation of grain quality. The company's team of engineers and technicians work closely with clients to develop customized solutions that optimize operational efficiency and reduce costs. By leveraging years of experience in the industry, HeadPowder ensures that its pneumatic conveying systems are reliable, durable, and compliant with industry standards. The company's commitment to quality and customer satisfaction has made it a trusted partner for rice processing facilities worldwide.