

Working Principle and Features of Multi-functional Powder Pneumatic Conveying Systems
HeadPowder, a leading provider of advanced material handling solutions, specializes in multi-functional powder pneumatic conveying systems. These systems are designed to efficiently transport bulk powders and granules over long distances with minimal maintenance and operational costs. The core technology behind these systems leverages the principles of pneumatic conveying, where air or gas is used as the medium to move material through a pipeline network.
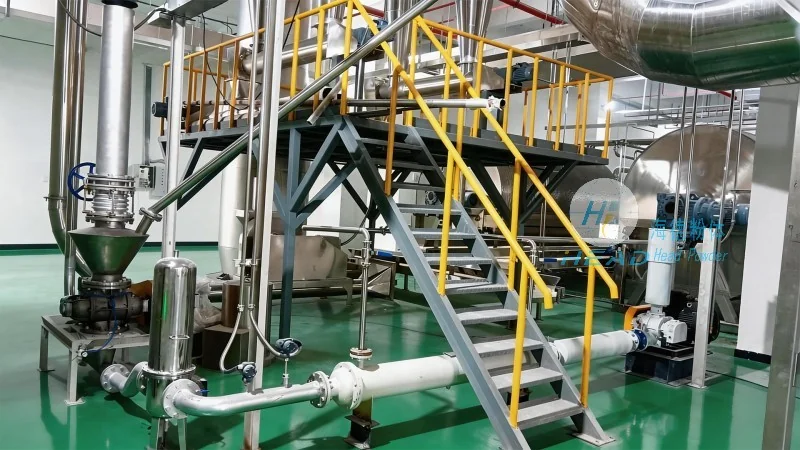
Working Principle of Multi-functional Powder Pneumatic Conveying
The operation of a multi-functional powder pneumatic conveying system begins with the material being fed into a hopper or feeder. From there, the material is introduced into a pipeline where it is entrained by a high-velocity air stream. The air velocity is carefully controlled to ensure that the powder particles are fully suspended and transported through the system without clogging or degradation. The system typically includes components such as a blower or compressor to generate the necessary air pressure, a filter to remove dust from the exhaust air, and a receiver or silo to collect the conveyed material at the destination. The design of these systems allows for flexibility in handling various types of powders, including fine powders, coarse powders, and even abrasive materials, making them suitable for a wide range of industrial applications.
Key Features and Advantages
Multi-functional powder pneumatic conveying systems offer several distinct advantages that make them an attractive choice for many industries. One of the primary features is their ability to handle a wide variety of powder characteristics, from low to high density, and from non-abrasive to highly abrasive materials. This versatility is achieved through adjustable air velocity and pressure settings, which can be customized to match the specific properties of the material being conveyed. Another key feature is the system's compact design, which reduces the footprint required for installation and operation, making it suitable for both new and retrofit applications. Additionally, these systems are known for their low maintenance requirements, as they have fewer moving parts compared to mechanical conveying systems, leading to lower operational costs and increased reliability over time.
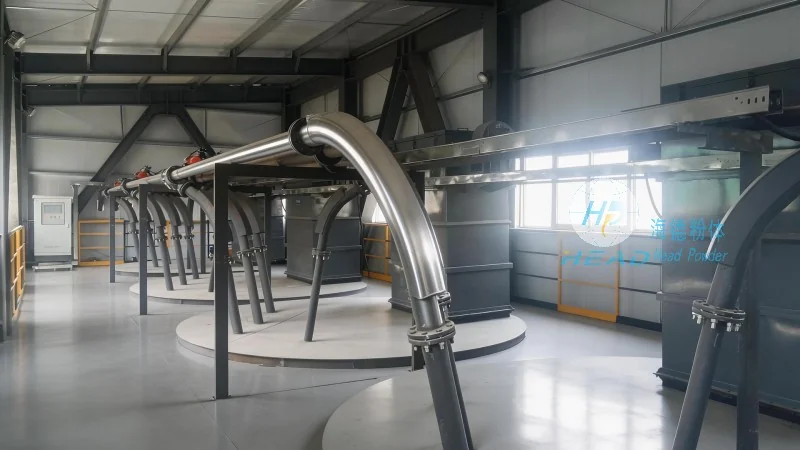
Applications in Industrial Settings
HeadPowder's multi-functional powder pneumatic conveying systems are widely used in various industrial sectors, including pharmaceuticals, food processing, chemical manufacturing, and mining. In the pharmaceutical industry, for example, these systems are employed to transport active pharmaceutical ingredients (APIs) and excipients with strict contamination control measures. The enclosed nature of the system ensures that the materials remain sterile and free from external contaminants, which is critical for maintaining product quality and compliance with regulatory standards. In the food industry, the systems are used to handle powders like flour, sugar, and spices, where hygiene and product integrity are paramount. The ability to maintain a clean and dust-free environment helps prevent cross-contamination and ensures that the final products meet safety and quality standards. In chemical manufacturing, these systems are utilized to convey raw materials and intermediates, often in hazardous environments, where the enclosed design protects workers from exposure to toxic or reactive substances. The system's ability to handle abrasive materials without significant wear and tear on components is particularly beneficial in such applications.
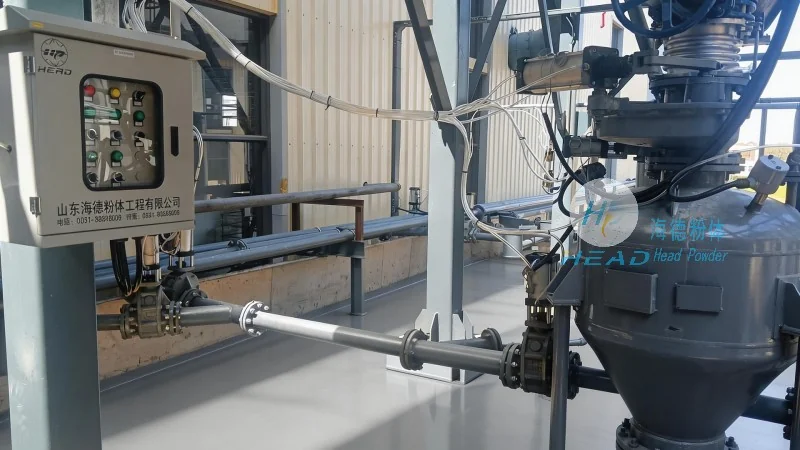
Customization and Integration
HeadPowder understands that each industrial application has unique requirements, and therefore, offers customized solutions tailored to specific needs. The company's engineers work closely with clients to design systems that meet their operational goals, including the required conveying capacity, distance, and material characteristics. Customization options may include different types of hoppers and feeders, adjustable air pressure and velocity controls, and specialized filters or receivers. Additionally, the systems can be integrated with existing production lines or new facilities, ensuring seamless operation and minimal disruption to production schedules. The company's commitment to quality and innovation is reflected in its use of advanced materials and components, which enhance the durability and performance of the conveying systems.
Conclusion and Company Information
Multi-functional powder pneumatic conveying systems represent a sophisticated and efficient solution for material handling in modern industrial operations. HeadPowder Engineering Co., Ltd., based in Shandong, China, is a trusted provider of these systems, offering reliable, versatile, and cost-effective solutions for a wide range of powder transport needs. By leveraging advanced pneumatic conveying technology and customized design, HeadPowder helps industries improve their operational efficiency, reduce costs, and maintain product quality. The company's focus on customer satisfaction and technical excellence ensures that clients receive systems that not only meet their current requirements but also adapt to future growth and technological advancements.