

Working Principle and Features of Activated Carbon Pneumatic Conveying System Equipment
Shandong HeadPowder Engineering Co., Ltd., a professional manufacturer based in China, specializes in the design, development, and production of advanced activated carbon pneumatic conveying systems. This equipment is widely used in various industrial sectors, particularly in processes requiring efficient material handling and transportation of activated carbon. The following sections will delve into the working principle and key features of such systems, providing a comprehensive understanding for potential users and industry professionals.

Working Principle of Activated Carbon Pneumatic Conveying Systems
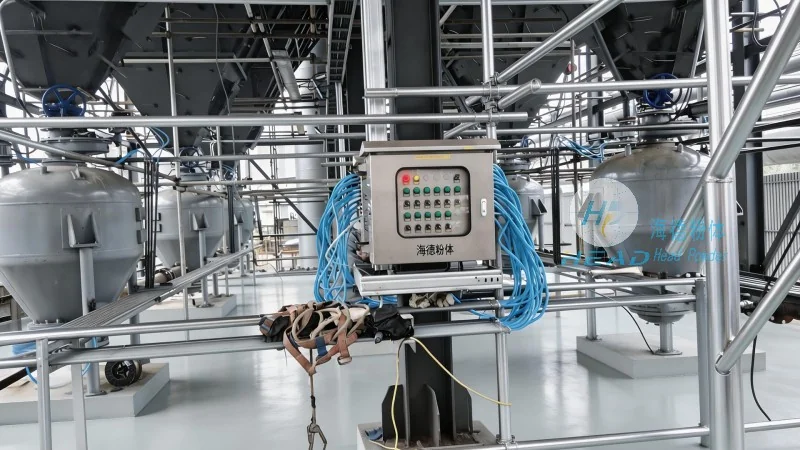
The activated carbon pneumatic conveying system operates on the principle of air flow to transport bulk materials. At its core, the system utilizes a combination of positive and negative pressure or vacuum to move activated carbon particles from a source to a destination. The process typically involves several key components, including a hopper, a feeder, a pipeline, and a receiver. The hopper stores the activated carbon, while the feeder ensures a consistent flow of material into the pipeline. Air is then introduced into the system, either by a blower or a vacuum pump, creating a flow that propels the carbon particles through the pipeline. The receiver collects the material at the end of the conveying line. This method eliminates the need for mechanical components like conveyors or belts, reducing maintenance and increasing operational efficiency.
Key Features of Activated Carbon Pneumatic Conveying Equipment
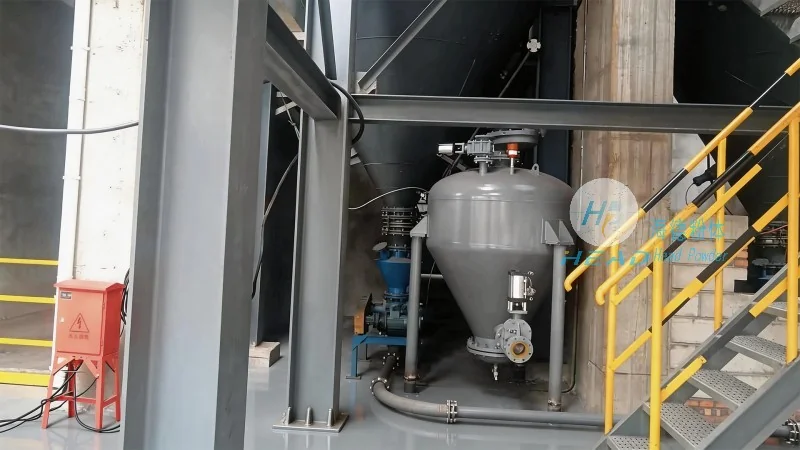
Activated carbon pneumatic conveying systems from Shandong HeadPowder Engineering Co., Ltd. are designed with several distinct features that enhance performance and reliability. Firstly, the system offers high conveying efficiency, capable of transporting large volumes of activated carbon over significant distances with minimal loss. This is achieved through optimized air flow and pipeline design, ensuring that the material moves smoothly without clogging or degradation. Secondly, the equipment is highly flexible in terms of layout and integration. It can be adapted to various industrial settings, accommodating different plant layouts and operational requirements. The modular design allows for easy installation and maintenance, reducing downtime and operational costs. Thirdly, the system provides excellent material handling capabilities, particularly for activated carbon, which is often delicate and prone to dust or attrition. The use of air as the conveying medium minimizes material degradation, preserving the quality of the activated carbon. Additionally, the system is equipped with advanced control systems that monitor and regulate the conveying process, ensuring consistent performance and safety. These features make the activated carbon pneumatic conveying system a reliable and efficient solution for industrial applications.
Applications and Benefits in Industrial Settings
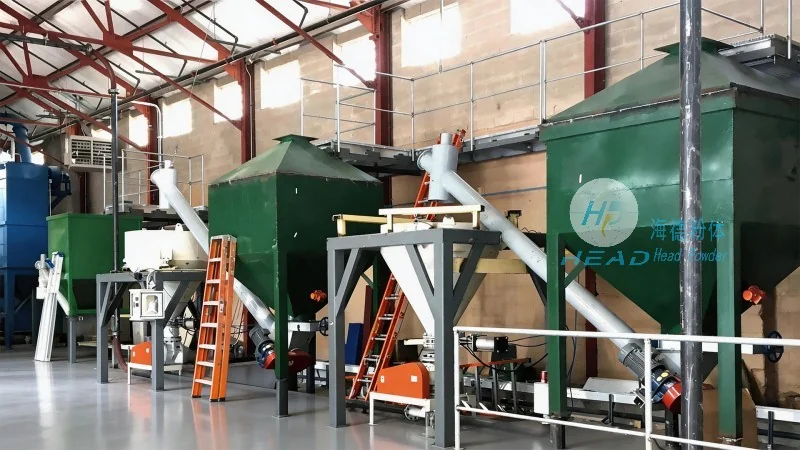
The activated carbon pneumatic conveying system is widely applied in industries such as water treatment, air purification, and chemical processing, where activated carbon is used for adsorption and filtration. In water treatment plants, the system efficiently transports activated carbon to and from filters, ensuring optimal filtration performance. In air purification systems, it moves activated carbon to and from adsorption units, maintaining the efficiency of air cleaning processes. The benefits of using this system include improved operational efficiency, reduced labor costs, and enhanced product quality. By eliminating manual handling and mechanical conveyors, the system minimizes the risk of contamination and material loss. Furthermore, the system's ability to handle large volumes of material reduces the need for frequent replenishment, leading to cost savings over time. The reliability of the system also contributes to increased plant uptime, as it requires less maintenance and has fewer points of failure compared to traditional conveying methods.