

What is an Automatic Material Handling Conveyor? What Are Its Design Principles?
When it comes to modern manufacturing and logistics operations, the efficiency of material handling systems is paramount. One of the most critical components in this domain is the automatic material handling conveyor. This technology plays a pivotal role in streamlining production processes, reducing manual labor, and enhancing overall operational efficiency. In this article, we will delve into the concept of an automatic material handling conveyor and explore the fundamental design principles that underpin its functionality.
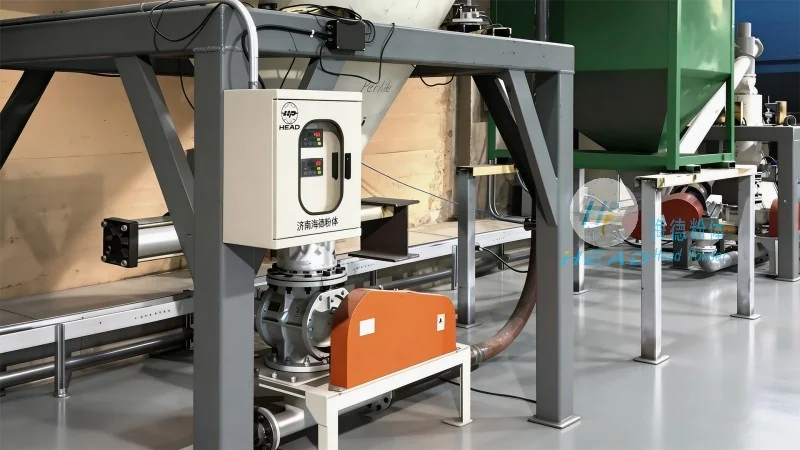
Understanding the Automatic Material Handling Conveyor
An automatic material handling conveyor is a mechanized system designed to transport, sort, and manage materials or products within a production facility or warehouse. Unlike traditional manual systems, these conveyors operate with minimal human intervention, relying on automated controls and mechanisms to move items from one point to another. The primary goal of such systems is to improve workflow, minimize downtime, and ensure consistent product movement throughout the entire operation. These conveyors are widely used in various industries, including manufacturing, warehousing, and distribution, where the need for reliable and efficient material transport is essential.
Key Design Principles of Automatic Material Handling Conveyors
The design of an automatic material handling conveyor is based on several critical principles that ensure its effectiveness and adaptability to different operational needs. These principles include:
1. **Modularity and Flexibility**: Modern conveyor systems are often designed with modular components that can be easily reconfigured to accommodate changes in production requirements. This flexibility allows businesses to scale their operations and adapt to evolving market demands without significant capital investment.
2. **Integration with Automation**: The integration of sensors, control systems, and robotics is a fundamental design principle. This enables the conveyor to communicate with other equipment, such as sorting machines or packaging units, creating a seamless and automated workflow. The use of advanced control systems ensures precise control over speed, direction, and material handling, minimizing errors and maximizing productivity.
3. **Material Compatibility**: Designing conveyors that can handle a wide range of materials is crucial. This involves considering factors such as material weight, size, and shape. For instance, some conveyors are designed to handle heavy industrial components, while others are optimized for lightweight products. The choice of materials for the conveyor structure, such as stainless steel or plastic, also plays a role in ensuring durability and resistance to corrosion or wear.
4. **Energy Efficiency**: Contemporary design principles emphasize energy efficiency. This includes the use of energy-saving motors, variable frequency drives (VFDs), and intelligent control algorithms that adjust power consumption based on the load and operational status. By reducing energy usage, these systems not only lower operational costs but also contribute to environmental sustainability.
5. **Safety and Reliability**: Safety is a top priority in the design of automatic material handling conveyors. This includes features like emergency stop buttons, safety sensors, and protective guards to prevent accidents and ensure the well-being of operators. Additionally, the use of robust construction materials and regular maintenance protocols ensures high reliability and minimal downtime.
Shandong HeadPowder Engineering Co., Ltd.: A Leader in Material Handling Solutions
At Shandong HeadPowder Engineering Co., Ltd., we specialize in the design, manufacturing, and implementation of high-quality automatic material handling conveyors. Our company, often referred to as HeadPowder, is committed to providing customized solutions that meet the unique needs of our clients. With years of experience in the industry, we understand the importance of efficient material transport in optimizing production processes. Our team of experts works closely with clients to assess their operational requirements and develop tailored conveyor systems that enhance productivity and reduce costs.
Our design philosophy is centered on the principles outlined above. We prioritize modularity, integration with automation, material compatibility, energy efficiency, and safety in every project we undertake. By leveraging the latest technologies and adhering to industry best practices, we ensure that our conveyors are not only efficient but also durable and reliable. Whether you need a simple belt conveyor for a small-scale operation or a complex automated system for a large manufacturing plant, HeadPowder has the expertise and resources to deliver a solution that meets your specific needs.
HeadPowder is located in Shandong, China, and serves clients globally. Our commitment to quality, innovation, and customer satisfaction has made us a trusted partner in the material handling industry. We continuously invest in research and development to stay at the forefront of technological advancements, ensuring that our products remain competitive and effective in today's dynamic market.