

What is a Small Bag Quantitative Weighing Pneumatic Conveying System Equipment? What Are Its Design
Small bag quantitative weighing pneumatic conveying systems represent a specialized class of industrial equipment designed to handle bulk materials in a precise and efficient manner. These systems are particularly valuable in industries where accurate measurement and controlled transport of powders or granules are critical, such as pharmaceuticals, food processing, and chemical manufacturing.
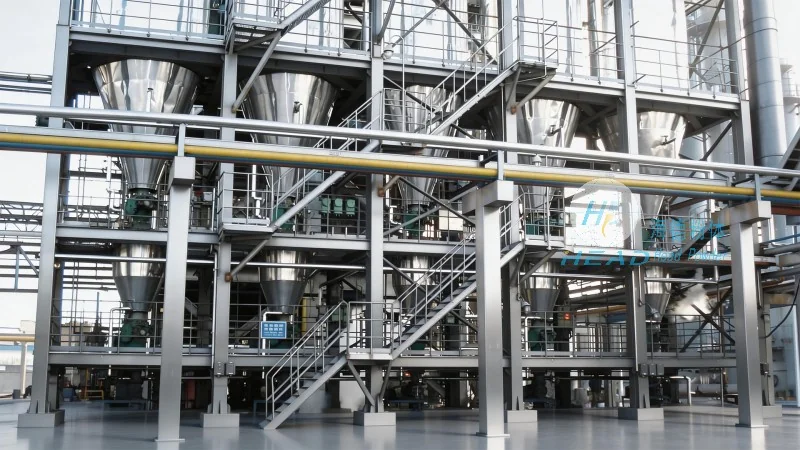
Key Components and Functionality
The core components of a small bag quantitative weighing pneumatic conveying system typically include a hopper for material storage, a weighing scale to ensure precise measurement, a pneumatic conveying line to transport the material, and a control system to regulate the entire process. The hopper is equipped with a feeder that can be adjusted to control the flow rate of material into the weighing scale. Once the desired weight is achieved, the material is released into the conveying line, which uses compressed air to move the material to the destination. The control system monitors all parameters, including weight, flow rate, and air pressure, to maintain consistent performance and prevent overfilling or underfilling.
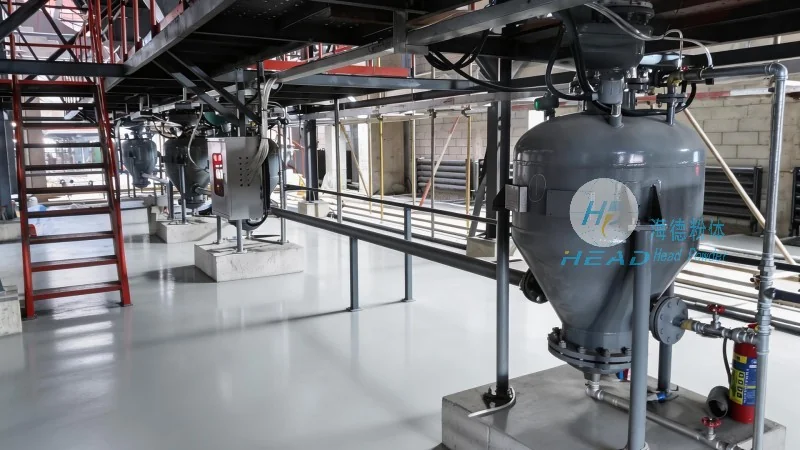
Design Principles and Operational Mechanics
The design of these systems is guided by several key principles to ensure accuracy and reliability. One fundamental principle is the integration of a high-precision weighing scale with a controlled feeding mechanism. This combination allows for the exact measurement of material quantities, which is essential for applications requiring strict compliance with regulations or quality standards. Another critical principle is the use of a pneumatic conveying system, which minimizes material degradation and contamination compared to mechanical systems. The system operates by creating a pressure differential between the hopper and the discharge point, using compressed air to draw the material through the pipeline. The control system adjusts the air flow and feeding rate in real-time to maintain the desired weight and flow rate, ensuring consistent performance across different material types and operating conditions.
Application Scenarios and Benefits
Small bag quantitative weighing pneumatic conveying systems are widely used in various industrial applications. In the pharmaceutical industry, they are used to transport active pharmaceutical ingredients (APIs) and excipients with high precision, ensuring that each batch meets stringent quality and dosage requirements. In food processing, these systems are employed to handle ingredients like sugar, flour, and spices, maintaining product purity and consistency. In chemical manufacturing, they are used to transport raw materials and intermediates, reducing the risk of cross-contamination and improving process efficiency. The primary benefits of these systems include improved accuracy in material measurement, reduced labor costs due to automated operation, and enhanced safety by minimizing human exposure to bulk materials. Additionally, the pneumatic conveying aspect reduces material degradation, which is crucial for sensitive products.
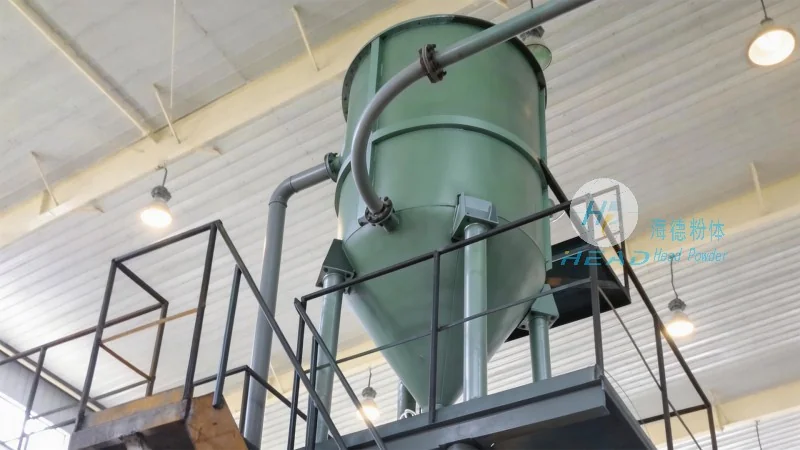
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer and supplier of industrial conveying systems, including small bag quantitative weighing pneumatic conveying equipment. The company is headquartered in Shandong, China, and has established a strong reputation for delivering high-quality, reliable, and efficient solutions tailored to the needs of various industries. With a focus on innovation and customer satisfaction, HeadPowder has developed advanced technologies to enhance the performance and durability of its products. The company's team of experienced engineers and technicians ensures that each system is designed and manufactured to meet the specific requirements of clients, providing customized solutions that improve operational efficiency and product quality.