

What is Sodium Bicarbonate Pneumatic Conveying? An Introduction to the Working Principle of Powder H
Sodium bicarbonate, commonly known as baking soda, is a widely used chemical in various industries, including food processing, pharmaceuticals, and manufacturing. The efficient and safe transportation of this fine powder is crucial for maintaining product quality and operational efficiency. Pneumatic conveying systems have emerged as a reliable solution for handling sodium bicarbonate, offering advantages such as reduced dust, improved safety, and enhanced process control. This article delves into the working principles of these systems, focusing on how they effectively transport sodium bicarbonate from one location to another.
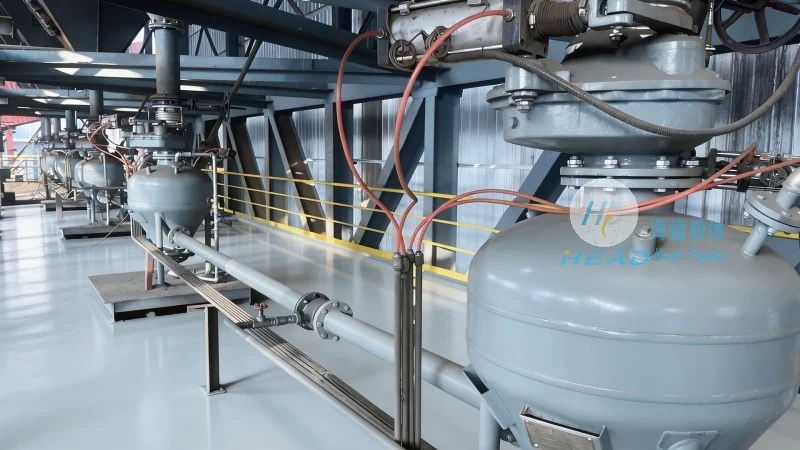
HeadPowder: A Leading Provider of Powder Handling Solutions
Shandong HeadPowder Engineering Co., Ltd., a prominent player in the powder handling industry, specializes in designing and manufacturing advanced pneumatic conveying systems tailored to the needs of various applications. With a strong commitment to quality and innovation, HeadPowder has established itself as a trusted partner for businesses seeking efficient and reliable solutions for transporting fine powders like sodium bicarbonate. The company’s expertise lies in understanding the unique challenges associated with handling such materials and developing customized systems that meet specific operational requirements.
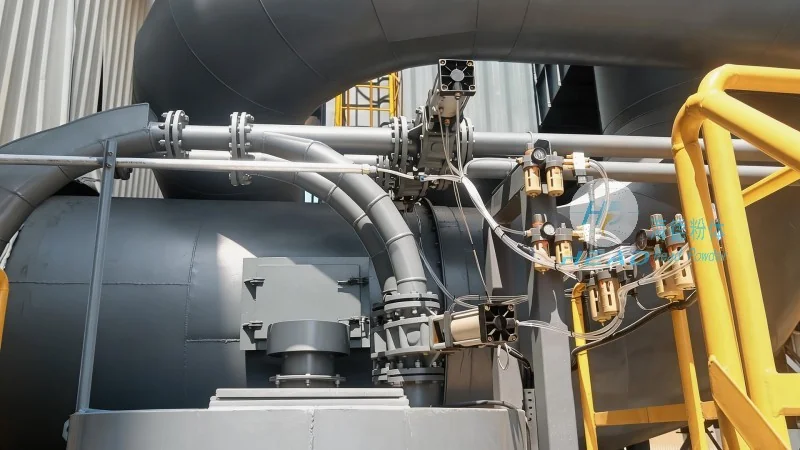
The Working Principle of Pneumatic Conveying Systems for Sodium Bicarbonate
Pneumatic conveying systems operate by using compressed air or other gases to transport bulk materials through a pipeline. In the case of sodium bicarbonate, the system typically consists of several key components, including a hopper for material storage, a conveyor line, and a receiver for the discharged material. The process begins with the material being fed from the hopper into the conveyor line. Compressed air is then introduced into the line, creating a flow that carries the powder particles forward. The velocity of the air is carefully controlled to ensure that the powder is transported without causing excessive wear or degradation. This method allows for the smooth and continuous movement of sodium bicarbonate, minimizing the risk of clogging or blockages that can occur with traditional mechanical conveyors.
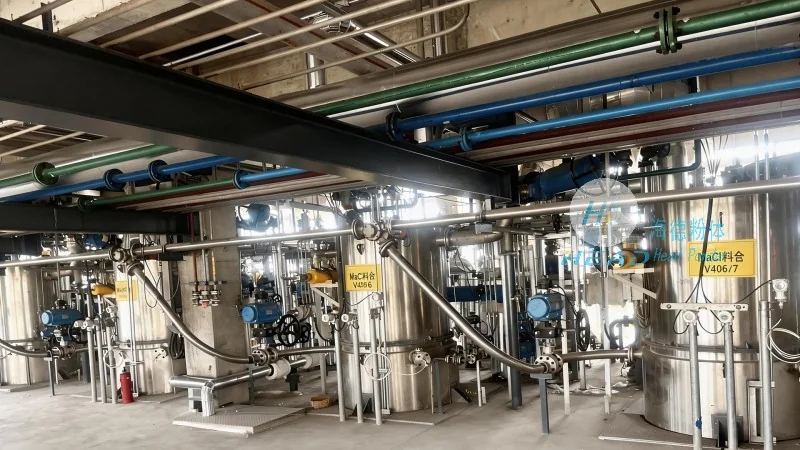
Key Advantages of Pneumatic Conveying for Sodium Bicarbonate
Compared to other powder handling methods, pneumatic conveying offers several advantages when dealing with sodium bicarbonate. Firstly, it provides excellent dust control, as the material is contained within the pipeline, reducing the risk of airborne particles and improving workplace safety. Secondly, the system is highly flexible, allowing for the transportation of materials over long distances and through complex layouts without the need for multiple transfer points. Additionally, pneumatic conveying systems are relatively easy to install and maintain, with minimal moving parts that can wear out over time. These benefits make pneumatic conveying an ideal choice for industries that require consistent and reliable transport of sodium bicarbonate, ensuring that the material remains in its original state and meets the required quality standards.
Customization and Application Flexibility
HeadPowder recognizes that different applications may have varying requirements for sodium bicarbonate handling. Therefore, the company offers customized pneumatic conveying solutions that can be tailored to specific needs. Whether the goal is to transport sodium bicarbonate from a storage silo to a processing plant or to distribute it to multiple points within a facility, HeadPowder’s systems can be designed to meet these demands. The company’s engineers work closely with clients to understand their operational challenges and develop solutions that optimize efficiency and reduce downtime. By leveraging advanced technology and years of experience, HeadPowder ensures that its pneumatic conveying systems are not only effective but also cost-efficient in the long run.
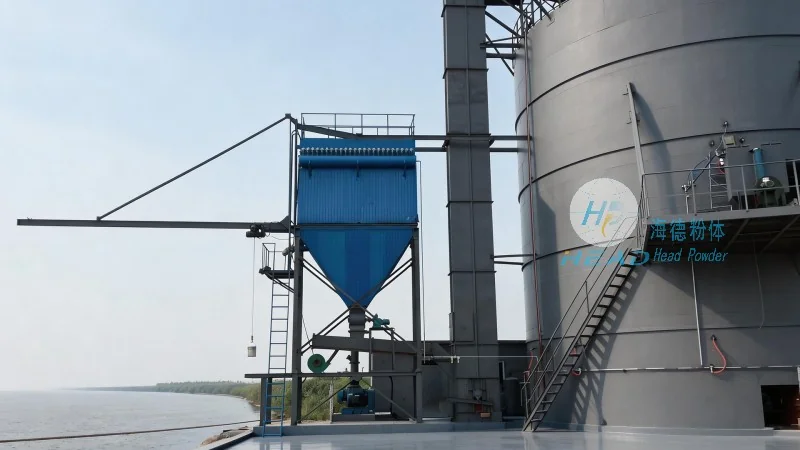
Conclusion: Enhancing Efficiency with Pneumatic Conveying
In conclusion, pneumatic conveying systems represent a sophisticated and efficient method for transporting sodium bicarbonate. By understanding the working principles and advantages of these systems, businesses can enhance their operational capabilities and ensure the safe and reliable handling of this essential material. With its expertise and commitment to quality, Shandong HeadPowder Engineering Co., Ltd. continues to provide top-tier powder handling solutions that meet the evolving needs of the industry. As the demand for efficient sodium bicarbonate transport grows, companies like HeadPowder play a vital role in supporting the success of various sectors that rely on this versatile chemical.