

What Comprises the Pneumatic Conveying of Rare Earth Ore Powders
When discussing the pneumatic conveying of rare earth ore powders, it's essential to understand the core components that form a functional and efficient system. This process involves transporting fine powders, such as those derived from rare earth minerals, using air or gas as the conveying medium. The components of such a system are designed to ensure reliable material handling, minimize dust emissions, and maintain operational efficiency. The following sections outline the key elements that constitute a typical pneumatic conveying system for rare earth ore powders.
Key Components of a Pneumatic Conveying System
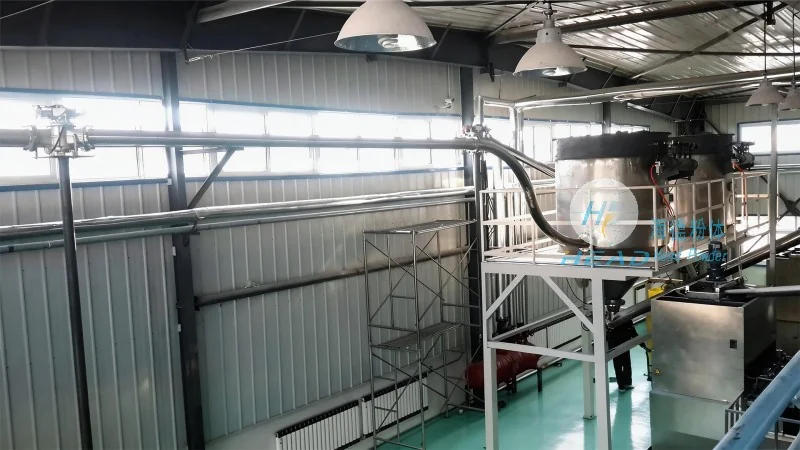
The pneumatic conveying system for rare earth ore powders typically consists of several interconnected components. These components work in synergy to achieve the desired material transport. The primary elements include the material feed system, the conveying line, the air supply system, and the control mechanisms. Each component plays a crucial role in the overall operation and performance of the system.
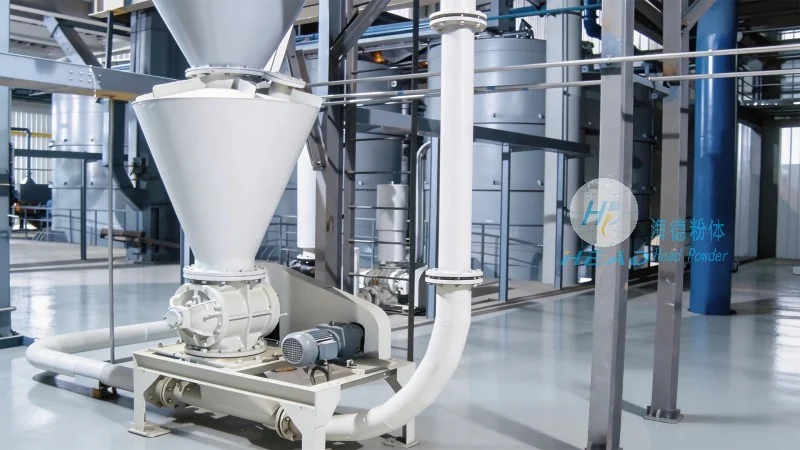
Firstly, the material feed system is responsible for introducing the rare earth ore powder into the conveying line. This may involve hoppers, feeders, or rotary valves that ensure a consistent and controlled flow of the powder. The design of the feed system is critical to prevent blockages and maintain a steady material supply. For rare earth ore powders, which can be abrasive and have specific flow characteristics, specialized feed equipment is often used to handle these materials effectively.

Secondly, the conveying line is the main pathway through which the powder and air mixture travels. This can be either a positive pressure system, where air is forced through the line, or a negative pressure system, where air is drawn through the line. The choice of system depends on factors such as the distance to be covered, the material properties, and the desired flow rate. The conveying line is usually made of materials like stainless steel or plastic to withstand the abrasive nature of the rare earth ore powders and to prevent contamination.
Thirdly, the air supply system provides the necessary air or gas to move the powder through the conveying line. This includes compressors, air dryers, and filters. The air must be clean and dry to avoid moisture-related issues with the rare earth ore powders, which can affect their quality and processing characteristics. The air supply system is designed to maintain a consistent pressure and flow rate, ensuring reliable operation of the conveying system.
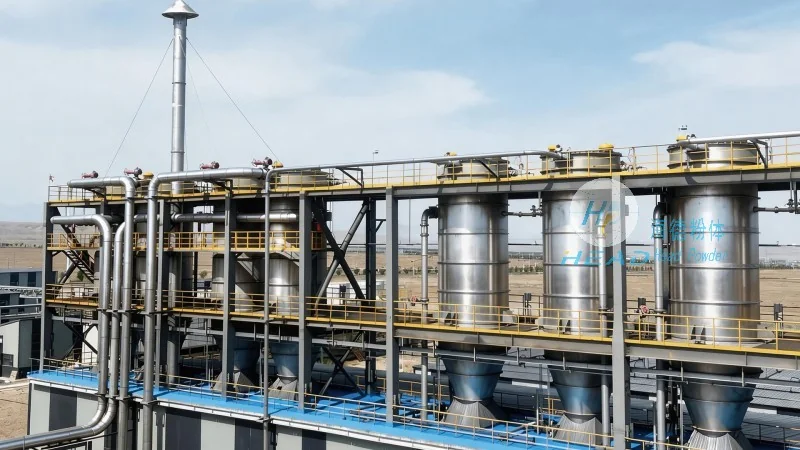
Fourthly, the control mechanisms are essential for monitoring and regulating the operation of the pneumatic conveying system. These may include pressure sensors, flow meters, and control valves. The control system allows operators to adjust the conveying parameters in real-time, ensuring optimal performance and preventing system failures. For rare earth ore powders, which require precise control due to their sensitivity to handling conditions, advanced control systems are often employed.
Special Considerations for Rare Earth Ore Powders
When dealing with rare earth ore powders, additional considerations are necessary to ensure the effectiveness and longevity of the pneumatic conveying system. Rare earth minerals are often fine and have high specific gravity, which can lead to issues such as caking, agglomeration, and increased wear on equipment. To address these challenges, the system components are often designed with special features. For example, the feed hoppers may include agitators or vibrators to prevent material buildup and ensure smooth flow. The conveying lines may be equipped with cleaning mechanisms to remove any deposits that could affect performance.
Moreover, the handling of rare earth ore powders requires adherence to strict quality control measures. The pneumatic conveying system must maintain the purity of the material, preventing contamination from the air or other components. This is achieved through the use of high-quality filters and sealed systems. The control system also plays a role in monitoring the material quality, such as moisture content and particle size distribution, to ensure that the powder meets the required specifications for downstream processing.
Role of Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, specializes in the design and manufacturing of pneumatic conveying systems tailored for various industrial applications, including those involving rare earth ore powders. With a focus on providing reliable and efficient solutions, the company utilizes advanced engineering principles and materials to develop systems that meet the specific needs of clients. The company's expertise lies in understanding the unique properties of rare earth minerals and designing components that can handle these materials effectively, ensuring long-term operational performance and minimal maintenance.
HeadPowder's systems are built with durability and efficiency in mind. The use of high-quality stainless steel and specialized materials in the construction of components, such as hoppers, conveying lines, and air supply units, ensures resistance to corrosion and wear caused by the abrasive nature of rare earth ore powders. The company also emphasizes the importance of proper system integration and commissioning to ensure that the equipment operates as intended. By adhering to strict quality standards and providing comprehensive support, headpowder helps clients achieve optimal performance in their rare earth ore processing operations.