

Components of Pneumatic Conveying for Baking Powder
Welcome to Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer specializing in advanced pneumatic conveying systems for baking powder applications. Our expertise lies in the comprehensive design and implementation of systems that ensure efficient, safe, and reliable material handling for this critical ingredient in the food industry.
Core Components of Pneumatic Conveying Systems
The pneumatic conveying of baking powder involves several key components that work in tandem to achieve optimal performance. These components are meticulously engineered to handle the unique properties of baking powder, such as its fine particle size and sensitivity to moisture. The primary elements include:
1. Material Hopper and Storage
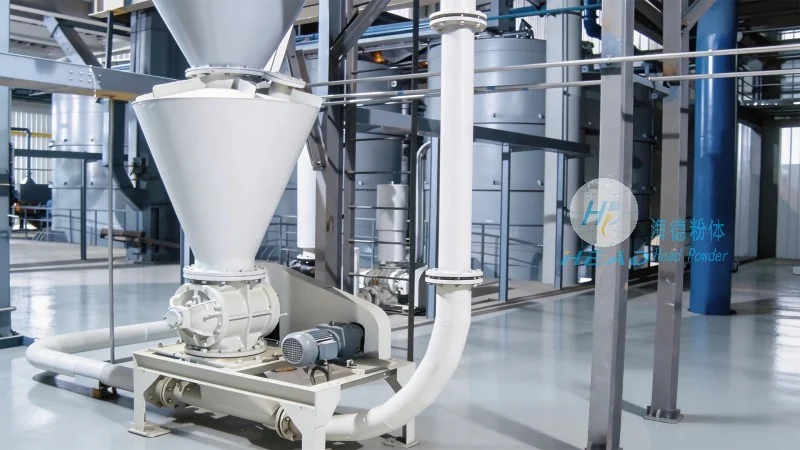
The process begins with a material hopper or storage silo, which serves as the initial container for the baking powder. This component is designed to maintain the product's quality by minimizing exposure to air and moisture. The hopper is typically equipped with a discharge valve or feeder that regulates the flow of material into the conveying system. For larger operations, multiple hoppers may be used to ensure a continuous supply, preventing interruptions in production.
2. Conveying Line and Tubing
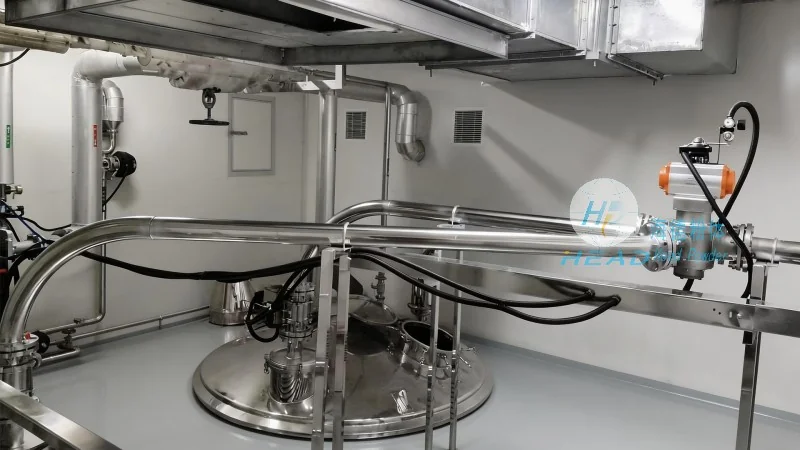
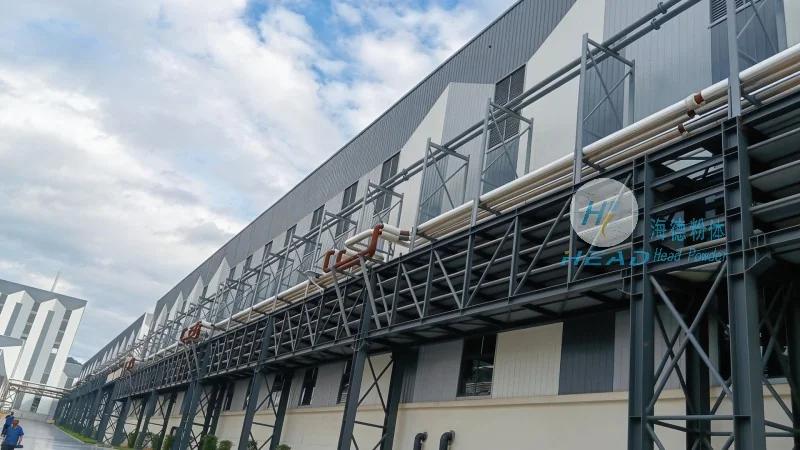
The heart of the pneumatic conveying system is the conveying line, which consists of a network of stainless steel tubing. The choice of tubing material is crucial, as it must be resistant to corrosion and able to withstand the abrasive nature of fine baking powder particles. The line is usually arranged in a loop or straight configuration, depending on the layout of the facility. The diameter and length of the tubing are carefully calculated to maintain the appropriate air velocity, ensuring that the powder is transported efficiently without clogging or degradation.
3. Air Supply and Blower Unit
Air supply is a critical factor in pneumatic conveying, as it provides the necessary force to move the material through the system. The blower unit, often a positive displacement blower or a rotary lobe blower, generates the required pressure and volume of air. The blower is typically located near the material inlet, ensuring that the air is introduced at the correct point to initiate the conveying process. The unit is equipped with controls to regulate air flow and pressure, allowing for adjustments based on the volume of material being handled.
4. Dust Collection and Filtration System
Due to the fine nature of baking powder, dust control is essential to maintain a clean and safe working environment. The system includes a dust collection and filtration unit that captures any airborne particles during the conveying process. This unit typically consists of a cyclone separator or a baghouse filter, which removes the powder from the air stream and returns it to the system or stores it for disposal. Proper filtration is vital to prevent product contamination and to comply with environmental regulations.
5. Control and Monitoring Systems
Modern pneumatic conveying systems for baking powder are equipped with advanced control and monitoring systems. These systems allow operators to track the flow rate, pressure, and temperature of the material and air, ensuring that the process operates within optimal parameters. Sensors and indicators provide real-time feedback, enabling quick adjustments to maintain efficiency and prevent equipment damage. The control panel is usually user-friendly, with intuitive interfaces that simplify operation and reduce the risk of human error.
Integration with Production Processes
The components of the pneumatic conveying system are seamlessly integrated with the overall production process to enhance efficiency and product quality. The system connects directly to the baking powder storage, conveying it to the mixing or packaging stages as needed. This integration minimizes manual handling, reduces the risk of contamination, and ensures a consistent supply of material. The design of the system takes into account the specific requirements of the production line, such as batch sizes, production rates, and product specifications.
Benefits of Pneumatic Conveying for Baking Powder
Implementing a pneumatic conveying system for baking powder offers numerous benefits that contribute to the success of food manufacturing operations. These advantages include improved product quality through reduced exposure to air and moisture, enhanced safety by minimizing manual handling, and increased operational efficiency through automated material flow. The system also reduces labor costs and downtime by eliminating the need for manual loading and unloading of material. Additionally, the compact design of the system allows for easy installation in existing facilities, making it a cost-effective solution for both new and existing production lines.
Customization and Maintenance
Shandong HeadPowder Engineering Co., Ltd. specializes in customizing pneumatic conveying systems to meet the unique needs of each client. Our team of engineers works closely with customers to design systems that align with their production requirements, space constraints, and budget. We offer a range of options, from standard configurations to fully customized solutions, ensuring that each system is tailored to the specific application. Regular maintenance is essential to keep the system operating at peak performance. Our company provides comprehensive maintenance services, including routine inspections, component replacement, and troubleshooting. By adhering to a regular maintenance schedule, customers can extend the lifespan of their equipment and minimize the risk of unexpected breakdowns.
Conclusion
In conclusion, the pneumatic conveying of baking powder is a sophisticated process that relies on a combination of carefully selected components working together to achieve efficient material handling. From the material hopper to the dust collection system, each element plays a critical role in maintaining product quality and operational efficiency. Shandong HeadPowder Engineering Co., Ltd. is committed to providing high-quality, reliable pneumatic conveying systems that meet the demanding requirements of the baking powder industry. Our expertise in system design, manufacturing, and maintenance ensures that our clients receive the best possible solution for their material handling needs.