

Types and Practical Applications of Pneumatic Conveying Systems for Quartz Stone Transport
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of advanced material handling solutions. Among these, pneumatic conveying systems for quartz stone transport stand out as a critical technology for efficient and reliable material movement in various industrial settings. This article explores the different types of pneumatic conveying systems used in quartz stone handling and their practical applications, providing insights into how these systems enhance operational efficiency and product quality.
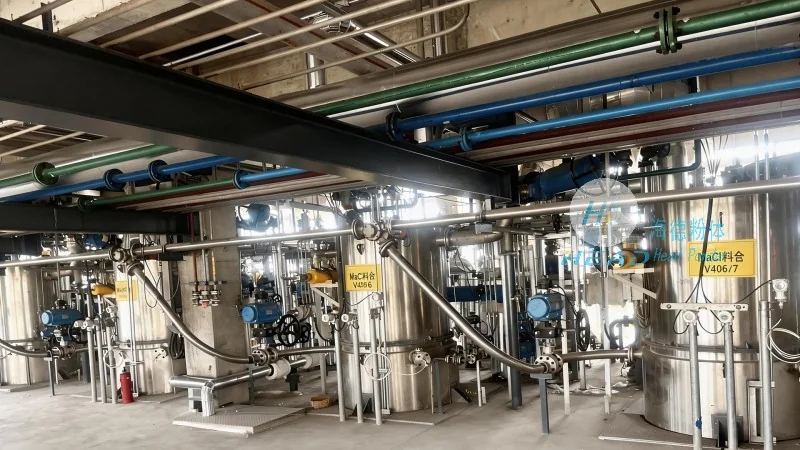
Types of Pneumatic Conveying Systems for Quartz Stone Transport
There are primarily two main categories of pneumatic conveying systems: positive pressure and negative pressure systems. Each type has distinct characteristics and is suitable for different operational requirements in quartz stone transport.
Positive pressure systems, also known as pressure conveying systems, operate by blowing air or a gas mixture into the conveying line, pushing the material forward. These systems are often preferred for long-distance transport and can handle a wide range of particle sizes and moisture content. They are particularly effective when the material needs to be conveyed from a central source to multiple destinations or when the system is integrated with other processing equipment.
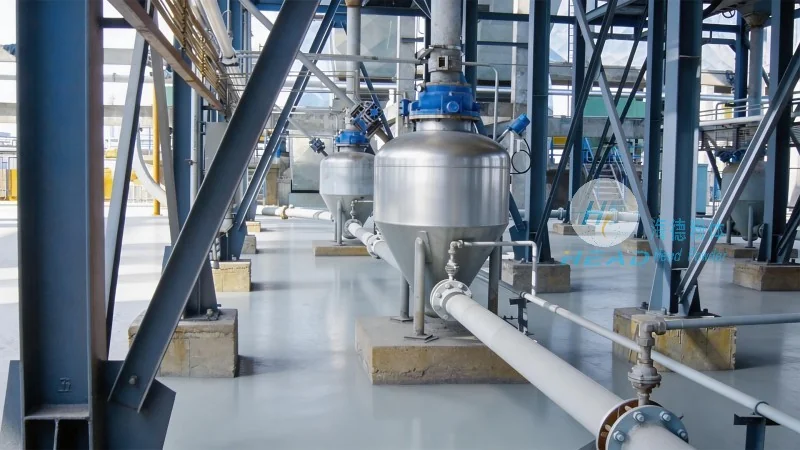
Negative pressure systems, or vacuum conveying systems, work by creating a vacuum in the conveying line, drawing the material into the system. This type of system is commonly used for short to medium-distance transport and is ideal for handling fine powders or granules that are sensitive to pressure changes. Negative pressure systems are also advantageous when the material is to be collected from multiple points and transported to a central location, as they can accommodate multiple inlet points without the need for complex branching.
Practical Applications of Pneumatic Conveying Systems in Quartz Stone Handling
The application of pneumatic conveying systems in quartz stone transport varies based on the specific needs of the industry. For instance, in mining and quarrying operations, these systems are used to transport raw quartz stone from the extraction site to processing facilities, ensuring a continuous and uninterrupted supply of raw materials. The positive pressure systems are often employed here due to their ability to handle large volumes and long distances, which is crucial for large-scale mining operations.
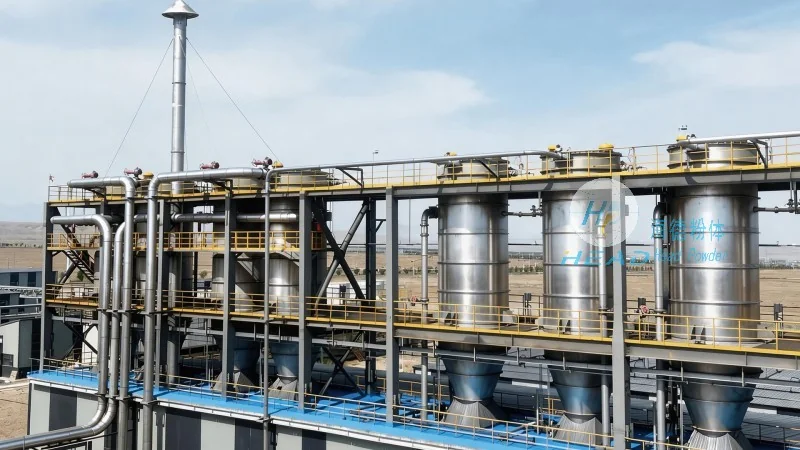
In the manufacturing sector, particularly in the production of quartz-based products such as countertops or decorative stones, pneumatic conveying systems play a vital role in transporting finished or semi-finished products between different stages of production. The negative pressure systems are frequently used in this context to handle fine powders or dust, which are byproducts of the processing and need to be collected and recycled efficiently. This not only improves the overall efficiency of the production line but also enhances environmental compliance by reducing dust emissions.
Additionally, in the construction and building materials industry, pneumatic conveying systems are utilized to transport quartz stone for use in concrete mixtures or as a component in decorative coatings. The systems are designed to handle the specific characteristics of quartz stone, such as its hardness and abrasiveness, ensuring that the conveying process is efficient and the equipment is durable. The use of these systems in construction applications helps in reducing labor costs and improving the quality of the final construction materials by ensuring consistent material quality throughout the transport process.
HeadPowder's Expertise in Pneumatic Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd. leverages its extensive experience and technical expertise to provide customized pneumatic conveying solutions tailored to the unique requirements of quartz stone transport. The company's engineers work closely with clients to assess their operational needs, material characteristics, and site conditions to design systems that maximize efficiency and minimize downtime. Whether it's a positive or negative pressure system, the company's solutions are engineered to meet the highest standards of performance and reliability.
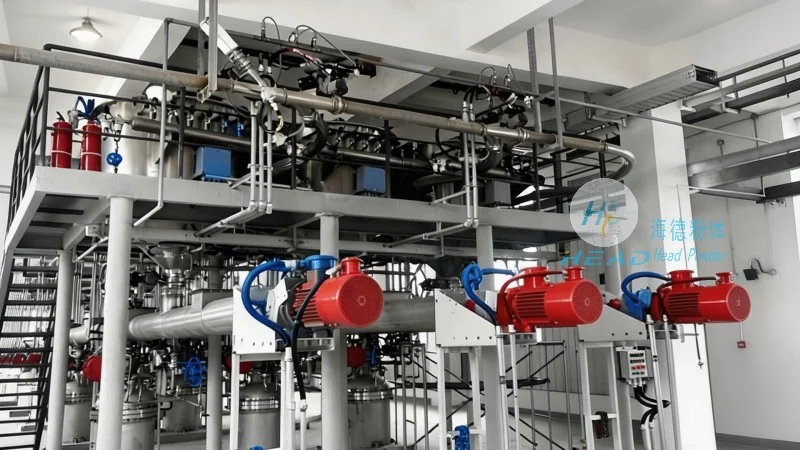
HeadPowder's commitment to quality is evident in its use of advanced materials and components in the construction of pneumatic conveying systems. The systems are designed to withstand the abrasive nature of quartz stone, ensuring long service life and low maintenance costs. The company also provides comprehensive support services, including installation, commissioning, and maintenance, to ensure that the systems operate at optimal performance levels throughout their lifecycle.
Conclusion
Pneumatic conveying systems are a vital technology in the efficient handling of quartz stone, offering numerous benefits over traditional methods such as belt conveyors or bucket elevators. The choice between positive and negative pressure systems depends on the specific operational requirements, including distance, material characteristics, and the need for multiple inlet or outlet points. By understanding the different types and their applications, industries can select the most appropriate pneumatic conveying system to enhance their operational efficiency and product quality. HeadPowder, with its expertise and customized solutions, continues to be a trusted partner in implementing effective pneumatic conveying systems for quartz stone transport, contributing to the growth and success of its clients in the industry.